Deep Hole Drilling Services
Our deep hole drilling services hold fit-critical bores to ±0.005 mm past an L/D of 10:1. Gundrilling or BTA tooling is matched to each bore, from one prototype to production.
-
±0.005 mm
Fit-Critical Bores
-
~1000 mm
Workpiece Length
-
3 Days
First Articles

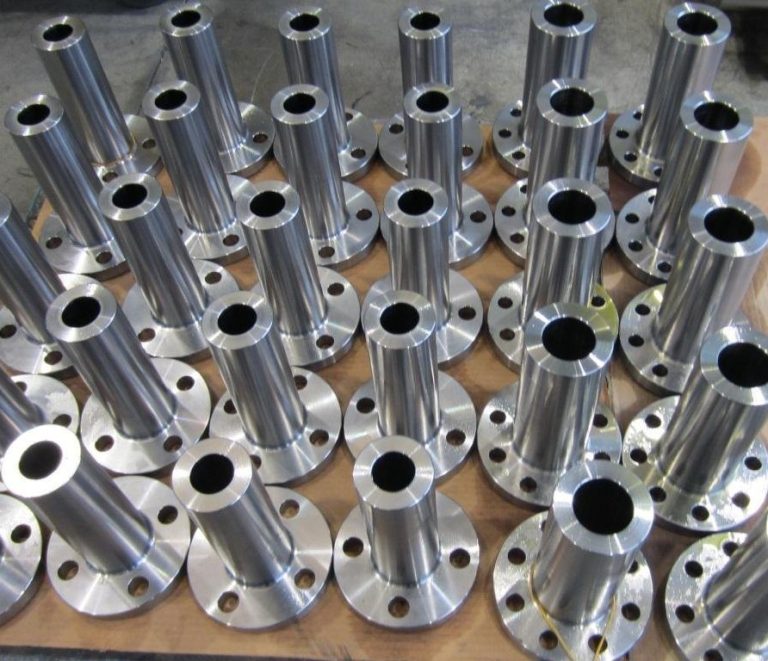
Long Bore Machining for Custom CNC Parts
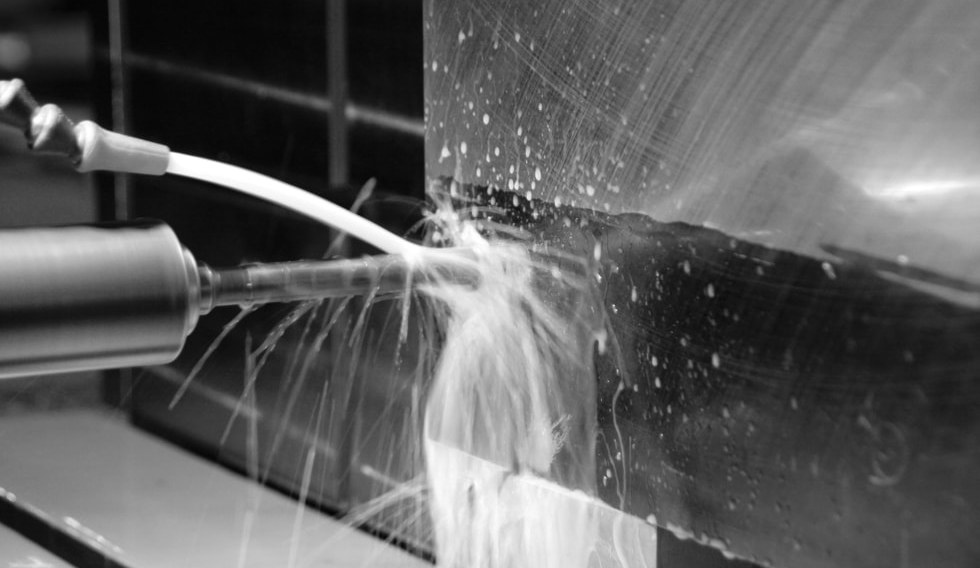
Once a hole’s depth passes roughly 10 times its diameter (L/D >10:1), standard drilling loses straightness, generates heat and drifts off-center. DEK matches single-flute gundrill tooling or external-coolant BTA boring bars to the bore’s ratio and material.
Deep bores run inside full CNC machining programs, from a single prototype bore to a production run. Because gundrilling and BTA differ in coolant path, the right choice depends on bore diameter and length; talk with our engineers to have your bore reviewed.
Why Source Deep Holes Through DEK
Deep hole drilling rarely stands alone. Here is why engineers keep the bore and the rest of the part under one roof.
-

One Quality System
Milling, turning, EDM and grinding around the bore run under the same documented QMS, certified to ISO 9001, ISO 13485 and AS9100D.
-

No Minimum Order
There is no MOQ: a single prototype bore gets the same process discipline and inspection as a production batch.
-

Engineer-Led Review
Our engineering team, led by 14+ years of hands-on production experience, reviews the bore geometry before cutting starts.
-

3-Day First Articles
First-article samples are typically ready in 3 days once the bore geometry, material and tolerance are confirmed.

Bores Verified on Real Parts
Every bore is measured on in-house CMM equipment with traceable, documented results, so straightness and concentricity are confirmed on the actual part. We ship to clients across Europe and North America.
Deep Hole Drilling Capabilities
We size the drilling method to your geometry instead of quoting one blanket maximum depth; exact numbers are confirmed at quote review.
Deep Hole Drilling vs. Other Hole Processes
Choose deep hole drilling once depth passes about 10 times diameter; below that, standard CNC drilling is enough.
| Criteria | This ProcessDeep Hole Drilling | CNC Drilling | CNC Turning |
|---|---|---|---|
| Best for | Long, straight bores | Shallow holes | Features around the bore |
| Depth ratio | L/D over 10:1 | Up to about 10:1 | Not a drilling method |
| Straightness at depth | Held, CMM verified | Drifts off-center | Supports bore coaxiality |
| Heat and chips | Through-tool coolant | Heat builds at depth | Not applicable |
| Tooling | Gundrill or BTA bar | Standard drills | Turning centers |
Deep Bores Across Industries
Medical, energy, industrial equipment and tooling programs rely on deep, straight bores machined and inspected under one quality system.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
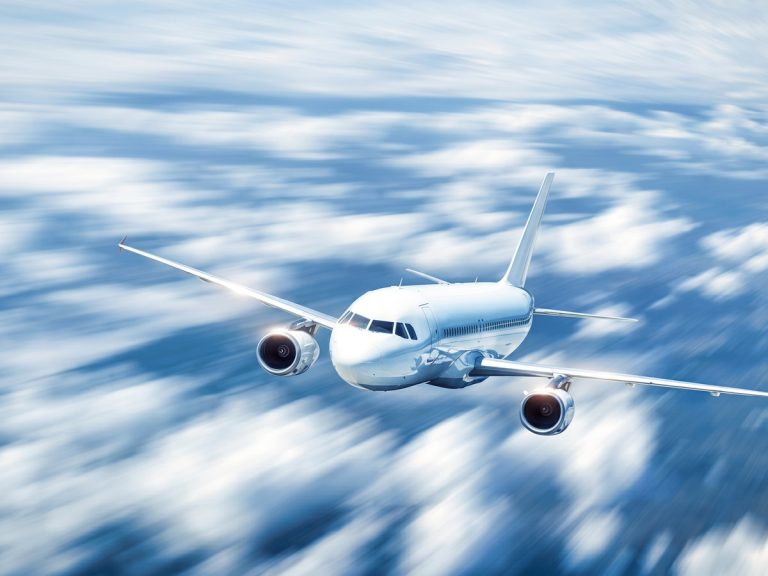 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Typical Deep-Hole Parts and Challenges
Deep, straight bores show up wherever a fluid, shaft or tool must pass cleanly through a long section of metal.
-

Hydraulic Cylinders & Rams
Bodies up to 1000 mm long keep the through-bore at ±0.005 mm coaxiality over the full length, so the piston never binds.
-

Shafts & Spindles
Long internal bores in custom shafts and spindles, with shaft-to-bore coaxiality held to ±0.005 mm.
-

Manifolds & Valve Bodies
Long fluid passages drilled in custom manifolds and valve bodies, then milled around the bores.
-

Mold Cooling Channels
Deep cooling channels in tooling and mold components, drilled straight along the full length.
-

Medical Instrument Bores
Small, deep bores for medical CNC machining, under ISO 13485 and with sub-10 mm features to ±0.003 mm.
-
Energy Equipment Housings
Long bores in energy and industrial equipment housings, often paired with large part CNC machining.
Common Challenges We Handle
-
Bore Drift
Beyond 10:1, standard drills drift off-center; gundrill or BTA tooling with pilot bushing accuracy keeps the bore straight.
-
Heat and Chip Evacuation
Through-tool coolant clears chips and controls heat along the full bore, with flow and pressure set per material and diameter.
-
Full-Length Coaxiality
Fit-critical bores held to ±0.005 mm coaxiality and concentricity, verified on CMM rather than assumed from a catalog spec.
-
Tough Alloys
Titanium, stainless and Inconel resist sustained cutting pressure; max L/D is confirmed per material at quote review.
Certified Quality for Every Bore
Deep-hole parts run through IQC, IPQC, FAI, OQC, SPC and CAPA, certified through TUV.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Metals We Deep-Hole Drill
Long, accurate bores depend on how the material behaves under sustained cutting pressure and heat. These are the alloys we drill.
Drilling another alloy? Ask our engineers about your material.
All MetalsHow to Order Deep-Hole Parts
Deep Hole Drilling FAQ
Short answers on depth limits, tolerances and drilling methods for long bores.
Request a Quote for Deep Hole Drilling Services
Send your bore geometry, material and tolerance; our engineers review it and send feedback before you commit to a vendor.
- Engineer-reviewed quote within 6 hours
- No MOQ, from a single prototype bore
- First articles typically in 3 days
- Fit-critical bores held to ±0.005 mm
- Every bore verified on in-house CMM

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.