

Media Blasting Services for CNC Machined Parts
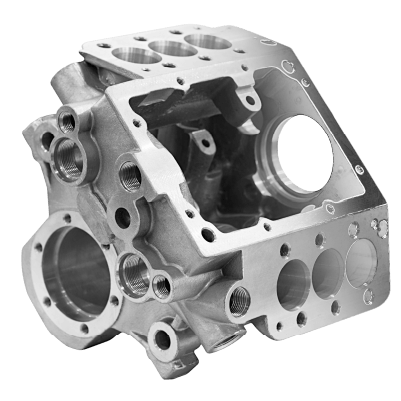
DEK's media blasting services are applied to parts we machine in-house, in the same order: bead blasting, aluminum oxide, ceramic and shot peening. Blasting adds a day at most, no MOQ.
- Ra 0.8–3 µm Typical Matte
- AMS 2430 Peening Standard
- ±0.005 mm Feature Tolerance
Media Blasting Services at DEK
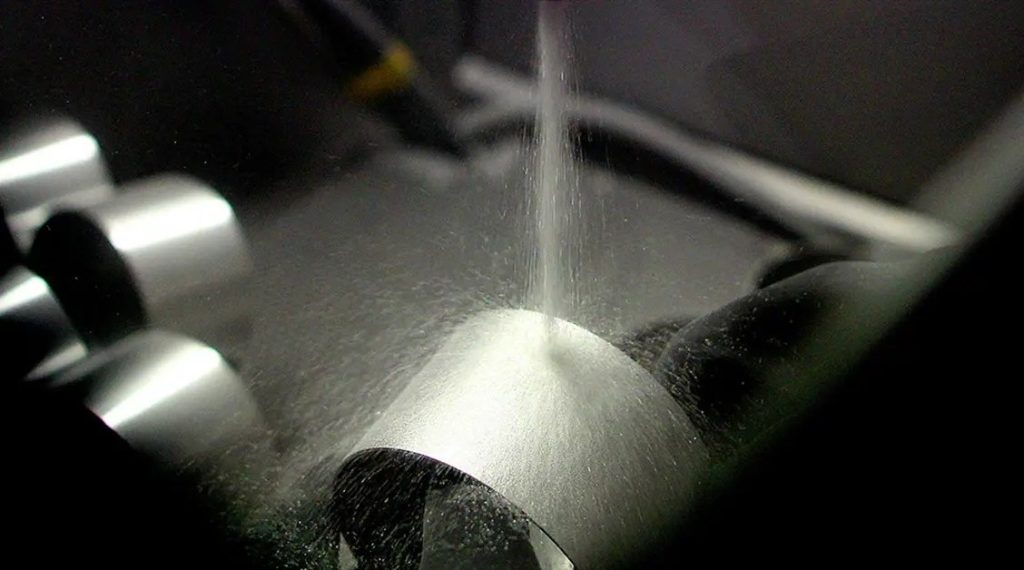
Compressed air propels media at the machined surface, leaving a uniform, non-directional texture. Blasting is planned with the machining in the same order; no blasting-only orders.
What Media Blasting Delivers & Where to Be Mindful
Blasting changes texture and cleanliness, not geometry. Know its strengths and limits before you specify it on a machined part.
-

Key Benefits
- Tool marks disappear: cutter paths and step-over lines are replaced by a uniform, non-directional texture
- Hides fingerprints: the matte surface stays clean-looking on handled housings and hardware
- Light burrs removed: blasting knocks off light burrs left by machining
- Clean surface: scale, heat tint and EDM recast are cleaned off before the next finish
- Paint and powder key: aluminum oxide leaves an etched texture suited to paint adhesion
- Longer fatigue life: shot peening adds compressive stress 0.1–0.5 mm deep
-

Limitations & Alternatives
- No precision improvement: blasting does not improve flatness, roundness or Ra on a precision face
- Smooth or bright surface: choose polishing or electropolishing on stainless; blasting goes the other way
- Internal passages: blasting cannot reach cross-holes; see deburring for edge work inside
- Small parts in volume: vibratory tumbling gives a similar matte at lower cost per piece
- Material removal on fits: aluminum oxide removes 5–10 µm on aluminum, so tight bores need masking
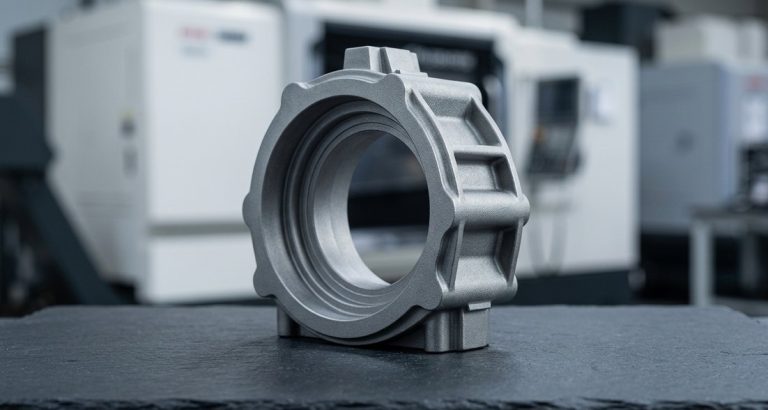
Matte Finish and Surface Results
Each media gives a measurable result on a machined part: texture, roughness, cleanliness or fatigue resistance, matched to the next finish.
-

Uniform Satin Matte
Glass bead #80–#170 gives Ra 0.8–1.6 µm with negligible dimensional change (< 2 µm) on cosmetic aluminum and stainless.
-

Brighter Satin
Ceramic bead 60–150 µm gives Ra 0.4–1.0 µm, finer and more consistent lot to lot on stainless, titanium and aluminum.
-

Etched Paint Key
Aluminum oxide 60–220 grit leaves Ra 1.5–4 µm for paint and powder-coat adhesion and scale removal on steel and titanium.
-

Fatigue Resistance
Shot peening closes surface micro-cracks and delays fatigue crack initiation, commonly extending fatigue life several-fold.
-

Gentle Cleaning
Plastic media Type II / Type V, 20–40 mesh leaves Ra ≤ 0.8 µm with no dimensional change on plastics and thin aluminum.
-

Descaled Steel
Steel shot S110–S330 gives Ra 2–6 µm with small growth; it is never used on aluminum or stainless (iron contamination).
Blasting Media Compared
| Media | Grit / size | Resulting Ra | Effect on dimensions | Purpose and typical materials |
|---|---|---|---|---|
| Glass bead | #80–#170 | 0.8–1.6 µm | Negligible (< 2 µm) | Satin matte; cosmetic aluminum and stainless; pre-anodize; light peening |
| Ceramic bead | 60–150 µm | 0.4–1.0 µm | Negligible | Finer, brighter satin; consistent lot to lot; stainless, titanium, aluminum |
| Aluminum oxide | 60–220 grit | 1.5–4 µm | 5–10 µm removed on aluminum; edges rounded ~0.05 mm | Aggressive etch; paint/powder key; descaling; steel, titanium, cast iron |
| Steel shot | S110–S330 | 2–6 µm | Small growth, surface dimpled | Shot peening and descaling of steel; never on aluminum or stainless |
| Plastic media | Type II / Type V, 20–40 mesh | ≤ 0.8 µm | None | Gentle cleaning, paint stripping, deburring plastics and thin aluminum |
Suitable Materials for Media Blasting
Glass and ceramic bead suit aluminum, stainless steel and titanium; aluminum oxide and steel shot suit steel and cast iron.
Stainless and aluminum are never blasted or peened with steel media, to avoid iron contamination. Silica sand is not used: a “sandblasting CNC parts” note is treated as aluminum oxide or glass bead, confirmed at quote review.
-
6061 AluminumA #120 glass bead blast hides cutter paths before clear or black anodize; deoxidized before the bath.Recommended
-
6063 AluminumTakes the same even, low-gloss bead blast matte before anodizing as 6061 for cosmetic housings.Recommended
-
Stainless SteelGlass or ceramic bead gives a satin matte; peened with stainless, ceramic or glass media only.No steel media
-
TitaniumCeramic bead gives a bright, consistent satin; aluminum oxide etches it as a key under paint.Good
-
Alloy SteelAluminum oxide removes scale; cast steel shot S110–S330 is used for peening and descaling.Peening
-
Cast IronAluminum oxide gives an aggressive etch and scale removal ahead of paint or powder coat.Good
Typical Applications
Media blasting serves cosmetic aluminum hardware and fatigue-critical shafts and gears, from consumer electronics to aerospace landing gear.
-
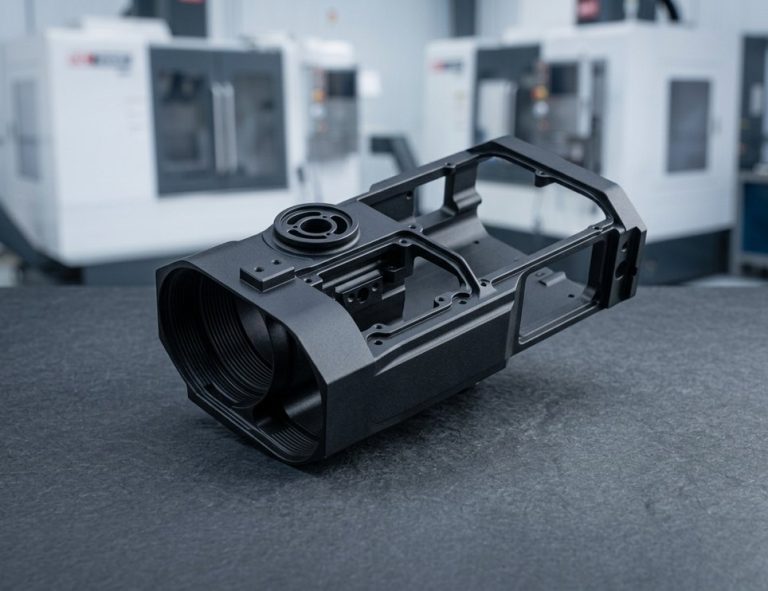 Electronics HousingsMachined 6061 or 6063 housings bead blasted #120 then anodized clear or black for an even, low-gloss matte.Request a Quote
-
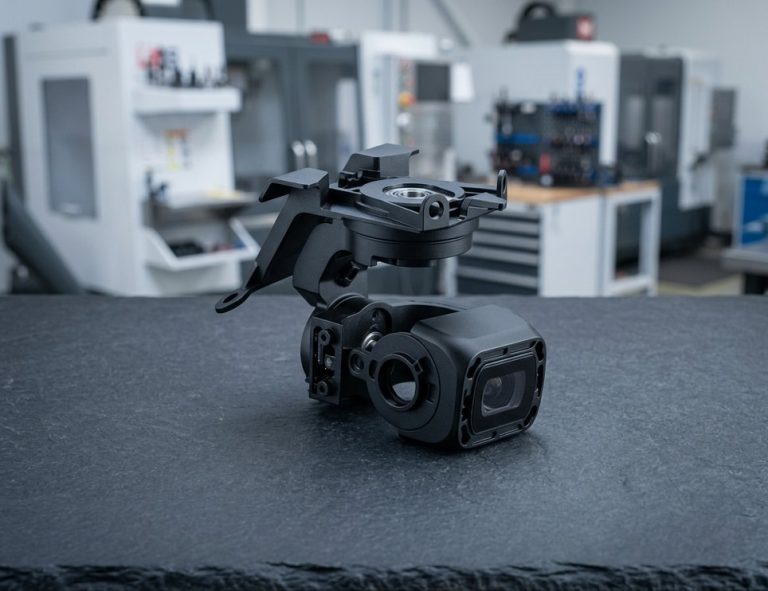 Camera HardwareBead blast before anodize hides every cutter path on visible camera hardware parts.Request a Quote
-
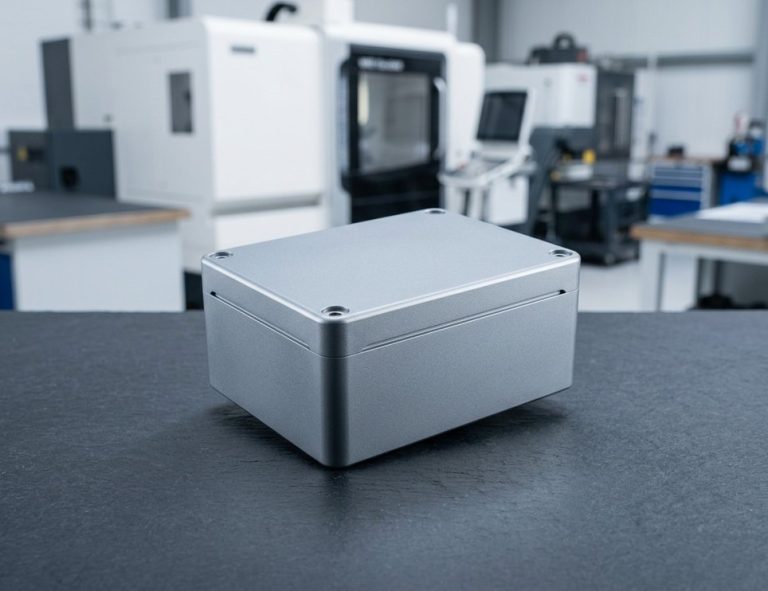 Instrument HousingsUniform matte that hides tool marks and fingerprints on machined instrument housings.Request a Quote
-
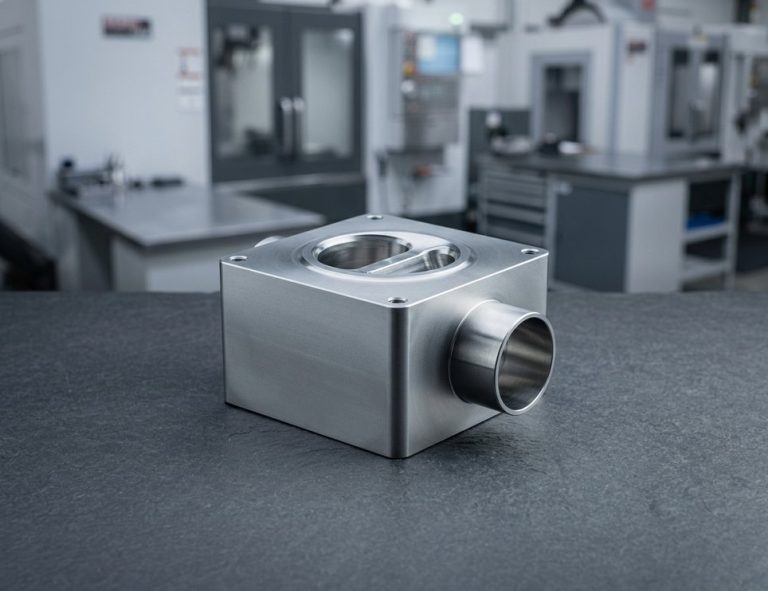 Medical PartsCeramic bead gives a bright satin on stainless, titanium and aluminum medical parts, consistent lot to lot.Request a Quote
-
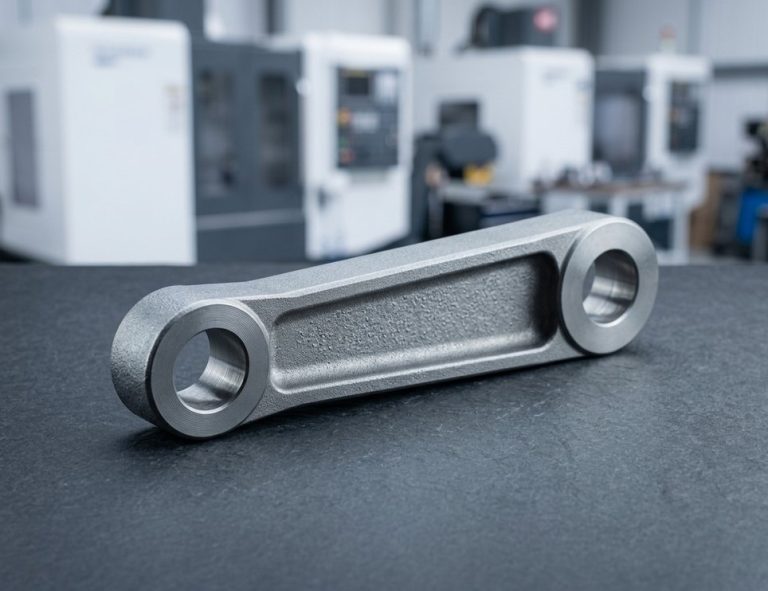 Aerospace ComponentsShot peening is a standard requirement on aircraft landing gear and turbine components.Request a Quote
-
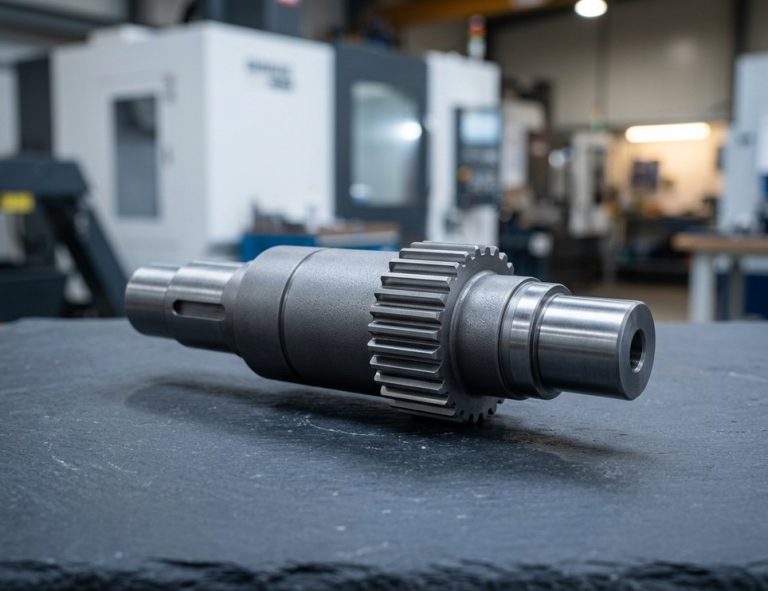 Peened Shafts and GearsSprings, gears and shafts that fail in bending or torsion are peened after final grinding.Request a Quote
Design & Tolerance Notes
Blasting reaches every exposed surface and can remove material, so the drawing must name the media, the surfaces, the masking and the follow-on finish.
-
Mask Critical Fits
Mask bores and shafts with H7/g6 or tighter fits, threads, sealing faces, O-ring grooves, lapped and datum faces, plus laser-marked zones.
-
Expect Edge Rounding
Unmasked aluminum oxide-blasted parts get a 0.05 mm edge radius; polished features lose some gloss.
-
Write the Drawing Note
Example: "Glass bead blast #120 all external surfaces; mask bore Ø12 H7, threads and face A". Add a boundary sample where cosmetic uniformity matters.
-
Name the Follow-On Finish
State "then anodize Type II clear" or "then passivate"; the same blast also works before black oxide on steel for a flat non-reflective black.
-
Sequence Peened Parts
Machine, heat treat, grind, peen, then plate or coat; a light polish may remove under 10% of the compressive depth.
-
Specify Shot Peening Services
Name the standard, media, Almen intensity, coverage and the peened surfaces on the drawing for shot peening services.
Blasting & Peening Specifications
- Glass bead grit #80–#170 (#120 general satin)
- Glass bead Ra 0.8–1.6 µm
- Ceramic bead Ra 0.4–1.0 µm
- Aluminum oxide removal 5–10 µm on aluminum
- Bead removal < 2 µm
- Peening depth 0.1–0.5 mm compressive
- Almen intensity 0.008–0.012 A / 0.006–0.010 N
- Coverage 100% min, 200% critical
- Peening standard AMS 2430 or SAE J2441
- Peened Ra 2–6 µm
- Feature tolerance ±0.005 mm
- Added lead time A day at most
- Certifications ISO 9001:2015, ISO 13485, AS9100D
Bead Blasting and the Shot Peening Process
Two processes with different goals: bead blasting for appearance before anodizing, peening for fatigue life.
Frequently Asked Questions
Answers on media choice, dimensions, anodizing and shot peening on machined parts.

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.