









Precision Wire EDM Services
DEK wire EDM services cut hardened, conductive metals to ±0.005 mm with no distortion and no MOQ. Prototypes ship in as fast as 3 days, from one insert to production runs.
-
±0.005mm
Profile Tolerance
-
1000 mm
Max Part Envelope
-
3 Days
Fastest Prototype

Wire Cut EDM for Hardened Tooling and Parts
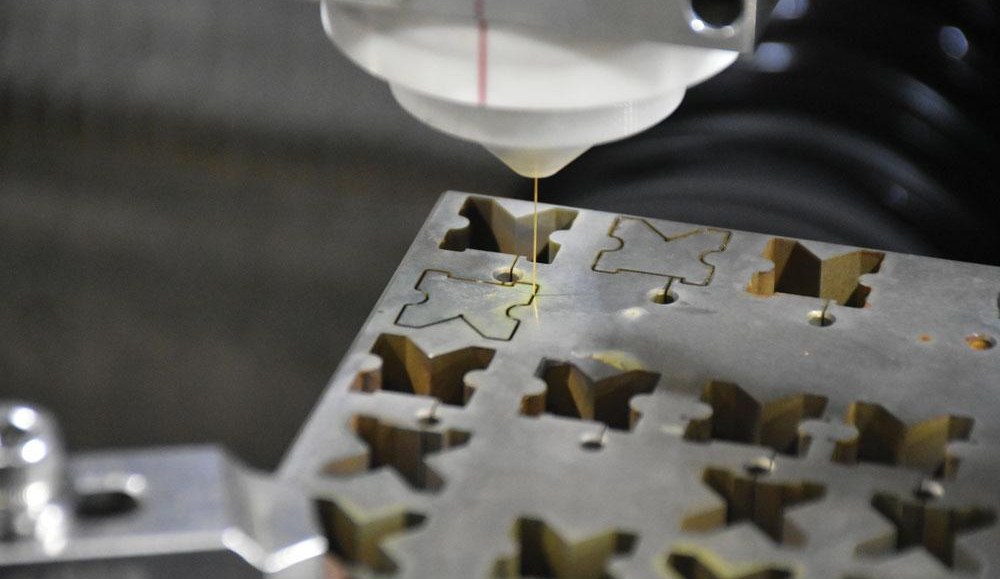
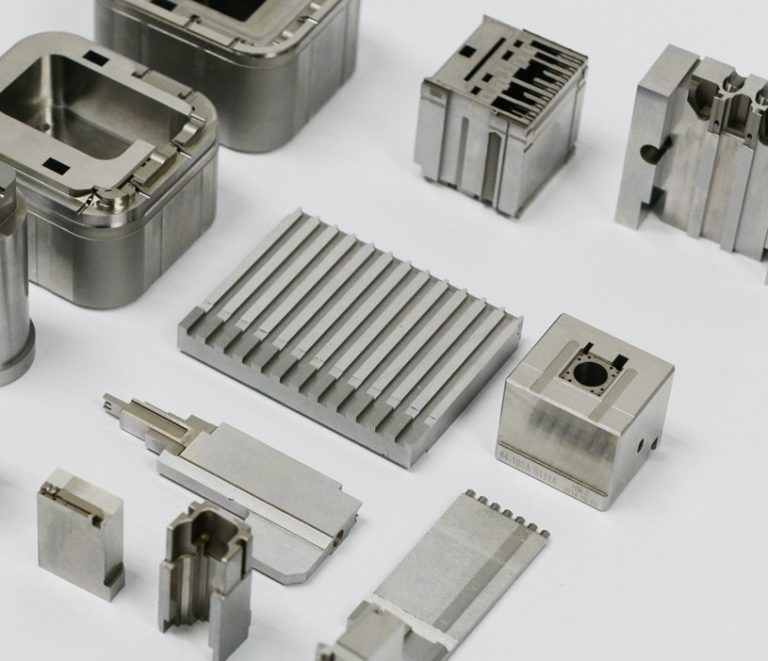
Because the wire never touches the part, wire EDM cuts hardened tool steel as fast as soft metal. Dies and punches go through heat treatment first, then straight to final profiling, with no re-softening and no dimensional drift.
Over 20+ years, our CNC machining China operation has machined 1.2M+ parts a year for 2,300+ OEM clients. One replacement punch gets the same engineering review as a 500-piece run. See how the process works in All You Need to Know about Wire Cut EDM.
Why Toolmakers Choose DEK for Wire EDM
Mold builders, die shops and OEMs without in-house EDM route hardened, tight-tolerance work to our wire EDM floor.
-

Cut After Hardening
Hardened tool steel and heat-treated alloys cut at the same rate as soft metal, so heat treatment happens before final profiling, not after.
-

No-Contact Cutting
The wire never touches the workpiece: no cutting force, no tool deflection and no distortion in thin or delicate sections.
-

No MOQ, Any Run Size
Single prototypes through production runs. Prototypes ship in as fast as 3 days, whether it is one hardened insert or a production batch.
-

Tight, Repeatable Profiles
±0.005 mm on production profiles, tightening to ±0.003 mm on micro and sub-10 mm features, with dimensions holding through repeat runs.

Engineering Review on Every Job
Our engineers check manufacturability and confirm wire EDM is the right process for your geometry, versus milling or sinker EDM, before quoting. Parts needing a mirror finish or tighter flatness are routed to grinding.


Wire EDM Capabilities & Specs
Part size, tolerances, materials and applications for wire-cut profiles in hardened and conductive metals.
Wire EDM vs. Sinker EDM and CNC Milling
Choose wire EDM for cut-through profiles in hardened metal. Both wire and sinker sit under our EDM machining service, so one request routes to the right method.
| Criteria | This ProcessWire EDM | Sinker EDM | CNC Milling |
|---|---|---|---|
| Best for | Cut-through profiles | Cavities and 3D forms | Lighter structural parts |
| Tool | Moving wire electrode | Machined, shaped electrode | End mill cutter |
| Hardened metal | Same rate as soft metal | Spark erosion | Speed depends on hardness |
| Cutting force | None, no contact | Spark erosion | Tool deflection risk |
| Choose when | Sharp corners, thin walls | Pocket or blind form | Aluminum, mild steel parts |
Wire-Cut Parts for Key Industries
We supply wire-cut parts to aerospace (non-flight-critical), medical devices, semiconductor equipment and automotive tooling programs.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Wire EDM Features & Challenges We Solve
Spark erosion cuts geometries that would need small end mills and multiple setups, or be impossible, on hardened material.
-

Sharp Inside Corners
Profiles that would chip a mill cutter or need multiple setups come off in one pass, burr-free.
-

Thin Walls & Fine Slots
No cutting force means no distortion in thin or delicate sections, even on hardened material.
-

Punch & Die Relief Angles
Taper cutting produces relief angles directly in the same setup, with no secondary angled fixture.
-

Micro Features Under 10 mm
Held to ±0.003 mm on sub-10 mm features; see our micro machining services.
-

Profiles up to 1000 mm
Part envelope up to 1000 mm in the largest dimension, from thin sheet stock to thick tool steel blocks.
-
Wire-Cut Plus Turned Features
A shaft with a splined end can move between wire EDM and Swiss CNC turning on one job.
Common Challenges We Handle
-
Hardened Tool Steel
Dies go through heat treatment first, then straight to the wire, avoiding the risk of milling soft and hoping tolerance holds afterward.
-
Tungsten Carbide
Wear parts and electrodes are cut from tungsten steel and carbide, materials that resist conventional cutting.
-
Post-Heat-Treat Drift
No re-softening and no second heat treatment cycle, so there is no dimensional drift between hardening and final profiling.
-
Mirror Finish or Flatness
When skim passes are not enough for a finish or flatness spec, parts are routed through precision grinding after cutting.
Certified Quality for Wire-Cut Parts
Every order runs through IQC, IPQC, FAI, OQC, SPC and CAPA, with CMM inspection.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Conductive Metals and Wire EDM Finishes
Wire EDM cuts electrically conductive metals only. Pair the right alloy with heat treatment, skim passes or grinding.
Surface Finishes
Need another conductive alloy cut? Browse all our materials
View All MetalsHow to Get a Wire EDM Quote
Wire EDM Services FAQ
Straight answers on how wire EDM works, what drives cost and how it differs from EDM.
Get a Wire EDM Quote
Send your drawing for an engineer-reviewed quote on hardened or conductive metal parts, from one insert to a production batch.
- No MOQ on any order size
- Prototypes in as fast as 3 days
- ±0.005 mm on production profiles
- Parts up to 1000 mm
- CMM inspection and full traceability






Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








