Precision Grinding Services
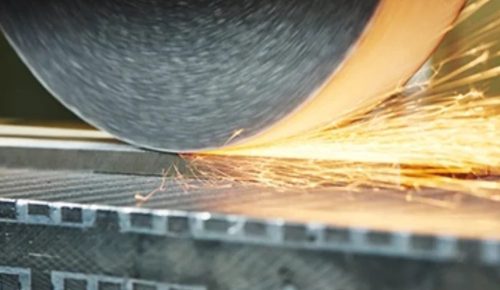
Precision grinding services from DEK hold ±0.002 mm and Ra 0.2–0.4 µm on hardened shafts, plates and bores. Grinding runs in-house after machining and heat treatment, in one order.
-
±0.002 mm
Ground Tolerance
-
Ra 0.05 µm
Lapped Finish
-
6 hours
Engineer Review

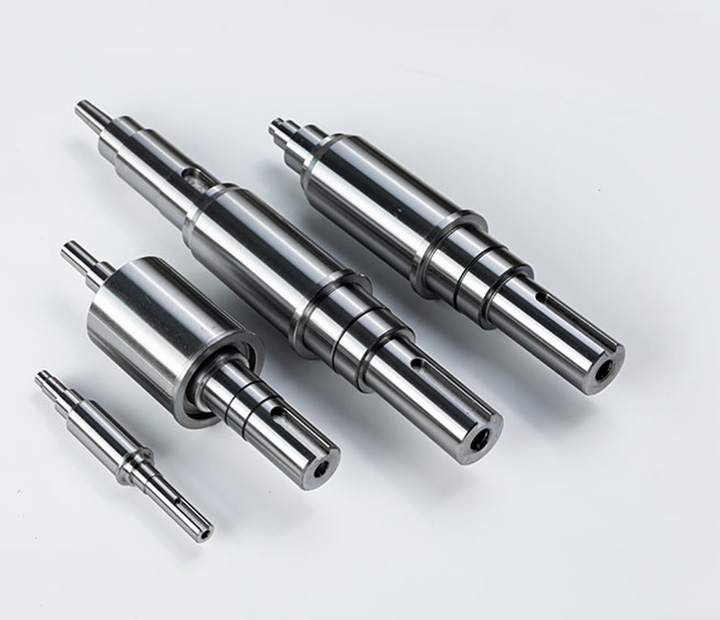
CNC Grinding Services for Hardened Parts
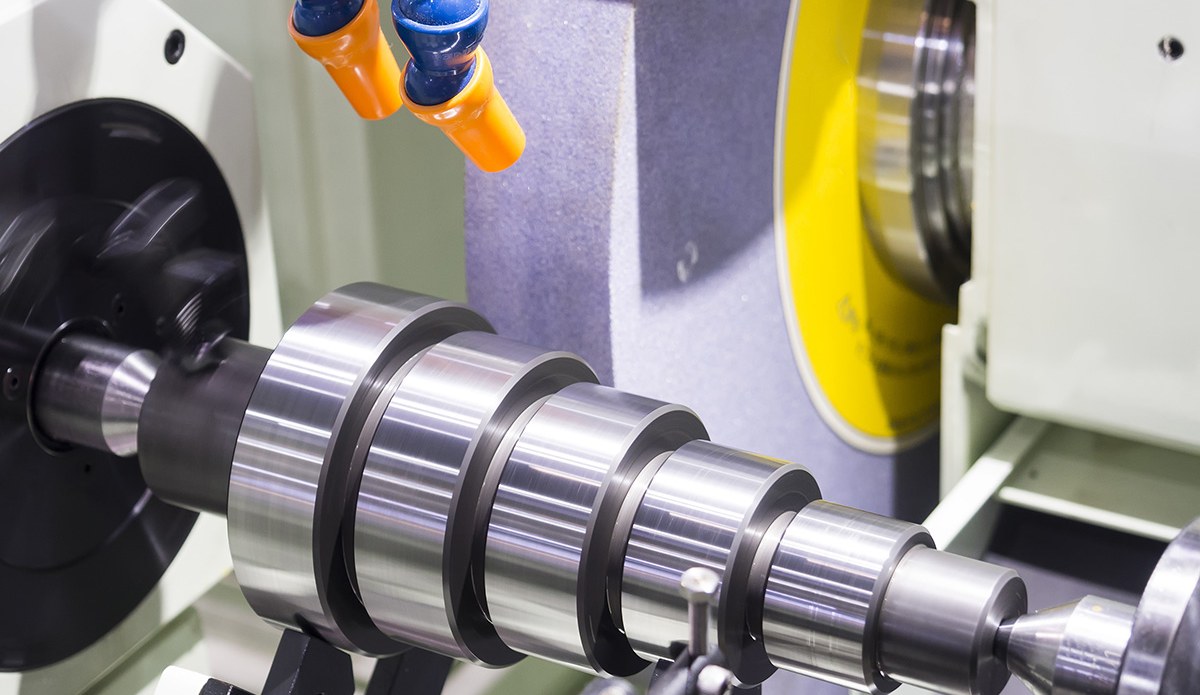
Grinding finishes the features that CNC milling and CNC turning cannot: hardened steel shafts and plates, carbide inserts, bores round within 0.002 mm and seal faces at Ra 0.2 µm. Parts above about 45 HRC are machined with stock allowance, hardened, then ground to size.
Surface, cylindrical, centerless, ID/OD and jig grinding, plus honing and lapping, run in-house on parts we machine. No MOQ, quotes reviewed by an engineer within 6 hours, and grinding scheduled in the same order as your CNC machining and heat treatment.
Why DEK for Precision Grinding Services
Grinding is not an add-on at DEK: it has been part of the shop since day one and runs on the same quality record as machining.
-

In-House Since 2002
DEK began in 2002 grinding mold core pins, ejector pins and guide bushes; grinding stays in-house beside milling, turning, Swiss and EDM.
-

Controlled Inspection
Ground parts are inspected in a temperature-controlled room on CMM, roundness and surface roughness testers, with dimensional reports on request.
-

One Order, One Record
Machining, heat treatment and final grind run under one quality record and one quote, from raw material to finished ground dimensions.
-

No MOQ, 2,300+ Clients
No minimum order quantity and 2,300+ customers worldwide, with ISO 9001:2015, ISO 13485 and AS9100D certification issued by TÜV.

Engineer-Reviewed Sequence
An engineer reviews every drawing, chooses grinding stock for the material and the expected heat-treat distortion, and confirms allowance and sequence before quoting, within 6 hours for most parts.
Precision Grinding Capabilities
Seven grinding and abrasive finishing processes, each matched to a geometry: flat faces, outside diameters, bores and hole patterns.
Grinding vs. Milling, Turning and Jig Boring
Grind when a feature is hardened above about 45 HRC, needs ±0.002 mm or Ra below 0.4 µm. Read what is cylindrical grinding for the basics.
| Criteria | This ProcessPrecision Grinding | CNC Milling | CNC Turning | Jig Boring |
|---|---|---|---|---|
| Typical tolerance | ±0.002 mm | ±0.005 mm | ±0.005 mm | ±0.003 mm position |
| Surface finish | Ra 0.2–0.4 µm | Ra 0.8–1.6 µm | Ra 0.8–1.6 µm | See jig boring page |
| Material state | Hardened, above 45 HRC | Soft material | Soft material | Soft material |
| Place in sequence | Final size after hardening | Rough, semi-finish | Rough, semi-finish | Soft bore patterns |
| Relative cost | Higher | Lower | Lower | Lower than jig grinding |
Ground Parts for Every Industry
From mold and die plates to hydraulic cylinders, medical components and motor shafts, ground parts ship with dimensional reports on request.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
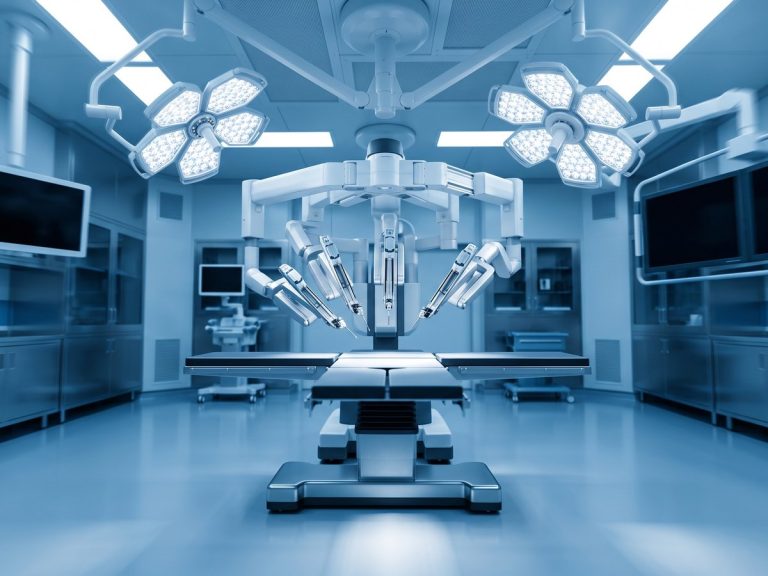 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
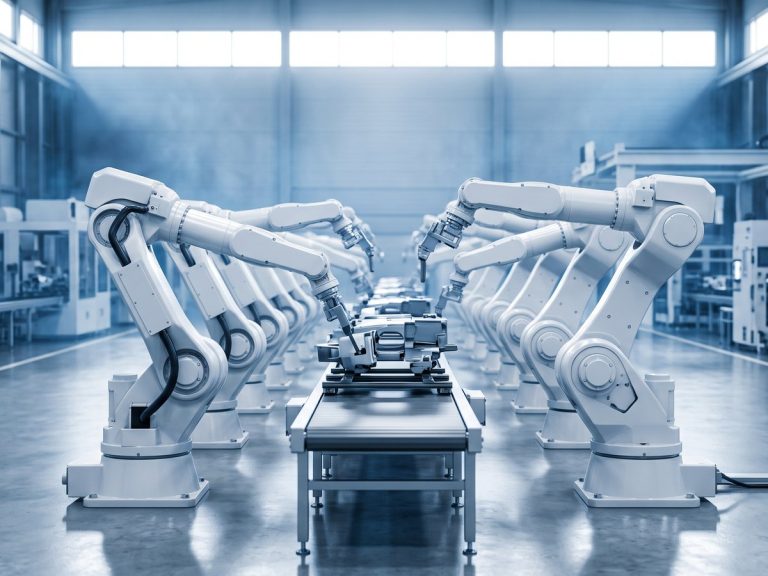 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
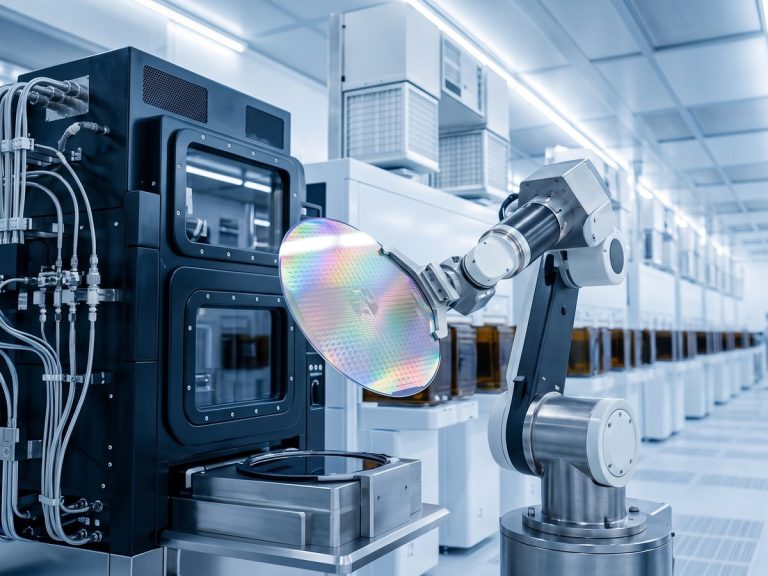 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Typical Ground Parts and Challenges
Grinding is material-agnostic: the wheel is chosen for the material, so the same cell finishes shafts, pins, plates and carbide.
-

Shafts & Spindles
Ground bearing seats, shoulders and tapers on motor and gearbox shafts, often machined first at DEK as custom shafts.
-

Pins & Gauges
Ejector, core and dowel pins, plug gauges, ring gauges and gauge plates held to ±0.002 mm on diameter or thickness.
-

Mold & Die Components
Punches, die inserts and mold plates ground flat and parallel, many machined first as mold components at DEK.
-

Bushings & Sleeves
Bushings, guide sleeves and valve spools where the bore-to-OD relationship matters more than either dimension alone.
-

Seal Faces & Carbide Parts
Seal faces, valve plates and tungsten carbide wear parts lapped flat to 0.001 mm, Ra 0.05–0.1 µm.
Grinding Challenges We Handle
-
Heat-Treat Distortion
Heat treatment moves dimensions by 0.02–0.1 mm. We leave 0.2–0.5 mm stock, harden, then grind using unground features or centers as the datum.
-
Hardened Material
Parts above about 45 HRC cannot be finish-machined at a useful rate. Tool steels at 58–62 HRC take aluminum oxide or CBN wheels; carbide takes diamond.
-
Shoulder Run-Out
Where a ground diameter meets a shoulder, a relief groove or undercut lets the wheel run out without leaving a fillet.
-
Case-Hardened Parts
Case depth must exceed the grinding stock. State the hardness range and whether the part is through or case hardened so the allowance is set right.
Certified Grinding Quality
Ground parts are made under ISO 9001:2015, ISO 13485 and AS9100D, certified by TÜV.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Materials and Finishes for Ground Parts
We grind hardened steels, stainless and carbide, then apply the finishes that must follow grinding, all in one CNC machining order.
Surface Finishes
Hardened Grades
Grinding a material not listed here? See all CNC machining materials
All FinishesHeat Treatment and Grinding Sequence
Precision Grinding FAQ
Tolerances, honing vs lapping and grinding stock, answered by our grinding engineers.
Request a Grinding Quote
Send your drawing with hardness, ground features and surface finish marked. An engineer confirms grinding allowance and sequence before quoting.
- Quote within 6 hours for most parts
- Tolerances to ±0.002 mm, Ra 0.2–0.4 µm
- Machining, heat treatment and grind in one order
- No minimum order quantity
- Dimensional reports on request

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.