









Precision 4-Axis CNC Machining
4-axis CNC machining adds a rotary A-axis to X, Y, Z travel, holding ±0.005 mm on multi-face parts in one fixturing. No MOQ, and prototypes ship in 3 days.
-
±0.005 mm
Standard Tolerance
-
3 Days
Prototype Delivery
-
~1000 mm
Max Part Size
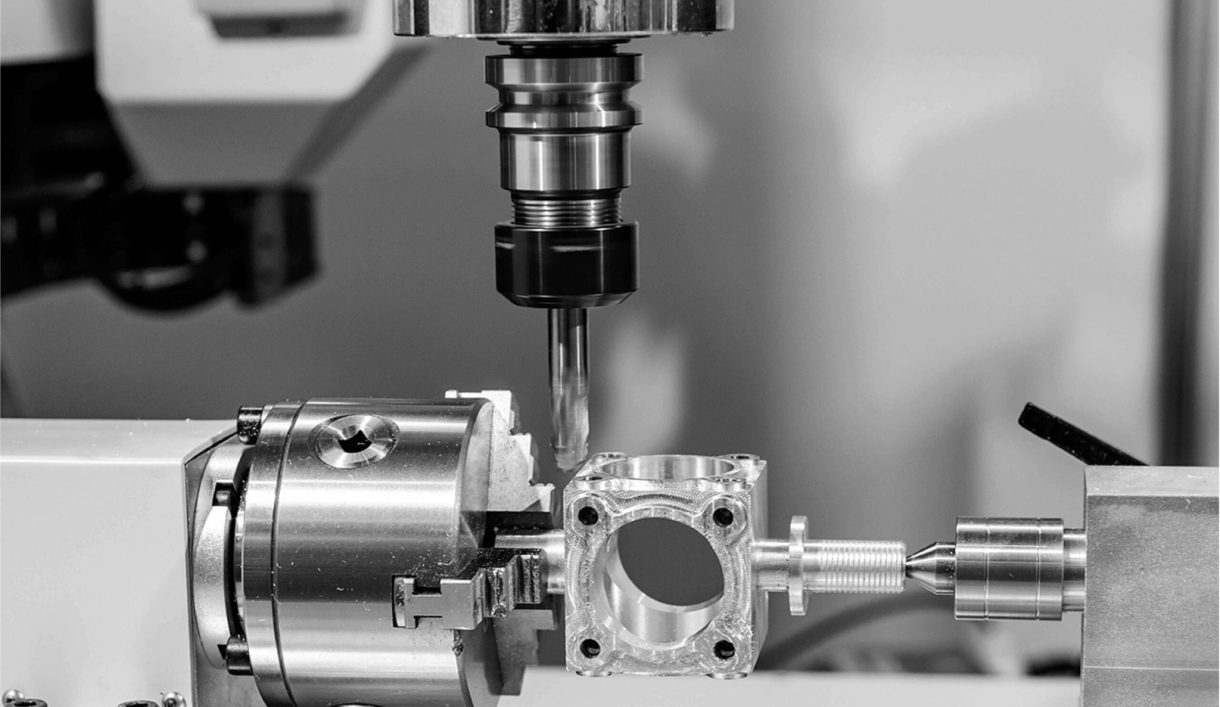

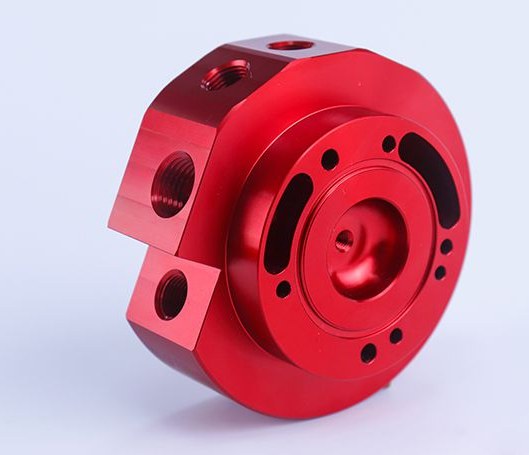
4-Axis CNC Machining Services for Multi-Face Parts
DEK runs 4-axis equipment in two modes: indexed, where the part stops rotating before each cut, and continuous, where the A-axis turns while cutting for cam profiles, spiral grooves and helical features.
One setup reaches front, back and side faces that would otherwise need separate fixtures and re-zeroing. For single-face prismatic parts, 3-axis CNC machining is usually cheaper; to weigh axis count against geometry, see 5-axis CNC machining or our full multi-axis machining range.
Why DEK for 4-Axis Machining
A long precision machining track record matters most on multi-face parts, where every re-fixturing step can cost accuracy.
-

20+ Years Experience
DEK has more than 20 years in precision machining, applied to indexed and continuous rotary-axis programs in metals and engineering plastics.
-

1.2M+ Parts per Year
We produce over 1.2 million parts annually for 2,300+ global OEM clients, from a single prototype to production runs with no MOQ.
-

98.6%+ On-Time Delivery
A 98.6%+ on-time delivery rate, with prototypes of 1–10 pieces typically shipping in 3 days and global shipping on every order.
-

Single-Setup Accuracy
A single-setup 4-axis program removes the re-fixturing errors that hurt accuracy on repositioned jobs, holding ±0.005 mm on standard features.

DFM Review Before Quoting
Our engineers review every drawing before quoting and flag features that are hard to reach on a rotary setup: undercuts, awkward fixturing points, or tolerances that would need grinding after machining.


4-Axis Capability, Tolerances & Lead Times
Specs for our rotary-axis work: tolerances by feature type, lead times by volume, working envelope and the materials we cut.
4-Axis vs. 3-Axis CNC Machining
A 4th axis isn't always the right call: choose it when features sit on several faces. For single-face parts, standard CNC milling on 3 axes usually costs less.
| Criteria | This Process4-Axis CNC Machining | 3-Axis CNC Machining |
|---|---|---|
| Best for | Multi-face and radial parts | Single-face prismatic parts |
| Faces per setup | Front, back and sides | One direction |
| Angled features | Via A-axis rotation | Needs repositioning |
| Helical grooves | Continuous A-axis cuts | Not on a stationary part |
| Relative cost | Higher (rotary setup) | Usually cheaper |
| Choose when | Features on several faces | Pockets, holes on one side |
4-Axis Parts for Key Industries
Stepped shafts, brackets, manifolds and housings for aerospace, automotive and marine programs, plus gear blanks and tooling bodies.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Typical 4-Axis Parts & Challenges
Parts that need more than one face machined without breaking the original fixture are natural fits for a 4th axis.
-

Stepped Shafts
Radial holes and flats cut around shafts in one setup, with bores held to ±0.005 mm.
-

Side-Drilled Brackets
Holes and slots on opposing faces of brackets without re-zeroing between operations.
-

Manifolds
Manifolds with ports on several faces, machined for automotive programs in one fixturing.
-

Gear Blanks & Hubs
Blanks and hubs indexed on the A-axis and cut through our gear machining service.
-

Rotational Housings
Pump and rotational housings machined on multiple faces in one setup, including shafts and housings for marine programs.
-
Fixture Plates & Tooling
Fixture plates and tooling bodies finished with jig boring for precise hole patterns.
Common Challenges We Handle
-
Undercuts on Rotary Setups
Our engineers flag undercuts that are hard to reach on a rotary setup during drawing review, before production starts.
-
Awkward Fixturing Points
Awkward fixturing points are identified before quoting, so issues surface early instead of during the run.
-
Grinding-Level Tolerances
Tolerances that would need precision grinding after machining are flagged at DFM review.
-
Re-Fixturing Errors
A single-setup 4-axis program removes the re-fixturing errors that hurt accuracy when a part is repositioned between faces.
Certified Quality on Every 4-Axis Job
In-house CMM inspection, IQC to CAPA controls and full traceability from raw material to shipment.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
50+ Metals and Engineering Plastics
Rotary setups run on the same metals and plastics we machine every day. Pick the material that fits your part.
Engineering Plastics
Need another alloy or polymer? See plastic CNC machining
View AllHow to Order 4-Axis Machined Parts
4-Axis Machining FAQs
Answers to the questions engineers ask most about rotary-axis machining at DEK.
Get a Quote for Custom 4-Axis Machining
Send a 2D or 3D drawing and our engineers will quote your 4-axis part, with the working envelope confirmed for your part size.
- No MOQ, from one prototype to production
- Prototypes in 3 days
- Free DFM review before quoting
- Tolerances to ±0.005 mm, CMM inspected
- Global shipping with full traceability







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








