Precision Sinker EDM Services
DEK sinker EDM services burn blind cavities, deep ribs and sharp internal corners in hardened tool steel and carbide at ±0.01mm typical. No MOQ and 3-day prototype lead times.
-
±0.005mm
Critical Features
-
3 Days
Fastest Prototype
-
Ra 0.15 μm
Finest Finish

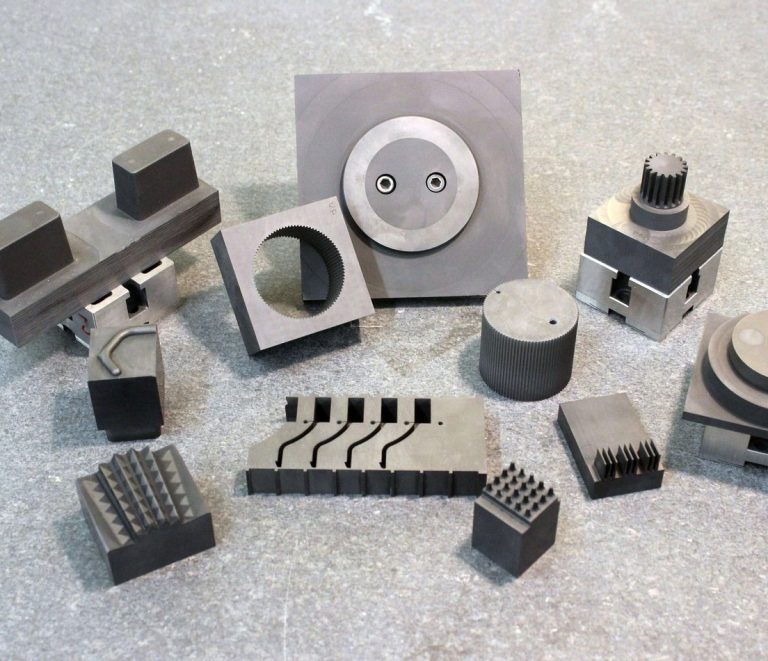
Custom Sinker EDM for Molds, Dies and Tooling
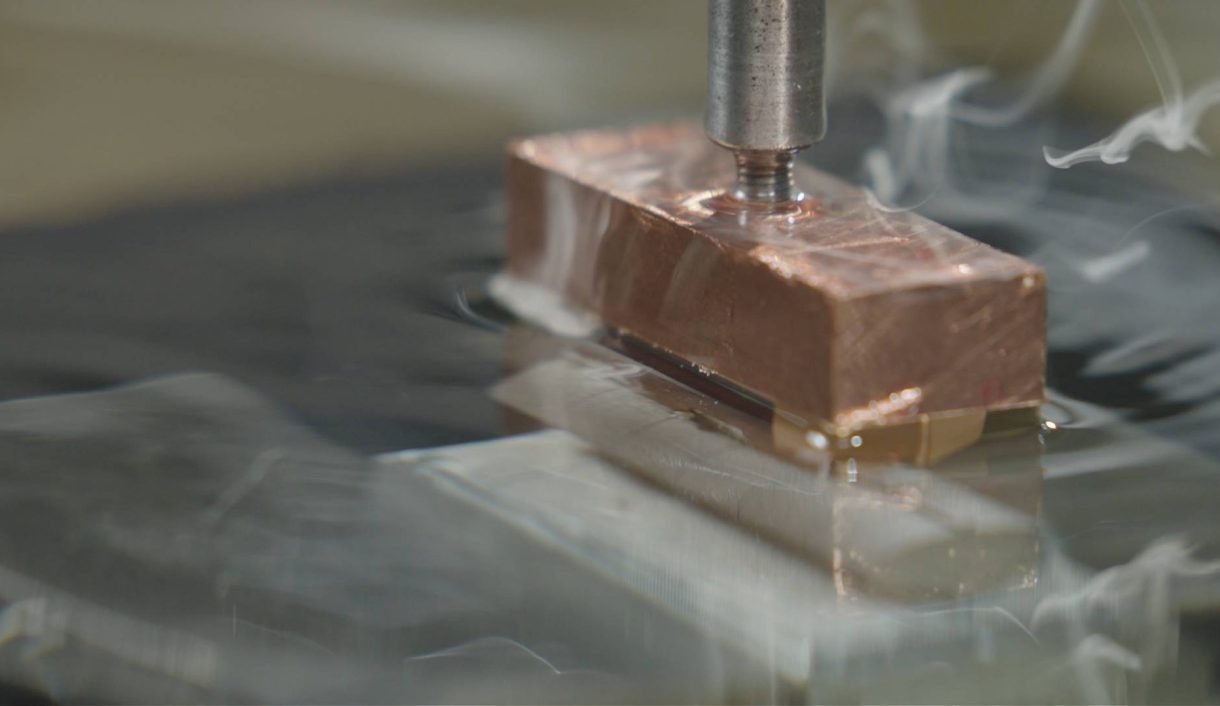
Sinker EDM, also called die sinking, erodes a shaped electrode into a conductive workpiece without touching it or inducing stress. The spark, wear and flushing mechanics are explained in The Ultimate Guide to Sinker EDM.
DEK runs it for moldmakers, aerospace and medical toolmakers, and anyone finishing hardened tool steel or carbide after heat treat, with 20+ years in precision machining. Through features usually go to wire EDM services; all processes sit under our EDM machining services.
Why DEK for Sinker EDM
A broader precision machining operation behind every electrode-burned cavity, from a lone mold insert to a full set.
-

Certified Quality
ISO 9001, AS9100D and ISO 13485 (via TUV) certified, with every cavity going through IQC, IPQC, FAI, OQC, SPC and CAPA.
-

Proven at Scale
Sinker EDM runs inside an operation that machines 1.2M+ parts annually for 2300+ global OEM clients.
-

On-Time Delivery
A 98.6%+ on-time delivery rate, with prototype orders shipping in as little as 3 days once production starts.
-

On-Demand EDM Machining
No MOQ: a single mold insert moves through the same inspection chain as a full production cavity set.

Electrodes Made In-House
Copper electrodes are machined in-house, and that work sits inside the 3-day prototype lead time quoted for the finished part, not as a separate line item. Talk to a sinker EDM engineer before you release the drawing.
Sinker EDM Services Capabilities
Axis setup, precision, hardened materials and electrode work: the core specifications behind every sinker EDM job at DEK.
Sinker EDM vs. Wire EDM and CNC Milling
Choose sinker EDM when the feature must stay blind. For through features, see the wire cut EDM guide.
| Criteria | This ProcessSinker EDM | Wire EDM | CNC Milling |
|---|---|---|---|
| Best for | Blind cavities, keyways, ribs | Slots, gear teeth, profiles | Features tools can reach |
| Feature geometry | Closed bottom, stops at depth | Runs through the part | Open, reachable features |
| Internal corners | Sharp | Contoured profiles | Tool-radius limited |
| Hardened tool steel | Yes, after heat treat | Through-cut features | Tools wear fast |
| Aluminum | Blind features only | Through features | Preferred, cuts easily |
| Choose when | Through-cut not possible | Faster, cheaper through-cuts | Soft, accessible geometry |
Industries We Serve
Sinker EDM for moldmakers, aerospace and medical toolmakers, and turbine and engine tooling in high-temperature alloys.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Mold and Die EDM Features We Burn
The electrode plunges to depth and stops, reaching geometry that milling tools cannot cut without deflection or radius limits.
-

Blind Cavities
Mold and die cavities with a closed bottom, burned to depth while the rest of the part stays untouched.
-

Blind Keyways
Blind keyways sunk to depth where a through-cut is not acceptable or not possible on the finished part.
-

Deep Narrow Ribs
Narrow ribs that need a closed bottom, formed by the electrode in one plunge without cutter reach limits.
-

Thin Walls
Non-contact erosion avoids the deflection milling runs into on thin walls in tool steel and carbide.
-

Sharp Internal Corners
Inside corners free of the tool-radius limits of milling, for mold components.
-
Textured Mold Cavities
Textured cavity surfaces and pockets for mold making, finish down to Ra 0.15 μm.
Common Challenges We Handle
-
Post-Heat-Treat Parts
Hardened tool steel and carbide are finished after heat treat, when conventional cutting tools wear out fast or cannot cut.
-
Damaged Hole Repair
Worn or damaged bores and cavity walls are cleaned up in place without altering the part's original form or position.
-
Single Mold Inserts
No MOQ: one insert follows the same FAI and OQC chain as a set; see prototype machining.
-
Blind Features in Aluminum
Aluminum burns cleanly but is usually milled; sinker EDM is reserved for blind features milling cannot reach.
Certified Quality at Every Stage
Every sinker EDM job runs under ISO 9001, AS9100D and ISO 13485 (via TUV) certification.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Materials We Sinker EDM
Any conductive metal burns with sinker EDM. These are the hardened and high-performance alloys we run most often.
Material not listed? Ask a sinker EDM engineer
View MaterialsHow to Order Sinker EDM Parts
Sinker EDM FAQs
Straight answers on accuracy, materials and what we need to quote your part.
Get a Sinker EDM Quote
Send a STEP, IGES or PDF drawing with material, hardness state and critical cavity dimensions for an engineer-reviewed quote.
- Prototypes ship in as little as 3 days
- No MOQ, from one insert to a full set
- ±0.01mm typical, ±0.005mm on request
- Copper electrodes machined in-house
- ISO 9001, AS9100D, ISO 13485 certified

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.