









Precision CNC Drilling Services
DEK's CNC drilling services hold dowel hole true position to ±0.005 mm in 50+ metals and plastics. Holes are cut in the same setup as milling or turning, with no MOQ.
-
±0.005mm
True Position
-
3 Days
Fastest Prototype
-
98.6%+
On-Time Delivery
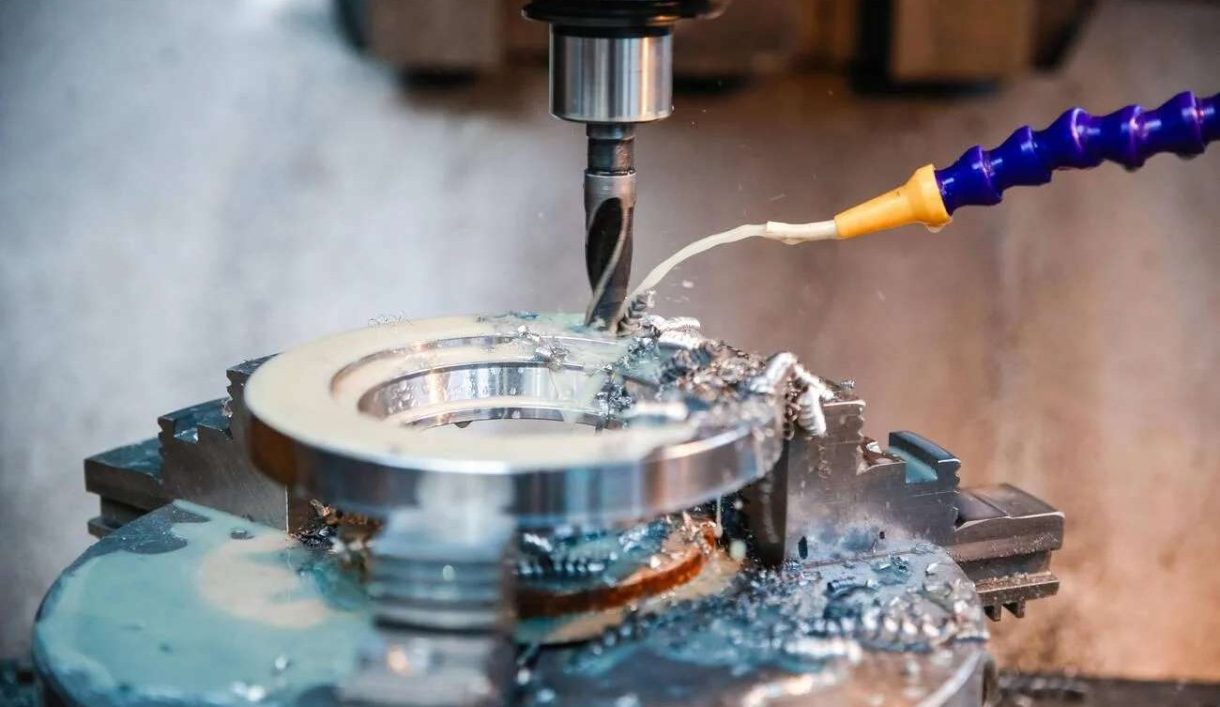

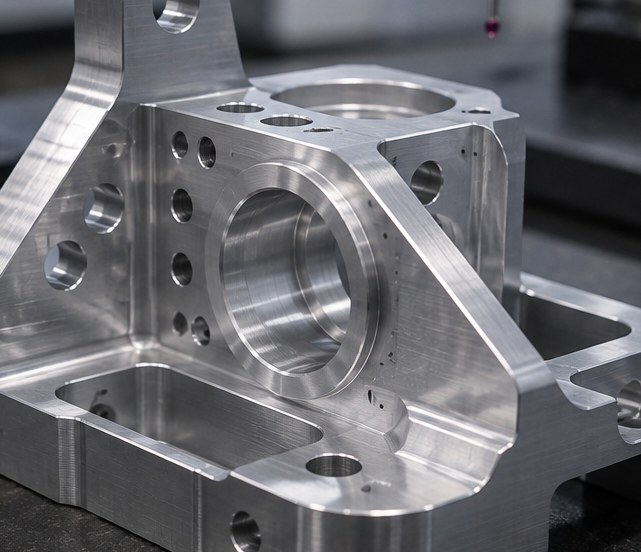
Precision Hole Drilling for Milled and Turned Parts
DEK drills through holes, blind holes, positioning/dowel holes, and counterbore or countersink features in 50+ metals and engineering plastics. Holes are cut on the same datum as the surrounding CNC milling or CNC turning operation.
Position tolerance carries through the whole part instead of resetting for a separate drilling pass. There is no MOQ, prototypes ship in as fast as 3 days, and our engineers confirm hole tolerance, material, and lead time before you commit, with general dimensions per ISO 2768.
Why Choose DEK for CNC Drilling
Drilled holes are usually one feature inside a larger milled or turned part. Here is why OEM buyers trust DEK with them.
-

20+ Years of Machining
DEK has run precision machining for 20+ years, producing 1.2M+ parts annually for 2300+ global OEM clients across Europe and North America.
-

98.6%+ On-Time Delivery
Prototype lead time runs as fast as 3 days; production lead time is confirmed once hole count, material, and tolerance are set.
-

Same Setup, Same Datum
Drilling runs on the same setup, datum, and inspection pass as the rest of the component, so there is no separate alignment error to track.
-

No Minimum Order Quantity
Order a single prototype or a production run: there is no minimum order, and every quantity gets the same engineer-reviewed drawing check.

Engineer-Reviewed Drawings
Our engineers flag holes beyond a 10:1 depth-to-diameter ratio, very small diameters in hard alloys, and cross-holes near thin walls, then confirm tolerance, material, and lead time before pricing.


CNC Hole Drilling Services Capabilities
Hole type drives tooling, setup, and inspection method. We select the drilling sequence around what your drawing calls for.
CNC Drilling vs. Other Hole-Making Processes
Choose CNC drilling for plain holes up to about 10:1 deep; switch process for deeper holes, threads, or H7 fit bores.
| Criteria | This ProcessCNC Drilling | Deep Hole Drilling | Tapping | Boring / Grinding |
|---|---|---|---|---|
| Best for | Through, blind, dowel holes | Long, straight holes | Internal threads | H7 fit bores |
| Depth-to-diameter | Up to ~10:1 | Beyond ~10:1 | Per thread callout | Follow-up on drilled bore |
| Typical tolerance | ±0.005 mm true position | Confirmed on review | Confirmed on review | H7 fit class |
| Limiting factor | Tool access, material | Straightness, coolant | Thread tooling | Fit class on drawing |
| Choose when | Plain hole in same setup | Hole exceeds 10:1 | Hole needs threads | Bore needs a press fit |
Drilled Parts for Every Industry
We drill parts for aerospace (non-flight-critical), medical devices, robotics, semiconductor equipment, automation, and automotive programs.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Hole Features and Challenges We Solve
From micro holes to large plates, these are the hole features our engineers drill and the drawing risks we flag early.
-

Blind Holes
Controlled-depth holes for standoffs and sealing faces. Conical bottom by default, flat bottom when the drawing calls it out.
-

Counterbores & Countersinks
Recessed seats for flush fastener heads: counterbores defined by diameter and depth, countersinks by included angle and depth.
-

Dowel & Locating Holes
True position and coaxiality between mating dowel and locating-pin holes held to ±0.005 mm for repeatable alignment.
-

Micro Holes
Holes in sub-10 mm parts down to ±0.003 mm through our micro machining setup.
-

Holes in Large Parts
Drilling on parts up to about 1000 mm, run with our large part CNC machining capacity.
-
Multi-Face Hole Patterns
Holes on several faces cut on 4- and 5-axis platforms, with profile features held to ±0.01 mm.
Hole Features We Flag Early
-
Holes Beyond 10:1
Depth-to-diameter ratios beyond roughly 10:1 limit straightness and coolant delivery, so they route to deep hole drilling.
-
Small Holes in Hard Alloys
Very small diameters in titanium or Inconel run slower and wear tooling faster; we confirm tolerance and lead time before pricing.
-
Cross-Holes Near Thin Walls
Cross-holes located close to thin walls are reviewed on the drawing so tolerance and lead time are confirmed before quoting.
-
Finish-Free Bores
Press-fit or threaded holes that must stay uncoated are flagged before anodizing, plating, or powder coating is applied.
Certified Quality on Every Hole
Drilling runs under our ISO 9001, AS9100D, and ISO 13485 certified quality system.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
50+ Materials for Drilled Parts
Hard alloys hold tighter position but run slower than aluminum or plastics. We drill across our full metal and plastic range.
Surface Finishes
Engineering Plastics
Need another material or finish? Talk with our engineers.
All MaterialsHow to Order CNC-Drilled Parts
CNC Drilling FAQs
Answers on hole tolerance, design review, and lead time for drilled parts.
Request a Quote for CNC Drilling Services
Send your 3D CAD file and 2D drawing. Our engineers confirm hole tolerance, material, and lead time before quoting a price.
- Prototypes in as fast as 3 days
- No MOQ, from one part to production
- True position held to ±0.005 mm
- 50+ metals and plastics drilled
- CMM inspection with full traceability







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








