









Custom Jigs and Fixtures Manufacturing
DEK machines custom jigs and fixtures from your drawings, with locator holes jig-bored to ±0.005 mm. No MOQ, and a single fixture ships in 3–5 days.
-
±0.005 mm
Jig-Bored Holes
-
0.01 mm
Flat Over 300 mm
-
3–5 days
Single Fixture
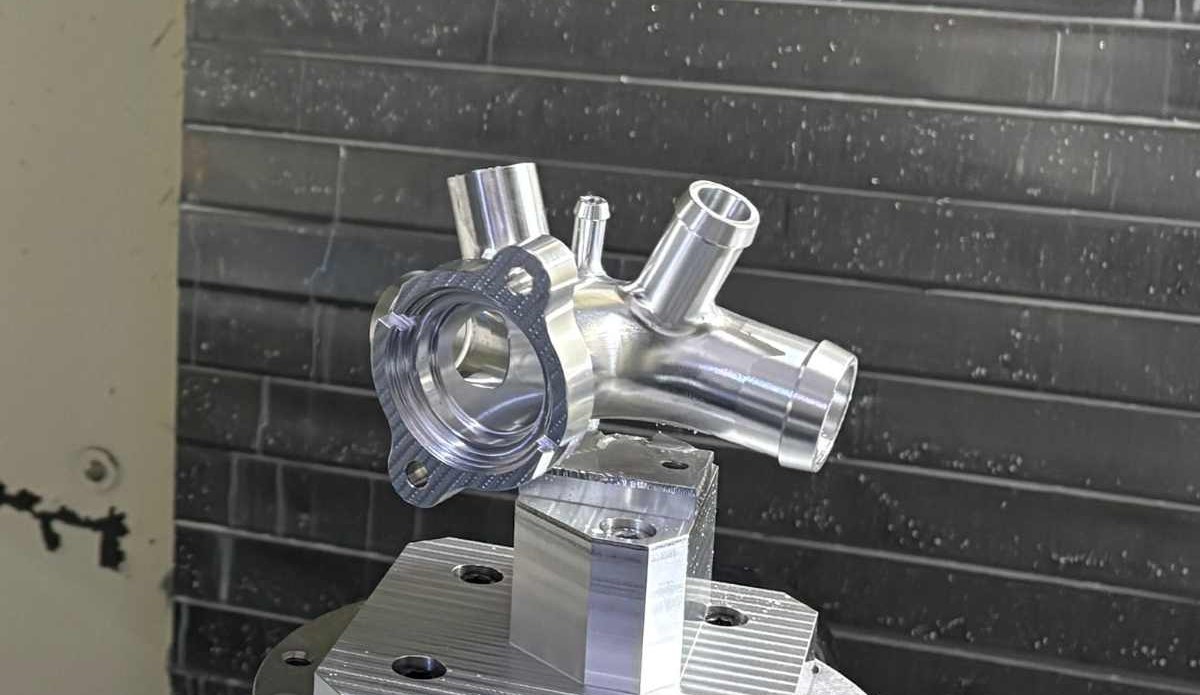

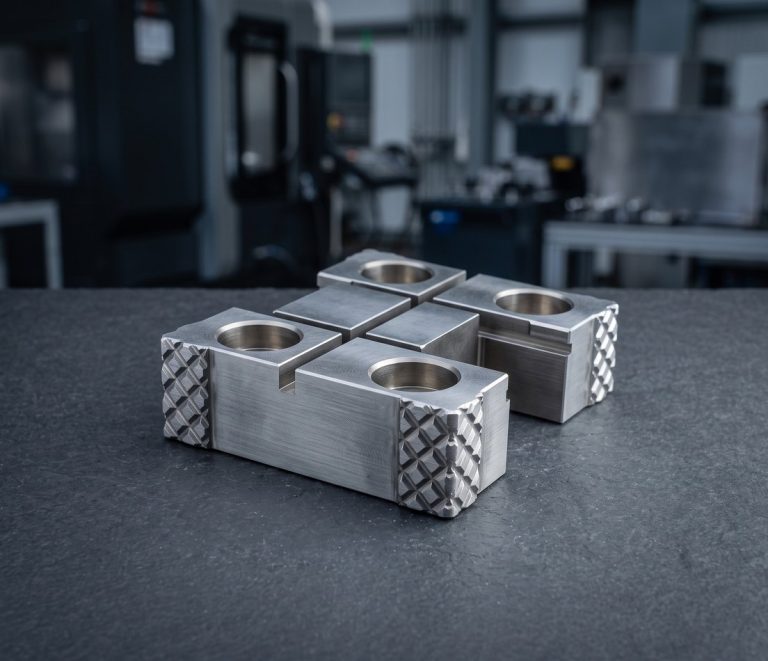
Custom Workholding and Fixtures to Your Drawing
DEK machines machining fixtures and fixture plates, soft jaws, drill jigs, welding and assembly fixtures, inspection and CMM fixtures, test nests, and end-of-arm tooling fingers in aluminum, tool steel, and Delrin.
Plates are ground flat to 0.01 mm over 300 mm, holes are jig-bored to ±0.005 mm, and pin-to-pin distances hold ±0.01 mm. We build to customer designs and do not offer fixture design. Part of our custom CNC machined parts catalogue.
Types of Jigs and Fixtures We Machine
From fixture plates and soft jaws to inspection nests and robot fingers, machined from cast plate, tool steel, and Delrin.
-
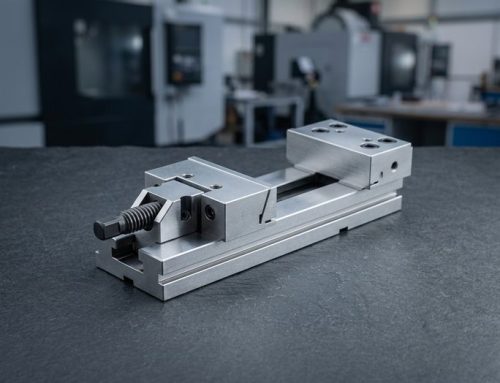 Custom WorkholdingFixture plates, tombstone adapters, soft jaws, and sealed vacuum chucks.
-
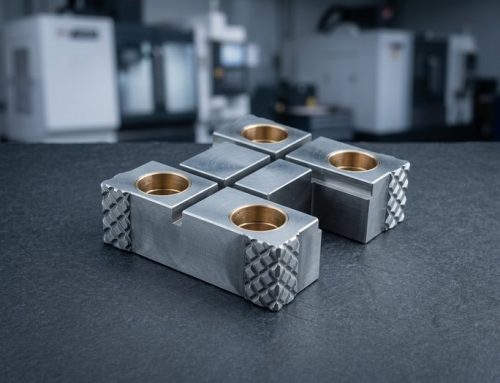 Drill and Reaming JigsHardened, ground bushings set at jig-bored positions for repeat drilling.
-
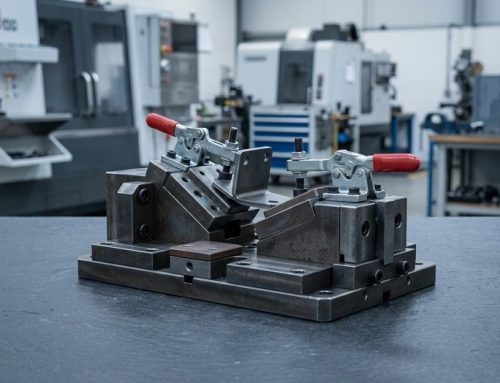 Welding FixturesLocators, clamp pads, and heat-resistant rest blocks for weld cells.
-
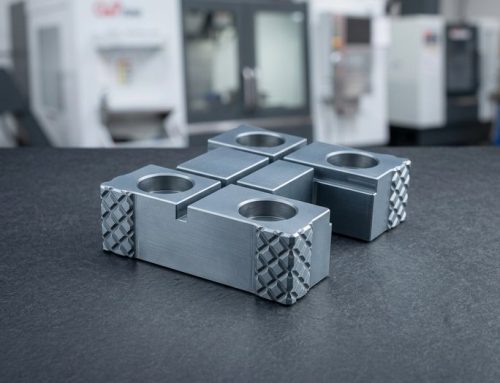 Assembly Fixtures and NestsNests for press-fitting, bonding, and screw-driving stations.
-
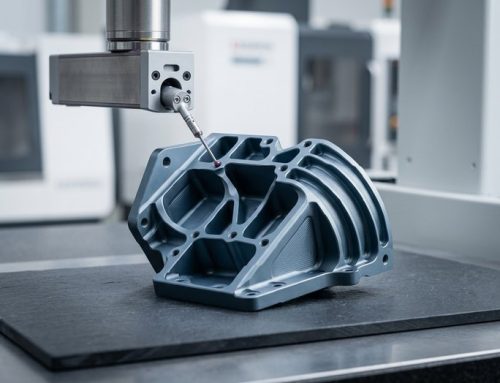 Inspection FixturesCMM holding fixtures, go/no-go gauges, and checking fixtures with datum pins.
-
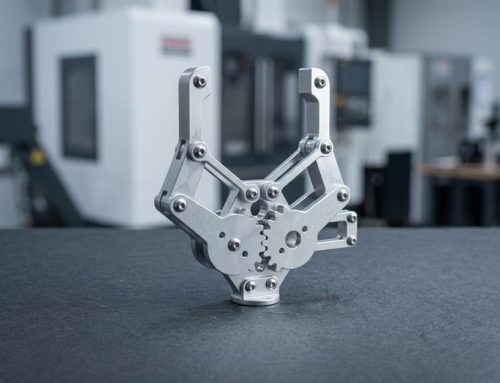 End-of-Arm Tooling FingersGripper fingers, gripper pads, and vacuum cup holders for robots.


Fixture Materials, Processes & Tolerances
How DEK builds fixture plates, locators, and nests: stable plate stock, ground datums, jig-bored holes, and hardened details.
Design Tips for Custom Jigs and Fixtures
Five drawing habits that keep locators accurate, plates flat, and wear surfaces replaceable on a machined fixture.
-

One Datum Corner
Dimension all locator holes as coordinates from one datum corner; chain dimensions accumulate error across a plate.
-

Round Plus Diamond Pin
Locate with one round and one diamond pin; two round pins over-constrain the part and fight the tolerance.
-

MIC6 for Deep Pockets
Specify MIC6 or 6061-T651 for plates pocketed deeper than 10 mm; extruded 6061 bar warps as stock is removed.
-

Replaceable Contact Points
Put hardened, replaceable rest buttons or bushings at every contact point instead of wear surfaces in the soft base.
What to Call Out on Your Drawing
-
Ground Faces
Call out ground faces explicitly with flatness and Ra; a milled face at 0.05 mm flatness looks identical on a drawing.
-
Datum Scheme
Send the datum scheme and locator positions; every plate is checked on a surface plate and CMM against it.
-
Hardware List
List pins, bushings, and clamp hardware; DEK supplies hardened pins and bushings machined in-house in the same order.
-
STEP Model and Drawing
Send a STEP model with the drawing; engineers flag issues such as wall thickness or unreachable features at quote review.
Applications & Industries
Assembly and test cells for automation, gripper fingers and pallets for robotics, PCB test nests for electronics, and washdown fixtures for medical lines.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Why DEK for Jig Manufacturing
Grinding, jig boring, wire EDM, and ground pins in one order: DEK's original trade since 2002.
-

One Shop, One Order
DEK grinds, jig-bores, wire-cuts, and supplies the ground pins and bushings for your fixture in a single order.
-

Fixture Work Since 2002
Grinding, jig boring, wire cutting, and ground pins and bushings have been DEK's original trade since 2002.
-

Coordinate Report
Every fixture plate is checked on a surface plate and CMM against your datum scheme, and a coordinate report ships with it.
-

No MOQ, 3–5 Days
One-off fixtures are quoted with no MOQ and typically ship in 3–5 days, including hardened pins and bushings.

Engineer-Reviewed Quotes
Every drawing is reviewed by an engineer before quoting. We do not design fixtures, but we flag manufacturability issues such as wall thickness or unreachable features during quote review.
Certified Fixture Quality
ISO 9001:2015, ISO 13485, and AS9100D certified for every fixture we machine.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Fixture Materials and Finishes
The plate stocks, tool steels, and finishes we use for custom jigs and fixtures, each chosen for flatness or wear.
Surface Finishes
Need another material for your fixture? Ask our engineers.
All MaterialsJigs and Fixtures FAQ
Answers on design scope, tolerances, and one-off orders for machined fixtures.
Get a Quote for Custom Jigs and Fixtures
Send a STEP model and drawing for an engineer-reviewed quote within 6 hours; multi-part fixture assemblies are quoted within 3 days.
- Datum scheme and locator positions
- Ground faces with flatness and Ra
- Hardware list: pins, bushings, clamps
- No MOQ; one-offs ship in 3–5 days







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








