Swiss machining is a CNC turning process that feeds bar stock through a sliding headstock and a guide bushing, so the cutting tool works right at the point where the material is supported. That support point is what lets Swiss lathes hold tight tolerances on long, slender parts that would flex, chatter, or go out of round on a standard lathe.
What Is Swiss Machining? (The Core Definition)
On a conventional lathe, the workpiece is clamped in a fixed headstock and stays still while the cutting tool moves along it. The farther the tool works from the chuck, the more the unsupported stock can flex under cutting force, a real problem for long, thin parts.
Swiss machining flips that setup. The headstock slides, moving the bar stock itself along the Z-axis and pushing it through a hardened guide bushing positioned right next to the cutting tools. The bushing supports the material within a few thousandths of an inch of where it's actually being cut. Deflection drops sharply, so shops can hold tight dimensions on parts with high length-to-diameter ratios, exactly the geometry that breaks down on a fixed-headstock machine. It's still CNC turning at its core; the difference is entirely in how the stock is supported and advanced.
What Is Swiss Style Machining?
"Swiss machining," "Swiss-type turning," "Swiss style machining," and "Swiss lathe" all refer to the same family of process; there's no meaningful technical difference between the terms, just different ways people say it depending on region or industry. The name comes from its origin: Switzerland's watchmaking industry, which needed a way to produce extremely thin, precise components and developed the sliding-headstock lathe to do it in the late 1800s. The mechanism spread from watches to every industry that needs small, slender, high-precision parts, but the "Swiss" name stuck.
How Does a Swiss Lathe Work?
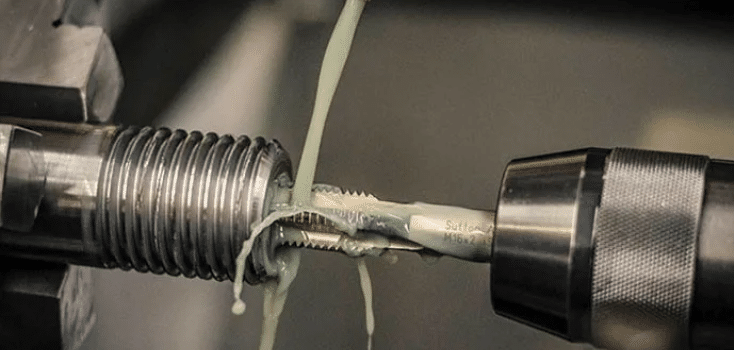
In-process threading with active coolant flow: one of several operations a Swiss lathe can perform in a single setup alongside turning and drilling.
A Swiss lathe is a CNC machine (programmed, automated, and repeatable like any other CNC turning center) but built around that sliding headstock and guide bushing pairing. Bar stock advances through the bushing along the Z-axis while cutting tools, arranged around the machining zone, work the exposed material close to the support point. Because tools stay in fixed positions and the material moves rather than the other way around, several operations can happen almost simultaneously.
Under ideal conditions, industry-standard Swiss lathes can hold tolerances as tight as ±0.0002 in (roughly ±0.005 mm), though what's actually achievable depends on stock quality, tooling rigidity, and thermal control on a given job. Bar capacity on most Swiss machines runs from about 4 mm up to 32 mm diameter stock, which covers the large majority of small-part production. Many machines can also run in a guideless (chucker) mode that removes the guide bushing entirely, useful for shorter parts where the extra support isn't needed and setup speed matters more than maximum length-to-diameter ratio.
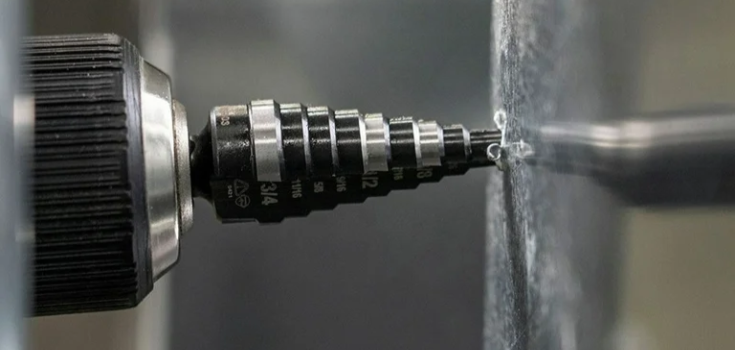 Cross-drilling a feature mid-cycle; live tooling lets a Swiss lathe drill, mill, or thread without moving the part to a second machine.
Most Swiss lathes carry live tooling, meaning some tools rotate independently rather than just cutting statically. That's what lets a single setup turn a diameter, drill a cross-hole, cut threads, and mill a flat on the same part without moving it elsewhere. High-pressure coolant is standard, both to clear chips from small features and to keep thermal growth from drifting the tolerance during longer runs.
What Does a Swiss Machinist Do?
A Swiss machinist's job centers on setup accuracy and constant monitoring, more than on the cutting itself once a job is running. Typical tasks include:
- Selecting and installing the guide bushing sized to match the bar stock diameter; a mismatch here is the single fastest way to introduce deflection or scrap a run.
- Programming multi-axis toolpaths and live tooling sequences so turning, drilling, threading, and milling operations happen in the correct order within one cycle.
- Loading and adjusting bar feeders, since Swiss work is bar-fed and the feeder has to keep pace with the spindle without introducing vibration.
- Monitoring bar-fed cycles in real time, watching for chip evacuation issues, tool wear, and thermal drift that can shift tight tolerances mid-run.
- Inspecting micro-tolerance features with optical comparators or CMM equipment, since the parts Swiss machines produce often carry tolerances too tight to check reliably by hand.
- Changing collets, bushings, and tooling between jobs as stock diameter or part geometry changes.
It's a skill set built around precision setup and process control rather than manual cutting; the machine does the cutting, the machinist makes sure it's cutting the right thing, the right way, every time.
What Materials Work Best in Swiss Machining?
Swiss machining works well with any material that machines cleanly at small diameters and doesn't gall or work-harden excessively under the tight cutting geometry:
- Stainless steel: holds tight tolerances and corrosion resistance for parts that need both strength and a clean finish.
- Titanium: favored where strength-to-weight ratio matters, though its poor heat conductivity demands careful coolant and feed control.
- Brass and copper alloys: machine easily at high speed and are common in connectors, fittings, and small precision hardware.
- Engineering plastics (PEEK, PTFE): used for insulating or chemically resistant components where metal isn't an option.
Where Is Swiss Machining Used? (Applications & Industries)
Bone screws and other implantable fasteners need full material traceability to satisfy ISO 13485 quality requirements, which is one reason medical machining programs document every lot back to its source stock. The regulatory and material requirements specific to implants and surgical instruments get fuller treatment in the complete guide to medical machining. Titanium and 316L stainless dominate the metals used in medical equipment for their biocompatibility and corrosion resistance, and both machine well on a Swiss lathe. Some implant geometries (porous or lattice structures for bone in-growth, for instance) aren't turned parts at all; those fall to additive processes instead, and 3D printed medical devices covers the materials and design rules specific to that side of medical manufacturing.
Small connector pins and contact housings used in circuit assemblies are routinely produced through CNC machining in the electronics industry, another category built almost entirely from small-diameter, high-volume parts. Automotive fuel and fluid fittings, and small aerospace fasteners, round out the common use cases: anywhere a part is long relative to its diameter and the tolerance stack-up leaves no room for deflection.
Benefits and Limitations of Swiss Machining
Swiss machining isn't the right call for every turned part; it earns its keep on specific geometries and volumes.
| Factor | Swiss Machining | Conventional (Fixed-Headstock) Turning |
|---|---|---|
| Best part geometry | Long, slender, small-diameter | Larger diameter, shorter length |
| Material deflection | Minimized by guide bushing support | Higher risk on unsupported length |
| Operations per setup | Turning, drilling, milling, threading combined | Often needs secondary setups |
| Setup cost, short runs | Higher: bushing/tooling setup takes time | Lower, faster to set up |
| Best for | High-volume, small-diameter, tight-tolerance parts | Large or simple parts, low volume |
Three practical costs come with that precision. Guide bushings require ground bar stock (often called SMQ, or screw-machine-quality stock) rather than commercial-grade bar, and ground stock costs more per pound. Every bar also leaves an unusable remnant once it's too short to feed through the bushing safely, so real material yield is lower than it looks on paper. And on harder-to-machine metals like titanium, poor heat conductivity concentrates heat at the cutting edge and produces long, stringy chips that can tangle in the tooling; chip and coolant control need closer attention on a Swiss lathe than they do on larger-diameter conventional turning.
The trade-off is straightforward: Swiss machining's guide-bushing setup and specialized tooling take longer to configure, which makes it less economical for very short runs or large-diameter parts that don't need the extra support in the first place. For those jobs, conventional turning is usually cheaper and faster to set up; the CNC turning cost breakdown covers what drives pricing on that side of the comparison.
Need Swiss-Turned Parts?
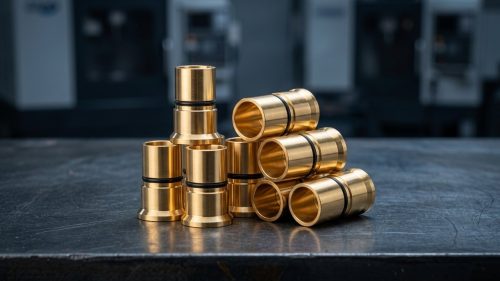
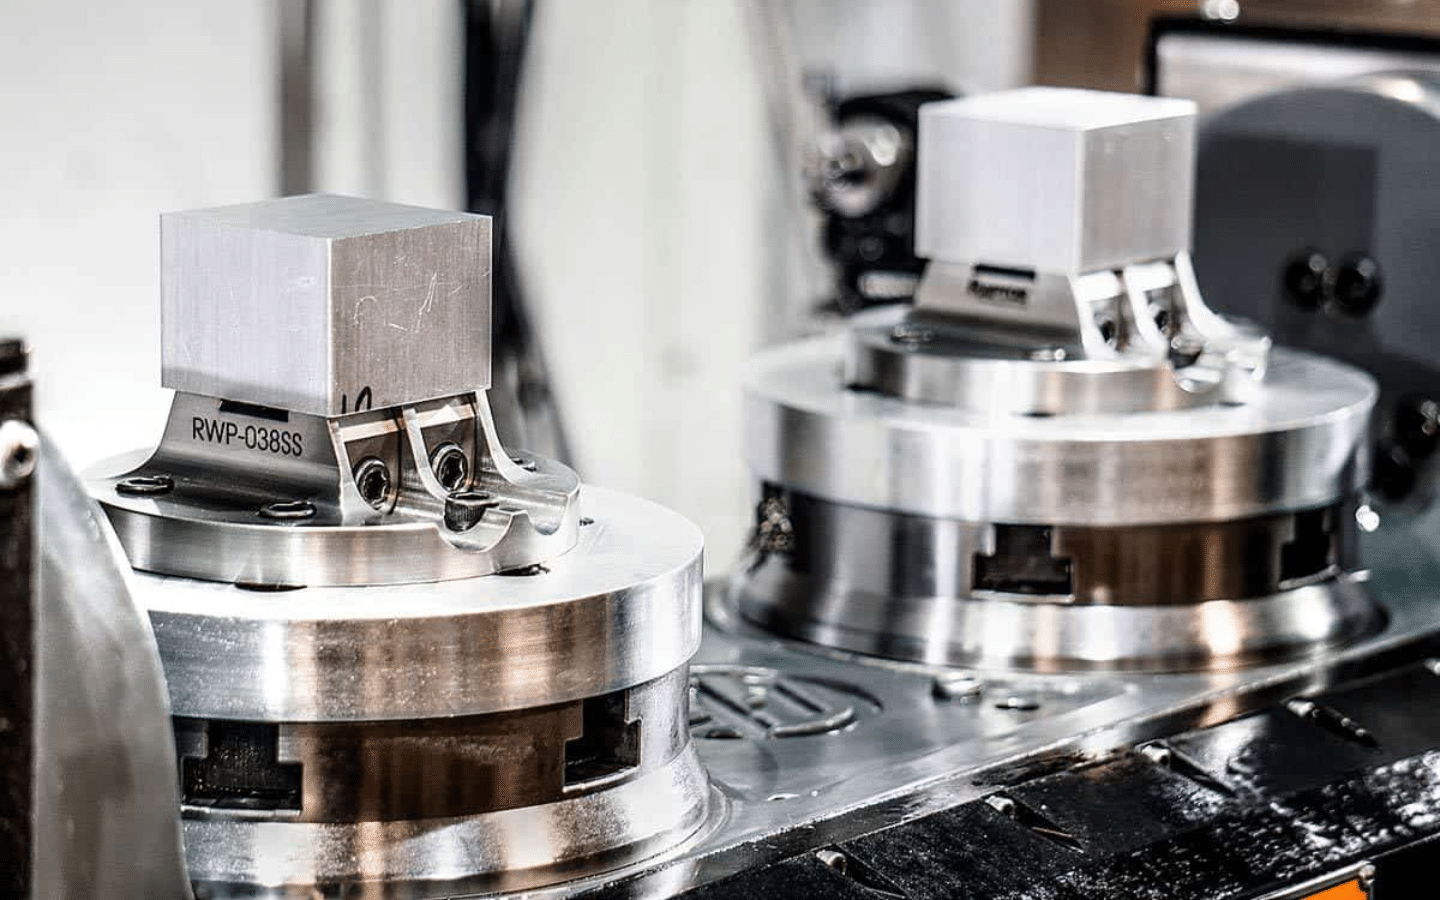 Small-diameter turned components like these are typical Swiss machining output: slender, tight-tolerance parts produced from bar stock.
Once a part's geometry calls for Swiss-type support (small diameter, high length-to-diameter ratio, tight tolerance) the next question is who can hold that tolerance consistently across a production run. DEK machines sub-10 mm precision components down to ±0.003 mm using Swiss-type turning capability, working across the 50+ metals and plastics in its material range, including stainless, titanium, brass, and PEEK. If a project's specs are settled and it's time to price it out, Swiss CNC turning services covers capability details and how to get a quote started.
FAQ
What is Swiss style machining?
Swiss style machining, Swiss-type turning, and Swiss machining all describe the same process: a sliding headstock feeds bar stock through a guide bushing so the cutting tool works right at the support point, reducing deflection on long, slender parts.
What does a Swiss machinist do?
A Swiss machinist sets up guide bushings and bar feeders, programs multi-axis and live-tooling sequences, monitors bar-fed cycles for thermal drift or tool wear, and inspects micro-tolerance parts; the job is mostly precision setup and process control rather than manual cutting.
How much does a Swiss machine cost?
Compact Swiss lathes with smaller bar capacity generally start around $80,000–$120,000; larger multi-spindle machines with bigger bar capacity and more live-tooling stations can run $200,000–$400,000 or more. Actual pricing depends on axis count, bar capacity, and control system; see swiss machining options for how equipment and setup costs translate into per-part pricing.
Do machinists make a lot of money?
Per the U.S. Bureau of Labor Statistics (May 2023 data), the median annual wage for machinists was roughly $48,000. Experienced CNC and Swiss-specific machinists, whose skills include multi-axis programming and micro-tolerance inspection, often earn $55,000–$70,000 or more depending on region, shift, and industry.
WRITTEN BY
Bing manages daily production, covering scheduling, workflow coordination, and shop-floor control. He has strong experience in machining processes, tooling, and practical problem-solving. In his free time, he likes outdoor exploration and adventure trips.
Related Posts
-
 Types of Washers: The Comprehensive Guide
-
 Melting Point of Glass : All You Need to Know
-
 Ceramic Melting Point : All You Need to Know
-
 Black Anodized Aluminum: All You Need to Know Introduction
-
 Liquid Silicone Rubber: Properties, Types, and Process
-
 Deburring Guide: Definition, Types and Methods
-
 Melting Point of PVC: All You Need to Know
-
 Guide To In-Mold Labeling (IML): Everything You Need To Know
-
 Density of Gold: A Detailed Guide

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.