









Complex Parts CNC Machining Services
DEK runs complex parts CNC machining for designs turned down elsewhere, holding ±0.003 mm on micro features. 50+ metals and engineering plastics run under one ISO-certified roof.
-
±0.003mm
Micro Features
-
50+
Metals & Plastics
-
3 Days
Fast Prototypes
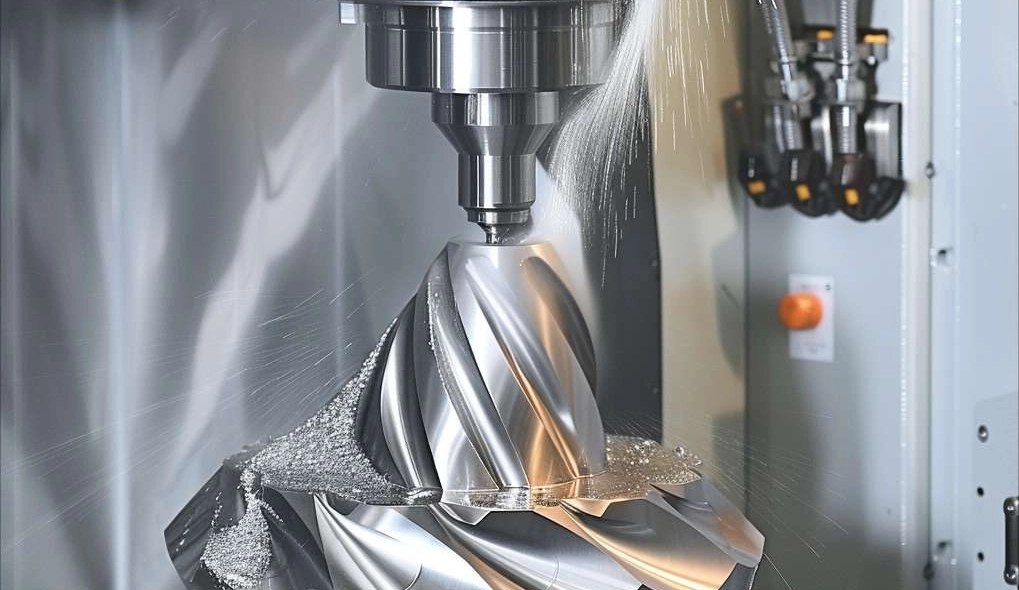

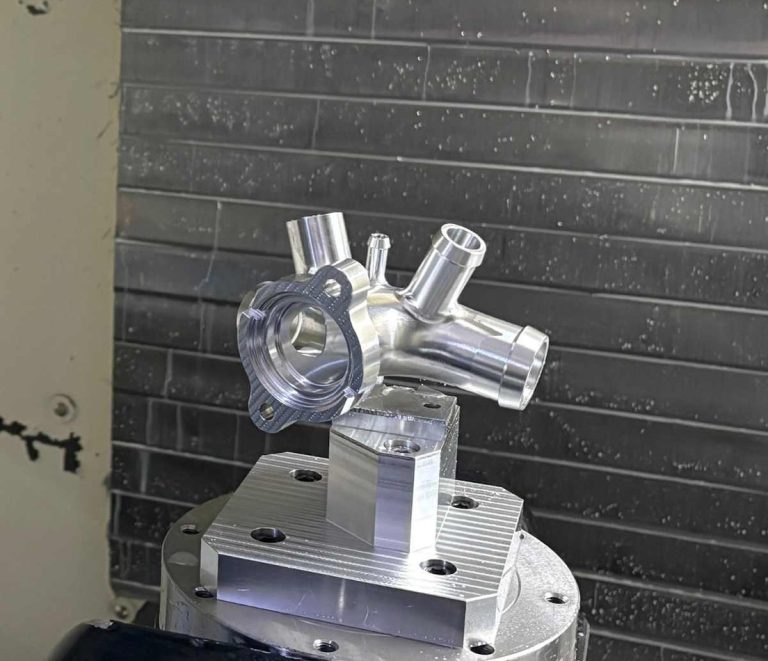
Complex CNC Machining for Parts Others Turn Down
Complex CNC machining covers geometries that push a standard 3-axis setup past its limits: thin walls that chatter, deep cavities beyond tool reach, compound angles, dense features and tight tolerance stacks across mating features.
DEK stacks 5-axis CNC machining, turning, EDM and grinding under one quality system, so a thin-wall housing, deep-cavity manifold or compound-angle bracket moves between operations in-house instead of bouncing between vendors.
Why Engineers Choose DEK
Complex parts fail sourcing when a shop can do four operations and subs out the fifth. Here is what keeps them on track at DEK.
-

Two Decades of Practice
A production floor built on two decades of hands-on precision-machining work, serving a client base of 2,300+ global OEMs sourcing complex work.
-

1.2 Million Parts a Year
More than 1.2 million critical parts leave DEK's shop floor every year, with in-house CMM inspection and full traceability documentation on every job.
-

98.6%+ On-Time Delivery
On-time delivery holds above 98.6% across that volume, with milling, turning, EDM and grinding run in-house under one quality system.
-

No MOQ, 3-Day Prototypes
No MOQ: one-off complex prototypes run alongside production orders, with prototype lead time as fast as 3 days.

Engineer-Reviewed Drawings
Every quote comes from an engineer who has reviewed the drawing, not an automated calculator. Send 2D/3D drawings and call out the tolerances that matter most: you get a review, not a bounce.


Multi-Process Capability Stack
A single machine rarely solves a genuinely complex part. These processes run under one roof so each operation stays in-house.
Complex Parts Machining vs. Single Processes
Choose complex parts CNC machining when a design combines two or more difficulties; see CNC machining cost for how each process drives price.
| Criteria | This ProcessComplex Parts CNC Machining | 3-Axis Machining | EDM Machining | Swiss Machining |
|---|---|---|---|---|
| Best for | Multi-feature, multi-process | Flat faces and pockets | Hardened alloys | Long, slender parts |
| Geometry | Thin walls, cavities, angles | Straightforward contours | Unreachable inner corners | Sub-10 mm diameter |
| Typical tolerance | ±0.003 to ±0.01 mm | ±0.005 mm (general) | Per drawing | ±0.003 mm (micro) |
| Choose when | 2+ difficulties combine | Extra axes add cost only | Milling can’t finish feature | Part deflects on a lathe |
Industries Running Complex Parts
Aerospace (non-flight-critical cabin and structural parts), medical devices, robotics and semiconductor equipment run complex parts through DEK.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
What Makes a Part Complex to Machine
A part usually qualifies when it combines two or more of these features. Together, they narrow the list of shops that can run it.
-

Thin Walls
Walls that flex or chatter under cutting load, typical of thin-wall housings where a free-machining grade helps avoid deflection.
-

Deep Cavities & Pockets
Cavities beyond standard tool reach, reached in one clamping with 5-axis CNC machining or finished by EDM.
-

Compound Angles
Multi-axis angles that need simultaneous tool tilt, as on compound-angle brackets, machined without re-fixturing.
-

High Feature Density
Many holes, bosses or pockets in one body, run in a single program without rework or repeated setups.
-

Tight Tolerance Stacks
Stacked tolerances across mating features, with fit-critical shaft-bore and coaxiality held to ±0.005 mm.
-
Multi-Process Builds
Multi-material or multi-process parts milled, ground and EDM'd in the same body, finished with cylindrical grinding.
Common Challenges We Handle
-
Designs Turned Down
Thin-wall housings, deep-cavity manifolds and multi-material assemblies with stacked tolerances get an engineer review, not a bounce.
-
Hardened Deep Cavities
A deep-cavity part in a hardened alloy may need EDM to finish features milling can't reach; validated on Ti-6Al-4V, Inconel 718 and 17-4PH.
-
The Subcontracted Fifth Step
Complex parts fail sourcing when a shop does four of five operations and subs out the fifth; DEK keeps the full stack under one roof.
-
Bores Ground After Turning
A coaxiality-critical bore ground after turning still has to land inside ±0.005 mm, or the assembly doesn't go together.
Quality Built for Complex Parts
Certified through TUV, with in-house CMM inspection and full traceability on every job.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
50+ Metals and Engineering Plastics
Complexity often drives material choice. Hard-material processes are validated for Ti-6Al-4V, Inconel 718, 17-4PH, 316LVM and PEEK.
Engineering Plastics
Need a grade not listed here? Browse all CNC machining materials
View MaterialsHow to Order Complex Machined Parts
Frequently Asked Questions
Straight answers on cost, tolerances and ordering for complex machined parts.
Request a Complex Parts CNC Machining Quote
Send 2D/3D drawings and call out the tolerances that matter most. Talk with our experts about the part other shops turned down.
- No MOQ, from one-off prototypes
- Prototypes ship in as little as 3 days
- Every quote reviewed by an engineer
- Tolerances as tight as ±0.003 mm
- ISO 9001, AS9100D and ISO 13485







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








