









4140 Steel Machining
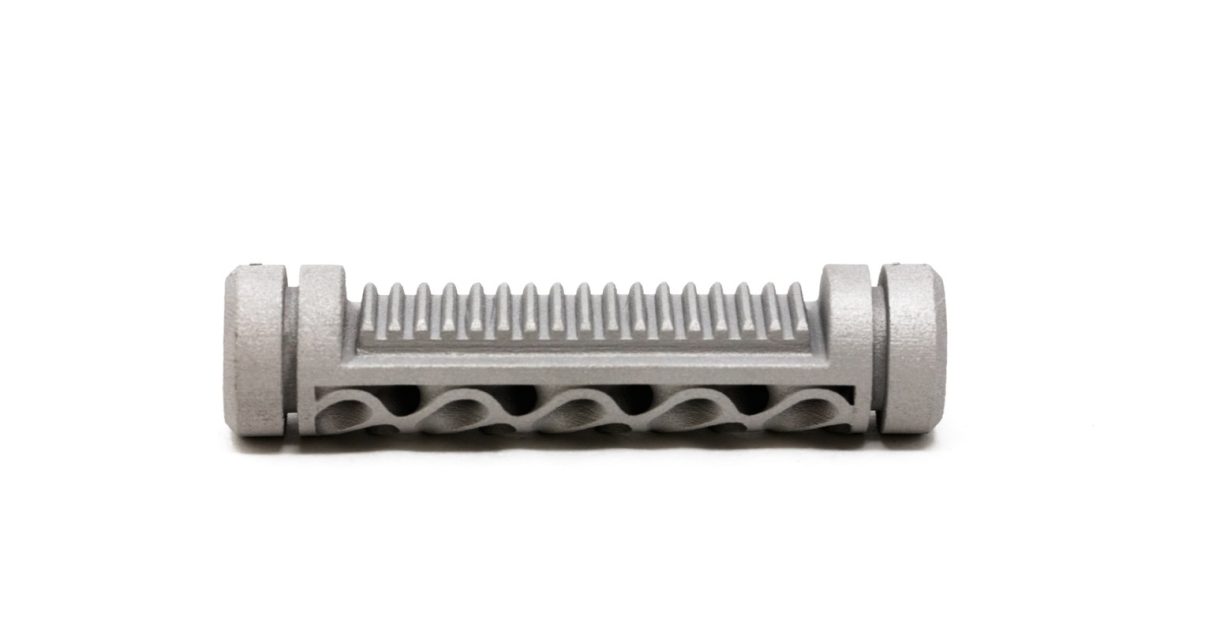
Also known as 42CrMo4 · SCM440 · EN194140 steel machining at DEK covers annealed bar at about 200 HB, 28–32 HRC pre-hard stock and Q&T parts ground at 50+ HRC. We turn, mill, grind and heat treat shafts, gears and tooling to ±0.005 mm on request, with no MOQ and prototypes in 3–5 days.
-
655 MPaTensile, Annealed
-
28–32 HRCPre-hard Hardness
-
830–900 MPaYield, Pre-hard
-
45–55 HRCQ&T High Hardness
4140 Machining Capabilities and Tolerances
Tolerances, finishes and part sizes DEK holds on 4140 shafts, gears and tooling across turning, milling and grinding.
-

Turned & Milled
±0.025 mmstandard
-

Tight Tolerance
±0.005 mmon request
-

Ground Diameters
±0.003 mm0.002 mm roundness
-

Bores and Fits
H7, g6, k6turned or ground
-

As-machined Finish
Ra 0.8–1.6 µmturned and milled
-

Ground Finish
Ra 0.2–0.4 µmhardened shafts, faces
-

Turning Diameter
3–300 mmincl. bar-fed production
-

Gear Quality
Grade 7–8ISO 1328, hobbing
4140 Properties and Equivalent Designations
Property data for 4140 chromoly steel in annealed, pre-hard (Q&T) and high-hardness Q&T conditions, with composition and equivalents.
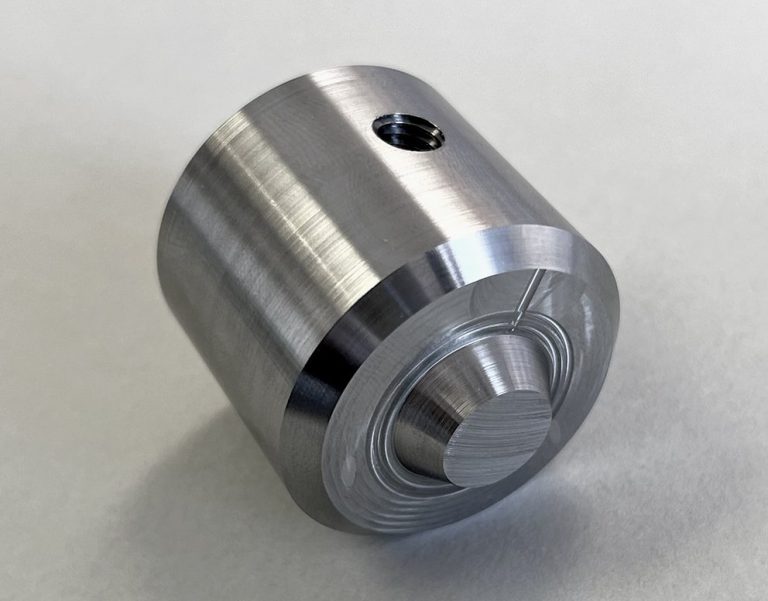

- Hardness, annealed 190–230 HB (~200)
- Hardness, pre-hard 28–32 HRC (269–302 HB)
- Hardness, Q&T high 45–55 HRC
- Tensile, annealed 655 MPa
- Tensile, pre-hard 950–1,050 MPa
- Tensile, Q&T high 1,500–1,900 MPa
- Yield, annealed 415 MPa
- Yield, pre-hard 830–900 MPa

- Yield, Q&T high 1,300–1,600 MPa
- Machinability, annealed ~66% (1212 = 100%)
- Machinability, pre-hard ~55% (1212 = 100%)
- Above 45 HRC Grind, hard turn or EDM

- C 0.38–0.43 %
- Mn 0.75–1.0 %
- Cr 0.8–1.1 %
- Mo 0.15–0.25 %
- Si 0.15–0.35 %

- UNS G41400
- EN 1.7225 (42CrMo4)
- BS EN19, 708M40
- JIS SCM440
- AMS 6382
4140 Machinability in Each Condition
How 4140 alloy steel machining changes from annealed bar to pre-hard stock and hardened parts on the shop floor.
Annealed 4140 alloy steel machining behaves like 1045 with slightly tougher chips: coated carbide at 150–220 m/min turning and straightforward CNC milling.
4140 pre-hard machining at 28–32 HRC is routine but harder work: speeds drop, cutting forces rise, and chips are stiff and hot. The finish is better than annealed because the material does not tear.
- Order annealed when the part is hardened to a specific HRC after machining.
- Pre-hard is the most common 4140 stock DEK runs, for parts going straight into service.
- Above 36 HRC conventional cutting becomes uneconomic.
- At 45–55 HRC we hard turn with CBN, grind, or use wire EDM.
-
Turning Speed, Annealed
150–220 m/minCoated carbide
-
Turning Speed, Pre-hard
100–150 m/minRigid setup, tough carbide
-
Machinability, Annealed
~66%Versus 1212 = 100%
-
Machinability, Pre-hard
~55%Routine but harder work
-
Finish, Pre-hard
BetterMaterial does not tear
-
Hardened Cutting
45–55 HRCCBN, grinding or EDM
Typical 4140 Parts: Shafts, Gears, Tooling
4140 parts DEK machines for industrial machinery, automation, automotive, agriculture and mining customers.
-
 Drive & Motor ShaftsDrive and motor shafts, spindles and splined shafts that need through-hardening and fatigue resistance.
-
 Gears & SprocketsGears, sprockets and pinions hobbed or shaped to ISO 1328 grade 7–8, Q&T for high-load duty.
-
 Jigs & FixturesJigs, fixtures, fixture plates and locating pins, usually machined from 28–32 HRC pre-hard stock.
-
 Tooling & Mold BasesPunch holders, die shoes and mold bases that go straight into service from pre-hard 4140.
-
 Hydraulic Cylinder RodsHydraulic cylinder rods ground to ±0.003 mm, with a nitrided wear surface where the drawing requires it.
-
 Couplings and HubsCouplings and hubs turned from 3 mm to 300 mm diameter, with bores and fits made to H7, g6 or k6.
-
 Oil and Gas Tool BodiesOil and gas tool bodies that need 800–1,000 MPa yield strength and through-hardening in thick sections.
-
 Mining & AgricultureWear and drive parts for agriculture and mining customers, with induction-hardened journals and gear teeth.
4140 vs 4130 and 4340
Choose 4140 for unwelded shafts, gears and tooling; 4130 when welded, 4340 for heavy sections. See alloy steel vs carbon steel.
Heat Treatment, Nitriding, and Finishing
CNC machining + finish for 4140: heat treatment and surface treatments run as part of the job on the parts we machine.
-
Quench and temper AvailableAustenitize at 845–870 °C, oil quench, temper: 45 HRC at 400 °C, 28–32 HRC at 540–600 °C. We leave 0.3–0.5 mm grind stock for distortion.
-
Nitriding AvailableGas or ion nitriding at 500–530 °C gives a 0.2–0.5 mm case at 55–62 HRC with 0.01–0.02 mm growth, done after finish machining.
-
Induction hardening AvailableJournals and gear teeth induction hardened to 50–58 HRC with a soft core, then ground to final size on the machined part.
-
Black oxide AvailableBlack oxide applied to finished 4140 parts as the drawing requires, after machining and any heat treatment are complete.
-
Zinc plating AvailableZinc plating applied to finished 4140 parts as the drawing requires, after machining and any heat treatment are complete.
-
Phosphate or QPQ AvailablePhosphate or QPQ applied to finished 4140 machined parts as the drawing requires, after machining and any heat treatment.
Request a 4140 Steel Machining Quote
Send a STEP, IGES or PDF drawing with condition, surface treatment and tolerances. An engineer confirms the route and grind features and returns pricing within 6 hours.
CNC Machining 4140 Chromoly Steel
4140 is a chromium-molybdenum medium-carbon steel: deep hardenability lets a 100 mm bar harden through, with strength retention to about 400 °C.
DEK brings 20+ years of 4140 steel machining for export customers, whether the drawing says 42CrMo4, SCM440 or EN19. We are ISO 9001:2015, ISO 13485 and AS9100D certified by TÜV, with turning, milling, gear cutting, grinding and EDM in-house.
- Spectrometer check on every incoming lot; hardness testing on every heat-treated batch.
- CMM inspection with IQC, IPQC, FAI and OQC.
- Engineer-reviewed quotes within 6 hours with grind stock and distortion allowance; no MOQ; prototypes in 3–5 days.
Choose 4140 for parts that need 800–1,000 MPa yield strength, through-hardening in 25–100 mm sections, fatigue resistance and a nitridable surface.
Choose something else when the part is welded in production (4130), when corrosion resistance is required (17-4 PH), when sections exceed 100 mm at high hardness (4340), or for a low-load bracket where 1018 or 1045 costs less.
-
 Raw Stock
 CNC Machined
 Finished Parts
-
 Raw Stock
 CNC Machined
 Finished Parts
4140 Machining FAQ
Common questions from engineers ordering 4140 and 42CrMo4 machined parts.
Other Materials
-
 Alloy Steel A514A514 steel is a cost-effective, high-performance material known for its strength, weldability, and toughness, especially in low temperatures.Learn More
-
 Alloy Steel 8620Alloy steel 8620 is a low-alloy steel containing nickel, chromium, and molybdenum with high strength and toughness. It is a commonly used steel that can be carburized.Learn More
-
 Alloy Steel 4340Alloy Steel 4340 belongs to the AISI 4000 series of steels, a heat-treatable, low-alloy steel with high strength and toughness.Learn More

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








