









Mold Core and Cavity Machining
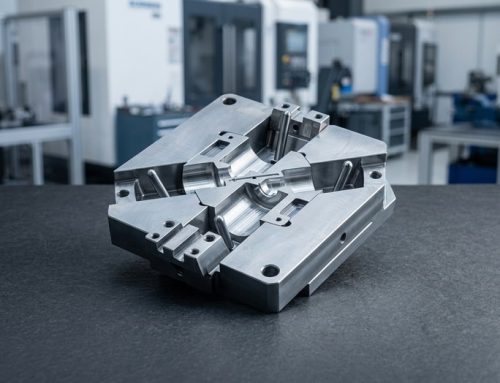
Mold core and cavity machining in H13, S7, D2 and A2, held to ±0.005 mm with polished surfaces to Ra 0.2 µm. No MOQ, prototypes in 3–5 days, every drawing engineer-reviewed.
-
±0.005 mm
Milled & Ground
-
Ra 0.2 µm
Polished Finish
-
3–5 days
Prototype Lead
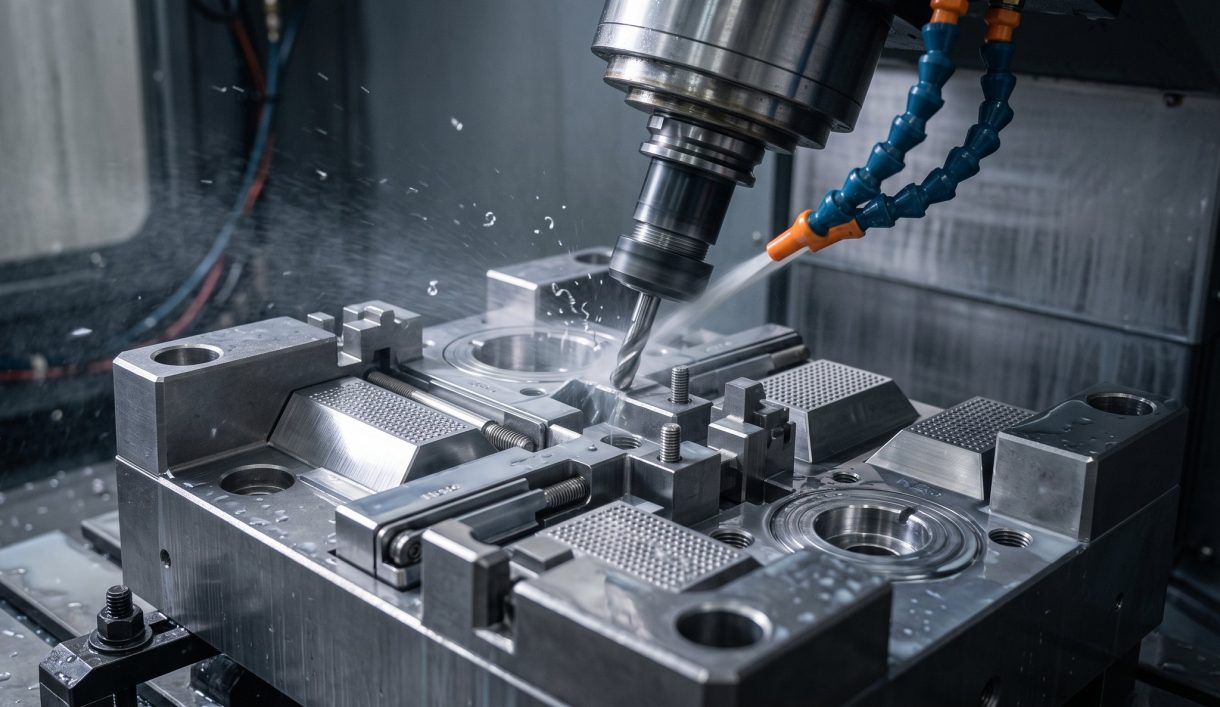

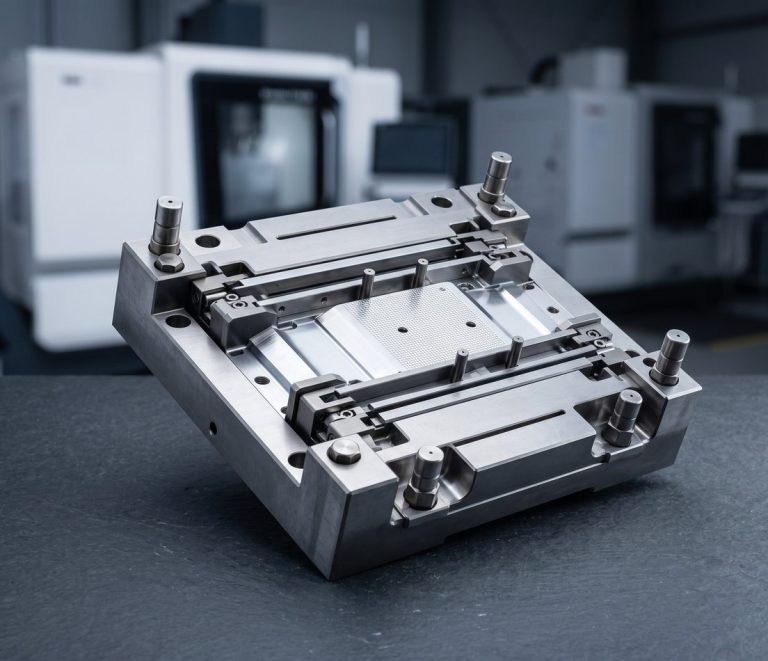
Mold Components Manufacturing Since 2002
Mold core and cavity machining is DEK’s oldest trade: founded in 2002, we supplied core pins, ejector pins and guide bushes to mold makers. Today we machine cores, cavities, inserts, slides, lifters and ejector pins in H13, S7, D2, A2, O1 and 420 stainless.
Mold components are part of our custom CNC machined parts catalogue, machined to your design with wire EDM and grinding. Mold design and injection molding are not covered here.
Types of Mold Components We Machine
Cores, cavities, inserts, pins, electrodes and die details machined from hardened, pre-hardened or annealed tool steel blocks.
-
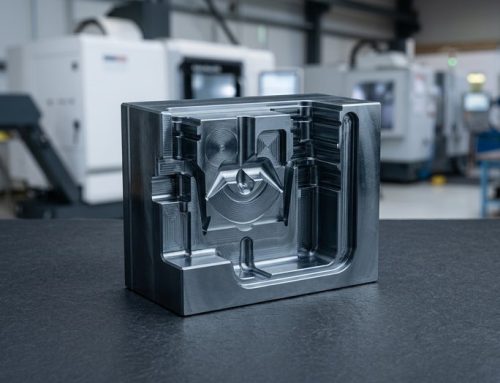 Cores and CavitiesFrom hardened or pre-hard blocks, hard milled after heat treatment.
-
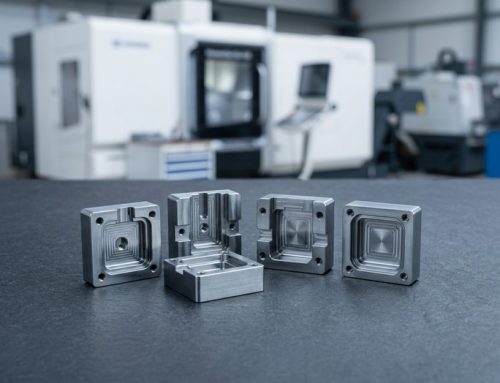 Mold Inserts CNC MachinedCavity, core, gate and vent inserts, CNC milled and wire-cut.
-
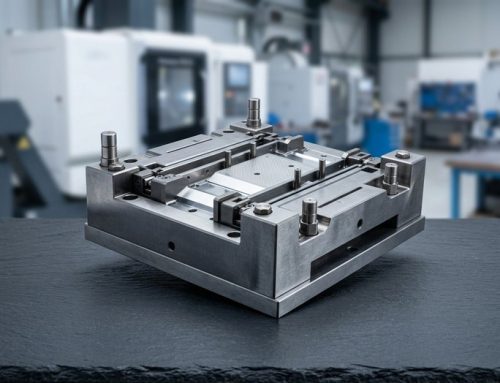 Slides, Lifters and WedgesSlides, lifters, wedges and wear plates with ground angled faces.
-
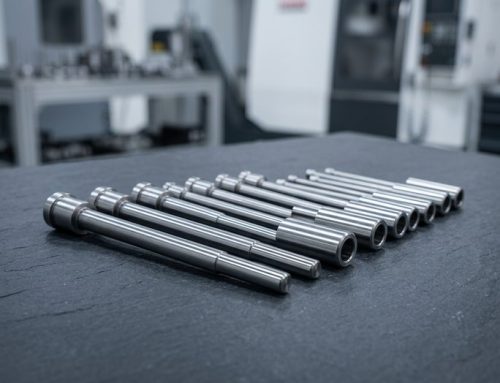 Ejector Pins and SleevesEjector pins, ejector sleeves, core pins and blade ejectors.
-
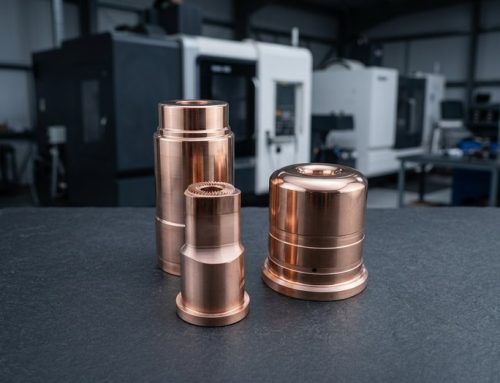 Sinker EDM ElectrodesElectrodes in C110 copper, machined in-house for sinker EDM work.
-
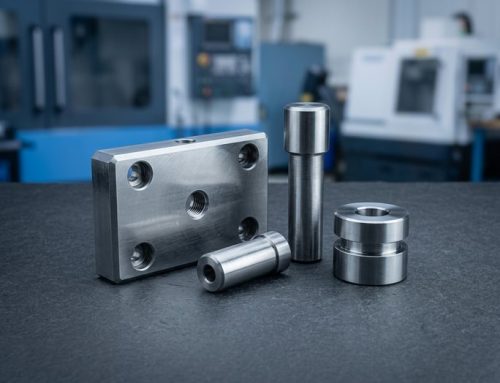 Stamping Die ComponentsPunches, die buttons, stripper plates and form blocks for stamping.
-
 Rapid Tooling InsertsInserts in aluminum or pre-hard steel for rapid tooling programs.


Mold Core and Cavity Machining Specs
Tool steels, EDM and grinding routes, measured tolerances and finishes for cores, cavities, inserts and die details.
Design Tips for Mold Components and Dies
Drawing callouts that decide cost, route and tool life for cores, cavities, inserts and ejector pins.
-

Hardness and Machining Order
State hardness and whether finish machining follows heat treatment; it costs more but removes distortion risk.
-

Internal Corner Radii
Radii under 0.2 mm imply EDM, so say which faces are EDM-acceptable on the drawing.
-

Ejector-Pin Hole Patterns
Dimension holes as a pattern from one datum with an H7 fit and a counterbore length tolerance.
-

Polish Grade and Direction
Call out draft, SPI or VDI 3400 grade and direction on every molding surface; "polish" alone is not a spec.
-

Replaceable Inserts
Design gate and wear-prone core inserts as replaceable pieces to avoid re-machining the whole cavity block.
What to Call Out on Your Drawing
-
STEP Model and Drawing
Send a STEP model with the drawing; every insert is checked on CMM against the model before shipment.
-
Steel Grade and Hardness
Give the grade (H13, S7, D2, A2, O1, 420) and target HRC; hardness is verified after heat treatment.
-
Polish Grade
Name SPI or VDI 3400 per surface: Ra 0.8 µm milled, Ra 0.2–0.4 µm polished, mirror polish on request.
-
Quantity and Lead Time
No MOQ: a single replacement insert or a set of ejector pins is quoted and ships in 3–5 days plus heat treatment.
Mold Machining Services by Industry
Mold machining services and custom tooling manufacturing for mold builders in automotive and consumer products, plus 420 stainless inserts for medical.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Why DEK for Mold Components Manufacturing
Over 20 years supplying mold makers, with inspection habits built for tool components.
-

20+ Years With Mold Makers
Founded in 2002 supplying core pins, ejector pins and guide bushes to mold makers; ISO 9001 passed in 2005.
-

Misumi Vendor Since 2012
A Misumi supply-chain vendor since 2012, so tool component inspection routines are long established.
-

CMM and Hardness Checks
Every insert is checked on CMM against the model, pins are gauged and hardness is verified after heat treatment.
-

One Roof, One Route
Milling, wire and sinker EDM, grinding and polishing run in-house, holding ±0.005 mm on finished features.

Engineer Review on Every Drawing
Every drawing is reviewed by an engineer before quoting. DEK is ISO 9001:2015, ISO 13485 and AS9100D certified by TÜV, and machines mold and die components to your design.
Certified Quality for Tooling
ISO 9001:2015, ISO 13485 and AS9100D certified by TÜV.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Tool Steels and Mold Finishes
Steels, copper and finishes we use for cores, cavities, inserts, electrodes and die details.
Surface Finishes
Need another steel or finish? Ask our engineers
All MaterialsMold Components FAQ
Hardened steel, single inserts and scope: answers for mold builders.
Get a Quote for Tool and Die Services
Send a STEP model and drawing with steel grade, hardness, polish grade and quantity. Every drawing is reviewed by an engineer.
- Simple inserts and pins quoted within 6 hours
- Core and cavity sets quoted within 3 days
- No MOQ, single inserts welcome
- Prototypes ship in 3–5 days
- ±0.005 mm milled, ground, wire-cut







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








