









Custom Couplings Machining & Pulleys
Custom couplings machining with bores held to H7 and pitch-diameter runout at 0.01 mm TIR. No MOQ, prototypes in 3–5 days, every drawing engineer-reviewed.
-
0.01 mm
TIR Runout to Bore
-
3–5 days
Prototype Delivery
-
H7
Standard Bore Fit
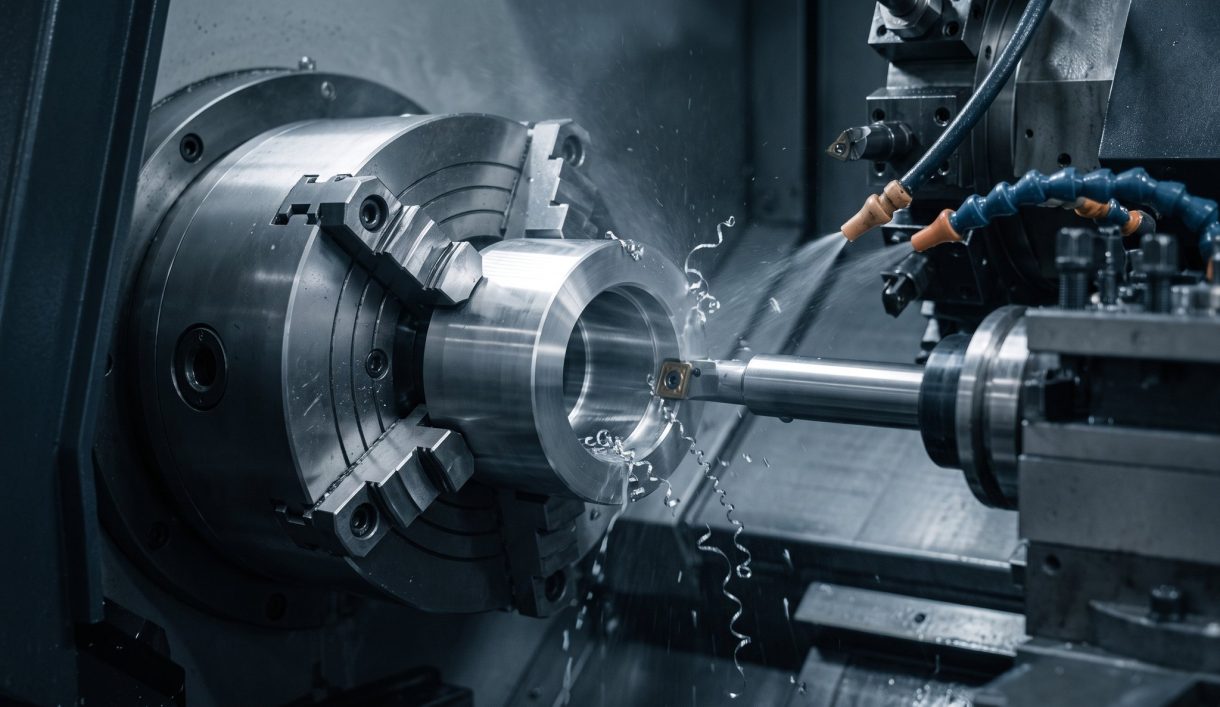

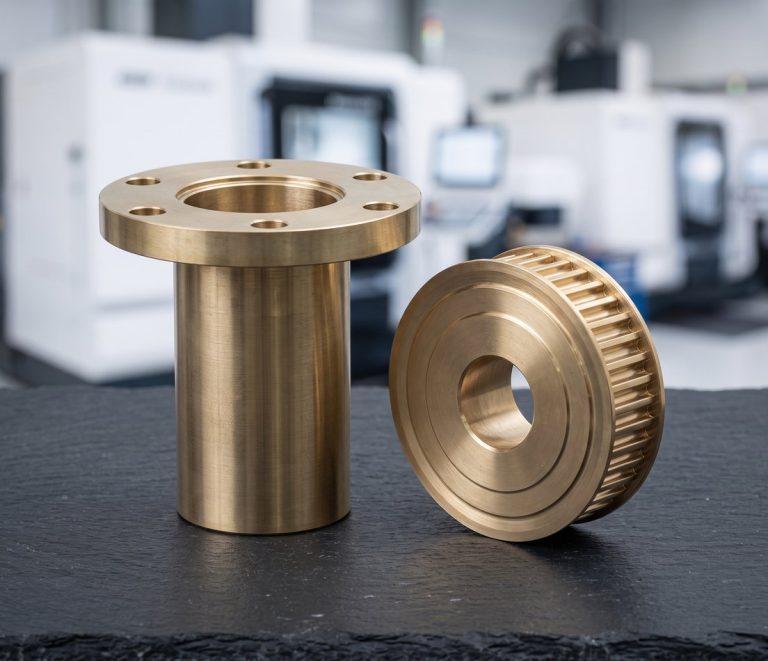
Custom Couplings Machining and Pulleys
DEK machines rigid and clamp shaft couplings, flange couplings, jaw and beam hubs, timing pulleys and V-belt sheaves, turned and milled from 6061 and 7075 aluminum, 1045 and 4140 steel, 303 stainless and Delrin.
Both families depend on bore-to-OD concentricity and bore fit: bores to H7 (H6 on request), critical dimensions to ±0.005 mm. They are catalogued with shafts and gears in our custom CNC machined parts range.
Types of Couplings & Pulleys We Machine
Couplings, coupling hubs, timing pulleys and sheaves, turned and milled from aluminum, steel, stainless and Delrin bar stock.
-
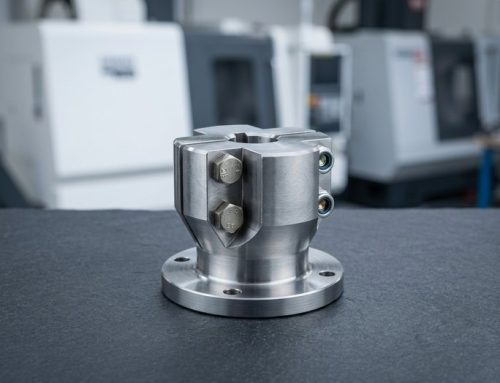 Rigid and Clamp CouplingsSleeve, set-screw and one- or two-piece clamp couplings for any shaft pair.
-
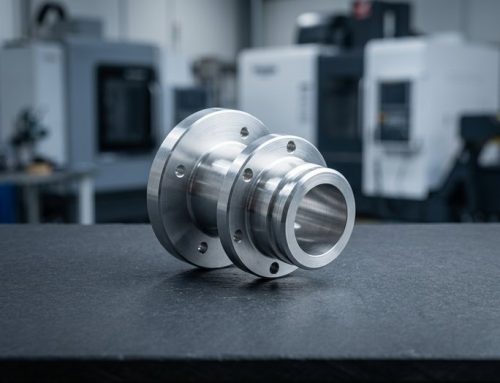 Flange CouplingsFlange couplings and coupling halves with bolt circles and pilot fits.
-
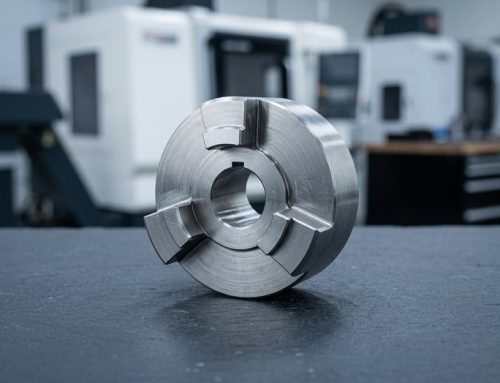 Jaw, Oldham and Disc HubsJaw (spider), Oldham and disc coupling hubs with keyways or clamp hubs.
-
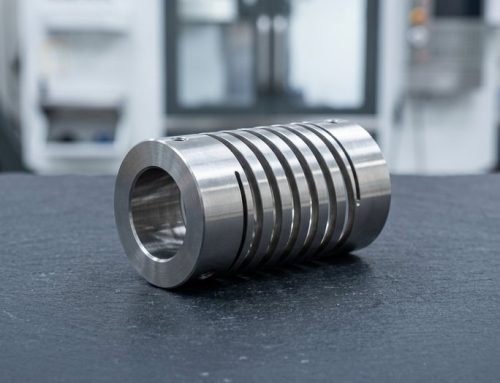 Beam CouplingsHelical or parallel slits cut by wire EDM or slitting saw for flexure.
-
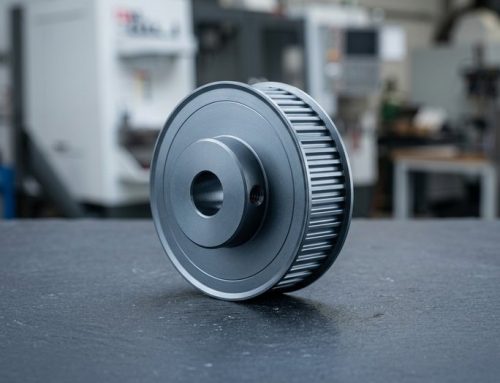 Timing Pulley CNC PartsGT2, GT3, HTD 3M/5M/8M, T5/T10, MXL, XL and L profiles, flanged or not.
-
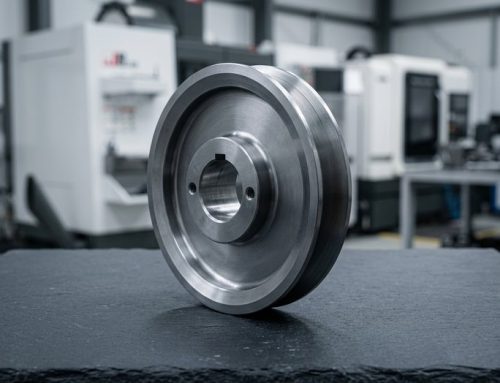 V-Belt Custom SheaveA, B, SPZ, SPA sheaves, flat-belt crowned pulleys and idler pulleys.


Coupling Materials, Processes & Tolerances
Materials, machining routes, tolerances and finishes for couplings and pulleys, all taken from production practice at DEK.
Design Tips for Custom Couplings and Pulleys
Five drawing decisions that set how a coupling grips and how a pulley tracks its belt, before the first chip is cut.
-

Belt Profile and Tooth Count
Specify profile and tooth count, not an approximate pitch diameter: the OD depends on the belt's pitch line differential.
-

Clamp Slit Wall
Keep the clamp screw tangent to the bore and leave at least 1.5 mm of wall at the slit root; thinner walls crack when over-torqued.
-

Flanges on Timing Pulleys
Add a flange on at least one side when shaft axes are not perfectly parallel; belts track off unflanged pulleys.
-

Bore Fit and Torque
H7 with a set screw on a flat suits most drives; use a keyway or clamp hub above roughly 5 N·m or in reversing loads.
-

Groove Angle for a Custom Sheave
State groove angle (34° or 38° by section and diameter) and groove pitch; both change with sheave diameter.
What to Call Out on Your Drawing
-
Bore Fit and Keyway
State H7 or H6, plus keyway (DIN 6885 / ANSI B17.1, P9 or JS9) or set screw position, so the bore is turned to your shaft.
-
Belt or Groove Section
Give GT2, HTD, T5 or MXL profile with tooth count, or A, B, SPZ or SPA groove section, so teeth are hobbed to ISO 5294.
-
Material and Hardness
Name the alloy and any hardness: 4140 at 28–32 HRC, or induction-hardened groove faces at 50–55 HRC on request.
-
Quantity and Lead Time
Add the quantity: there is no MOQ, and single sheaves or prototypes ship in 3–5 days after engineer review.
Applications & Industries
Belt-driven axes for robotics, conveyor and indexing drives for automation, motor couplings for new energy pumps and fans, gimbal drives for drones.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Why DEK for Shaft Coupling Machining
Hobbed teeth, one roof for every process and measured runout: why buyers send couplings and pulleys to DEK.
-

Hobbed, Not Milled Teeth
Timing pulley teeth are cut with hobs, not a profile end mill, because a milled approximation of a GT2 tooth wears belts.
-

One Roof, Four Processes
Turning, hobbing, milling and wire EDM run in-house, so a matched pulley pair and its clamp couplings ship as a set.
-

Runout Measured at FAI
Bores are gauged and runout measured at first article inspection, against a 0.01 mm TIR pitch-diameter target.
-

No MOQ, Fast Prototypes
No minimum order quantity; prototypes and single sheaves ship in 3–5 days, from one part to production runs.

Engineer Review on Every Drawing
Every coupling and pulley drawing is reviewed by an engineer before quoting, checking bore fit, belt profile and groove section, and quotes return within 6 hours.
Certified Quality on Every Drive Part
ISO 9001:2015, ISO 13485 and AS9100D certified, with bores gauged at FAI.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Materials and Finishes for Couplings
Pick the alloy and finish for your coupling or pulley: low inertia, torque, washdown or quiet running.
Surface Finishes
Need another alloy or finish? Ask our engineers.
All MaterialsCouplings and Pulleys FAQ
Answers on bores, tooth counts, coupling types and small sheave runs.
Get a Quote for Custom Couplings Machining
Send a drawing with bore fit, belt profile and tooth count or groove section, material and quantity. Engineer-reviewed quotes return within 6 hours.
- No MOQ, from a single sheave
- Prototypes ship in 3–5 days
- Bores H7 standard, H6 on request
- Runout 0.01 mm TIR, measured at FAI







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








