









Precision Impeller Machining
Impeller machining from solid on 5-axis centers, with blade profiles held to ±0.05 mm and hub bores to H7. No MOQ, and prototypes ship in 3–5 days.
-
±0.05 mm
Blade Profile
-
3–5 days
Prototype Lead
-
20–600 mm
Impeller Diameter
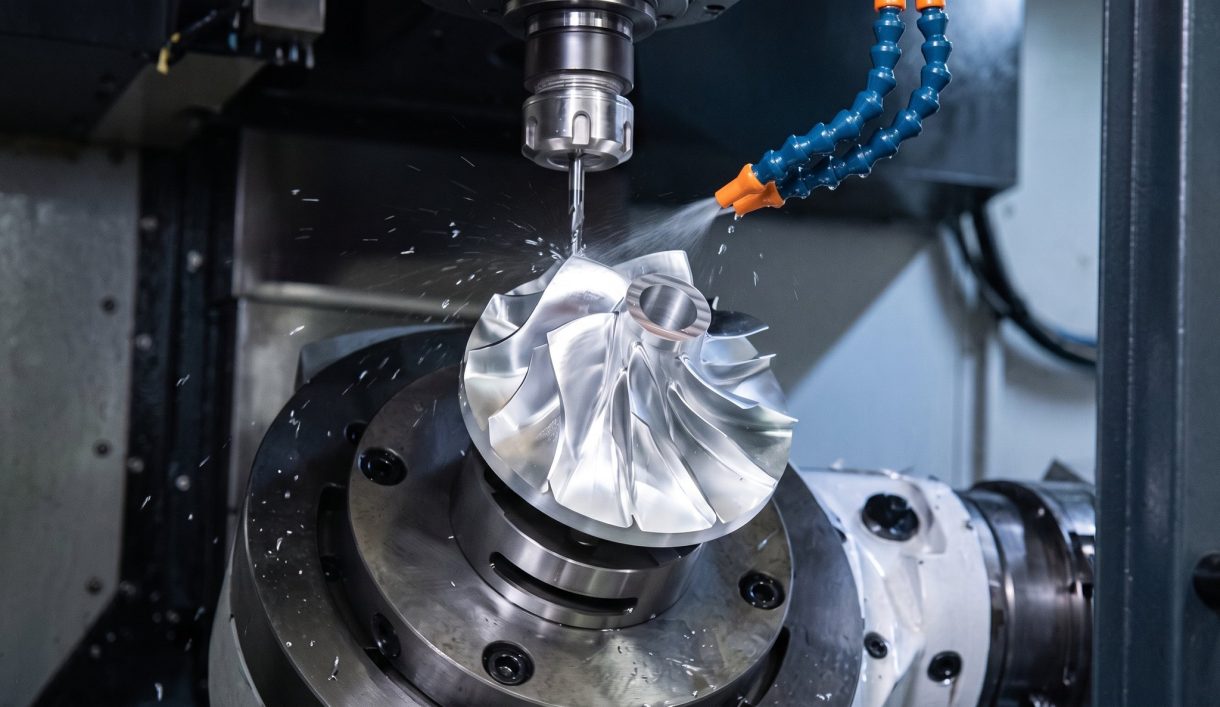

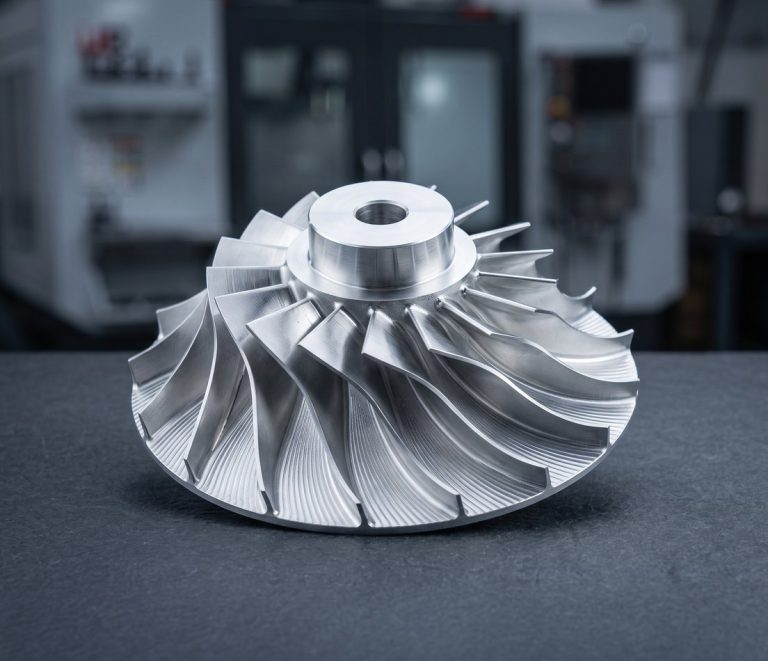
Custom Impellers and Pump Parts Machining
DEK machines open, semi-open and closed impellers, inducers and compressor wheels from solid on 5-axis machining centers, plus the volutes, wear rings, sleeves and shafts around them. Critical dimensions are held to ±0.005 mm.
Machining from bar or plate removes the porosity, blade-thickness scatter and lead time of a casting, so prototype and low-volume pump programs are machined first. These parts sit in our custom CNC machined parts catalogue; for basic forms see 6 types of impellers.
Impeller & Pump Part Types We Machine
Impellers, inducers and the pump parts around them, machined complete from solid bar or plate blanks in stainless, bronze and titanium.
-
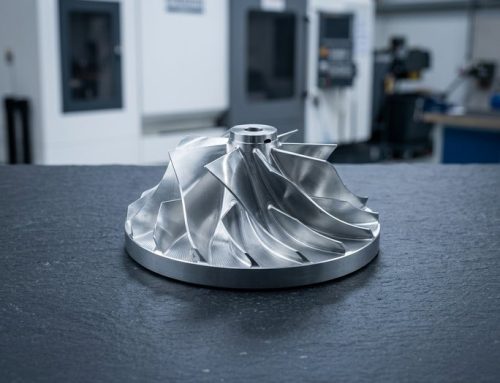 Open & Semi-Open ImpellersRadial impellers with 3 to 12 blades, machined complete from one blank.
-
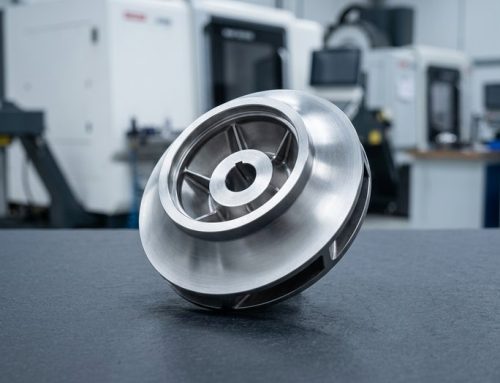 Closed Shrouded ImpellersCut in one piece where passages allow, or as a two-piece hub and shroud.
-
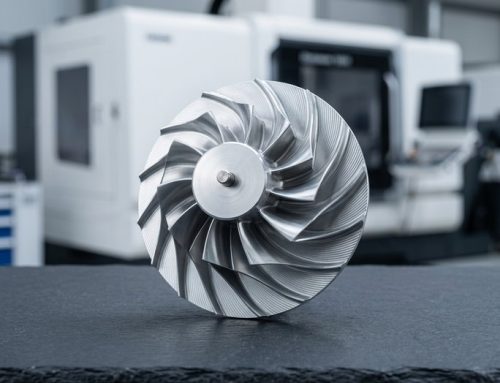 Mixed-Flow & Axial ImpellersMixed-flow and axial impellers, inducers, compressor and turbo wheels.
-
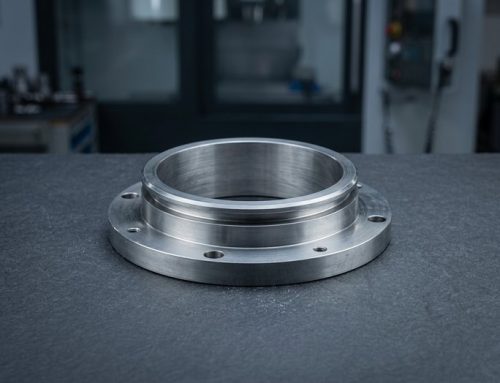 Pump Housing MachiningVolutes, casings and covers with bearing bores and seal faces.
-
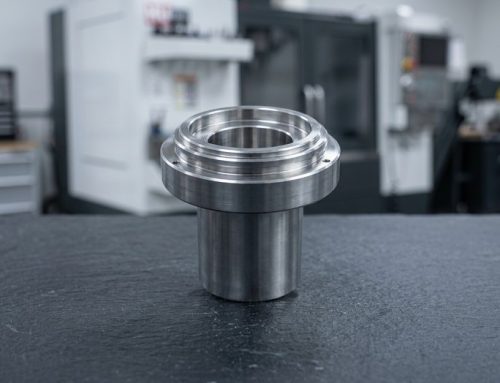 Wear Rings & Shaft SleevesWear rings, throat bushings and shaft sleeves, bronze or hardened stainless.
-
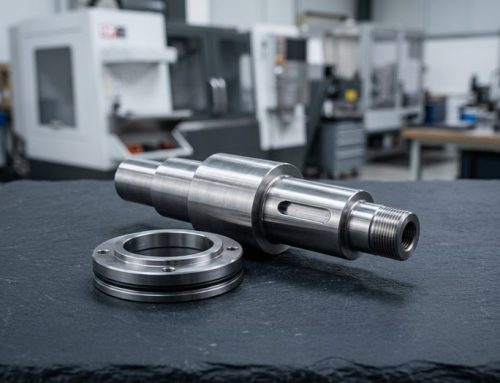 Pump Shafts & Seal HousingsPump shafts, seal housings and mechanical-seal adapters.


Materials, Processes & Specs for Impellers
From material choice to blade profile and balancing, here is how we build impellers and pump parts to your CAD model.
Design Tips for Custom Impellers & Pump Parts
A few drawing choices decide whether an impeller can be cut in one piece and how fast it balances.
-

Send Solids, Not Meshes
Send a native or STEP solid with blade surfaces; five-axis toolpaths come from surfaces and a mesh adds facet error.
-

Wide Enough Blade Passages
Allow a cutter of at least 1/8 of the passage height; narrower passages force a two-piece shroud or EDM.
-

Define Blade Edges
Specify leading-edge radius and trailing-edge thickness; both control cavitation and are easy to leave ambiguous in CAD.
-

Plan the Finishing Hold
Add a dimensioned back-face relief and hub chamfer so the impeller can be held on the bore for the finishing turn.
-

Call Out Balancing
State grade, plane and speed; an unbalanced 316 impeller at 3,000 rpm shortens bearing life quickly. See impeller design.
What to Call Out on Your RFQ
-
Blade Profile Tolerance
State the profile tolerance to the CAD surface; ±0.05 mm is typical, and blade finishing time depends on it, not on material volume.
-
Bore Fit and Keyway
Give the hub bore fit (H7 standard, H6 on request) and keyway to DIN 6885 so runout to the bore stays at 0.02 mm TIR.
-
Material and Balance Grade
Name the alloy and balance grade (ISO 21940 G6.3 or G2.5) with quantity; there is no MOQ for prototypes or production.
-
Matched Pump Set
Include housings and wear rings in the RFQ: pump housing machining alongside the impeller matches bores, seal faces and clearances as a set.
Applications & Industries
Pump parts machining for oil and gas transfer pumps, marine seawater and bilge pumps, new energy coolant pumps, and medical sanitary pumps.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Why DEK for 5 Axis Impeller Machining
Impellers punish shops that quote from a cutting-time calculator. Here is how DEK handles them.
-

Quoted by an Engineer
An engineer programs and quotes every impeller by hand, because blade finishing time depends on surface tolerance and cutter reach.
-

CMM Blade Verification
Blade profiles are verified against the CAD model on CMM to the ±0.05 mm profile tolerance, and parts are photographed before shipment.
-

All In-House
5-axis milling, turning, boring and polishing are all in-house, so the impeller and its pump parts stay under one roof.
-

Certified Quality
Impellers and pump parts are made under ISO 9001:2015, ISO 13485 and AS9100D certified quality systems.

Route Review at Quote
For closed impellers, an engineer checks blade passage geometry at quote and recommends a one-piece cut or a two-piece hub and shroud for welding or press assembly.
Certified Impeller Quality
Impellers are made under ISO 9001:2015, ISO 13485 and AS9100D quality systems.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Impeller Materials and Finishes
Stainless, bronze, titanium and aluminum, each paired with the finish applied after machining.
Surface Finishes
Not seeing your alloy? Ask our engineers for a route.
All MaterialsImpeller Machining FAQ
Common questions on closed impellers, tolerances and pump housings.
Get a Quote for Impeller Machining
Send a STEP model with blade profile tolerance, bore fit, material, balance grade and quantity. An engineer reviews every impeller.
- Complex impellers quoted within 3 days
- Simpler pump parts quoted within 6 hours
- No MOQ; prototypes ship in 3–5 days
- Blade profile held to ±0.05 mm







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








