









Custom Bushings Manufacturing
Custom bushings manufacturing with ±0.005 mm on bore and OD and 0.005 mm concentricity. No MOQ, engineer-reviewed quotes within 6 hours, prototypes in 3–5 days.
-
±0.005 mm
Bore and OD
-
Ra 0.2 µm
Ground Bore Finish
-
3–5 days
Prototypes Ship
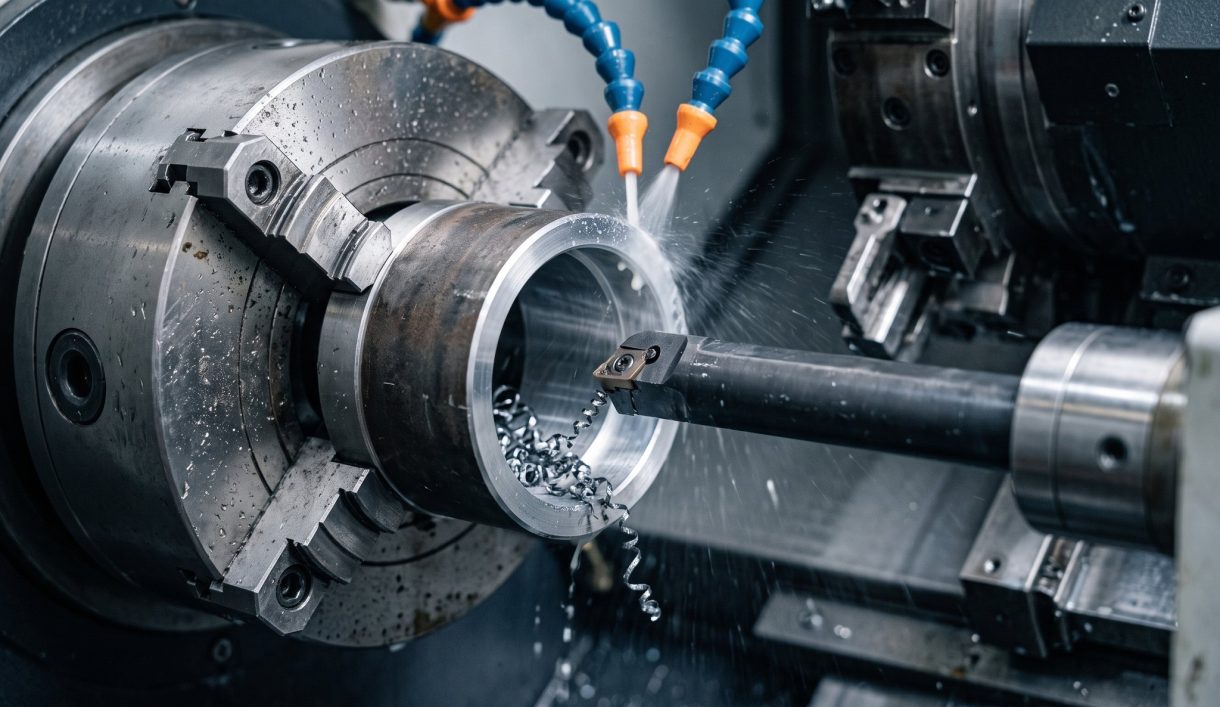

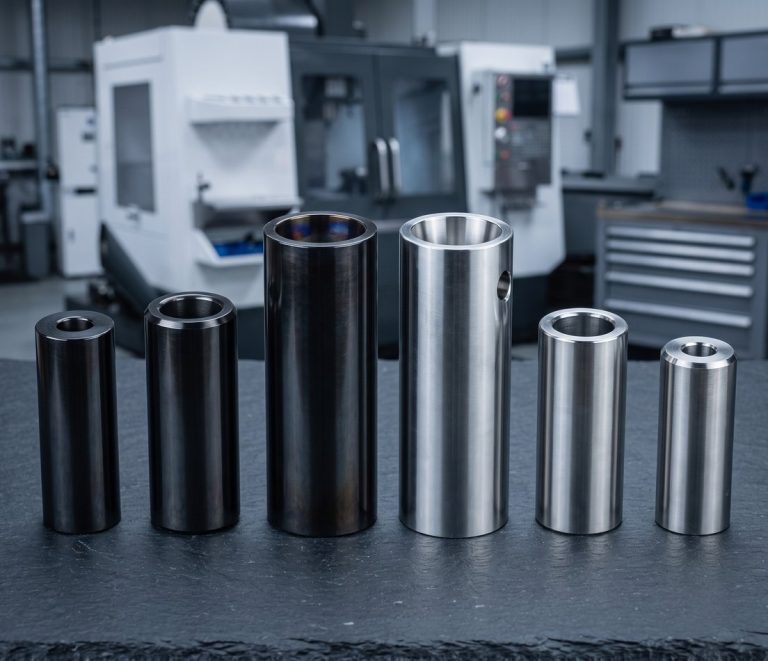
Custom Machined Bushings and Sleeves
DEK turns plain sleeve bushings, flanged bushings, guide bushes, reducer sleeves and wear sleeves from bronze, brass, steel, stainless and engineering plastics. Bore size and concentricity decide whether a shaft runs smoothly or seizes.
We hold ±0.005 mm on bore and OD, with ground bores at Ra 0.2–0.4 µm where the print asks for it. Bushings sit alongside shafts and pins in our custom CNC machined parts catalogue.
Types of Bushings We Machine
From plain sleeves to self-lubricating bushings, turned from bronze, brass, steel, stainless and plastic bar to your print.
-
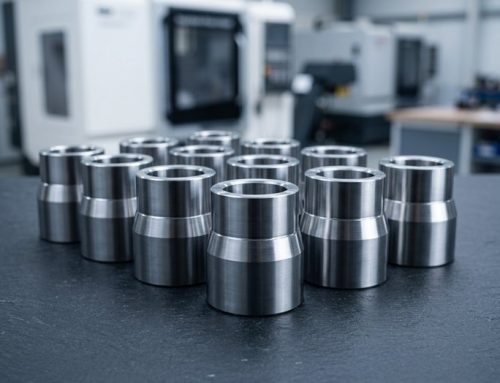 Plain Sleeve BushingsPlain bearing sleeves for rotating or sliding shafts.
-
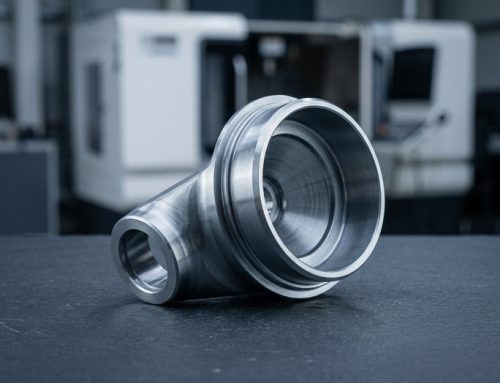 Flanged Bushing CNC PartsFlange carries axial thrust and locates the bushing in the housing.
-
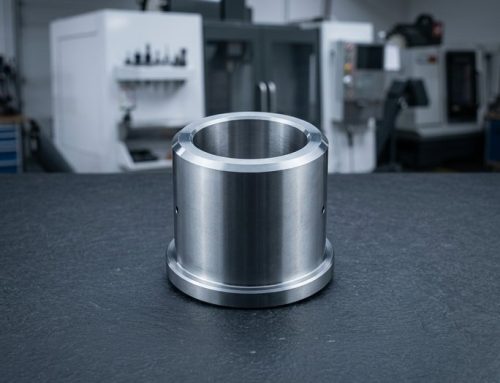 Guide & Leader-Pin BushingsFor molds, dies and fixtures; hardened and ground.
-
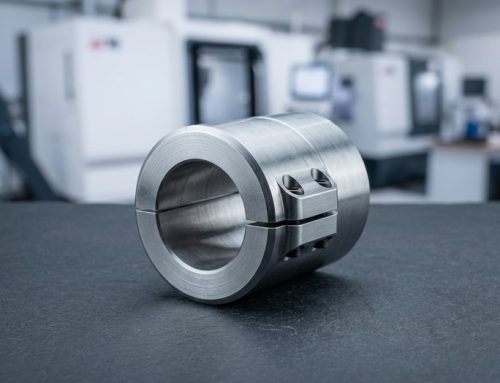 Split & Clamp BushingsSplit and clamp designs that install without a press.
-
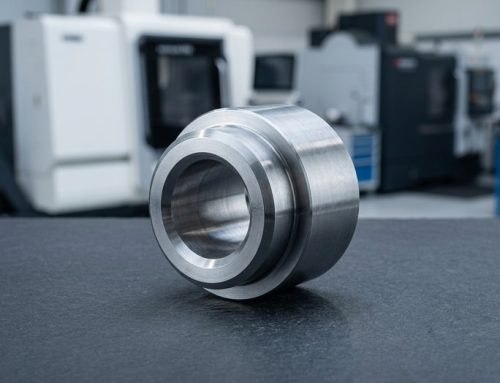 Reducer & Adapter SleevesSleeves that fit a small shaft into a large bore.
-
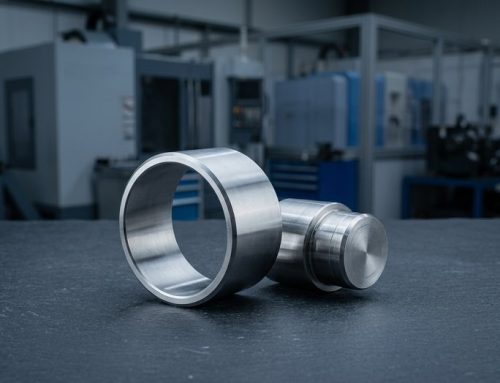 Wear & Repair SleevesShaft wear and repair sleeves in hardened steel or stainless.
-
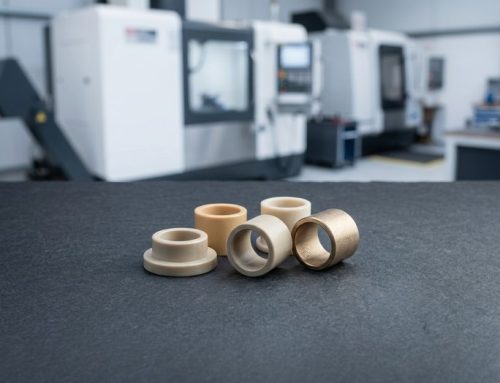 Plastic & Self-Lube BushingsDelrin, PTFE or PEEK insulators; sintered bronze self-lubricating.


Bushing Materials, Processes & Tolerances
Bearing bronzes to hardened steel and PTFE, turned in one chucking and ground when the fit calls for H6.
Design Tips for Custom Bushings
Fits, walls and chamfers decide whether a bushing installs cleanly and stays round in service.
-

Press-Fit by Tolerance Class
Call interference by class (Ø20 s6). In bronze the bore closes by roughly 70–90% of the interference.
-

Wall Thickness in Bronze
Keep wall thickness at 8–12% of shaft diameter in bronze so the bushing stays round when pressed.
-

Lead-In Chamfers
Add a 0.5 × 45° lead-in chamfer on both bore and OD to avoid shaving the housing on installation.
-

Flange Runout to Bore
On flanged bushings, tolerance flange runout to the bore (0.02 mm is practical), not only flange thickness.
-

Oil Groove Ends
Stop oil grooves 1–2 mm short of both ends to keep lubricant inside the bushing during service.
-
Plastic Running Clearance
Give plastic bushings 0.5–1% more running clearance than metal for thermal expansion and moisture uptake.
What to Call Out on Your Drawing
-
Bore and OD Class
State bore and OD tolerance class, for example H7 or H6 bore and p6, s6 or h6 OD, so the fit is unambiguous.
-
Fit Before or After
Say whether the bore fit applies before or after installation; if the installed bore matters, dimension it that way.
-
Material and Hardness
Name the grade and hardness: 4140 at 28–32 HRC, 440C at 56–58 HRC or case-hardened 8620 at 58–62 HRC.
-
Order Quantity Needed
Give the quantity: a single replacement bushing or a 10,000-piece run gets the same engineer-reviewed quote.
Applications & Industries
Bushing machining for agriculture and construction pivots, automation guide bushes, marine rudder and davit bushings, and medical dry-running bushings.
-

Aerospace
-

Medical
-

Automotive
-

Robotics
-

Semiconductor
-

Electronic
-

Telecom
-

Drone & UAV
-

Energy
-

Oil & Gas
-

Marine
-

Industrial Equipment
-

Construction
-

Agriculture
-

Consumer Products
-

Military & Defense
-

Mining
-
 AerospaceNon-flight-critical brackets, cabin hardware and fittings under AS9100D, in 7075 aluminum, Ti-6Al-4V and Inconel 718, with FAI.Learn More
-
 MedicalInstrument shafts, handles and cannulas in 316L stainless, titanium and PEEK under ISO 13485, with lot traceability as standard.Learn More
-
 AutomotivePrototype and low-to-mid-volume sensor housings, valve bodies and shafts in aluminum, 4140 and 4340 alloy steel, stainless and brass.Learn More
-
 RoboticsJoint housings, harmonic drive flanges and gripper fingers in aluminum and hardened steel, with 5-axis milling in one setup.Learn More
-
 SemiconductorChamber components, wafer handling fixtures and vacuum flanges in 6061 aluminum, 316L, PEEK and Kovar, with burr-free edges.Learn More
-
 ElectronicConnector bodies, heat sinks, RF shields and precision pins in aluminum, brass and copper, held to ±0.01 mm on contact features.Learn More
-
 TelecomWaveguide components, filter housings and RF enclosures in aluminum and copper alloys, with silver or nickel plating for conductivity.Learn More
-
 Drone & UAVMotor mounts, gimbal frames and landing gear fittings in 7075 aluminum, titanium and magnesium to cut weight without losing stiffness.Learn More
-
 EnergyBattery end plates, busbars, inverter housings and fuel-cell fittings in aluminum, copper and stainless, machined flat and burr-free.Learn More
-
 Oil & GasValve components, manifold blocks, downhole tool parts and flanges in 4140, 17-4 PH, duplex 2205 and Inconel, with hardness specs.Learn More
-
 MarinePropeller shafts, pump parts and deck hardware in 316 stainless, bronze and aluminum bronze, chosen first for corrosion resistance.Learn More
-
 Industrial EquipmentGripper plates, linear guide mounts, cam followers and machine frames in aluminum and steel, with fixtures kept on file for repeats.Learn More
-
 ConstructionStructural brackets, anchoring hardware and hydraulic fittings in mild steel, alloy steel and aluminum, zinc plated or powder coated.Learn More
-
 AgricultureGearbox housings, shafts, sprayer nozzle bodies and sensor mounts in cast iron, steel and stainless for abrasion and moisture.Learn More
-
 Consumer ProductsKnobs, handles, enclosure parts and audio hardware where the machined surface shows, anodized, bead blasted or polished to sample.Learn More
-
 Military & DefenseOptical mounts, enclosures and accessory rails in aluminum, steel and titanium, with material certification and FAI reports.Learn More
-
 MiningWear plates, bushings, crusher components and hydraulic fittings in hardened alloy steel, bronze and stainless for dust and vibration.Learn More
Why DEK for Custom Bushings Manufacturing
Ground-bore discipline since 2002, verified materials and documented inspection on every bushing order.
-

Making Bushes Since 2002
Guide bushes for mold makers were among the first parts DEK made in 2002; the same ground-bore discipline applies today.
-

Spectrometer-Checked Stock
Incoming bronze and steel are spectrometer checked before machining, so the grade on the print is the grade you receive.
-

Plug Gauge and CMM
Bores are verified with plug gauges and CMM, and inspection reports are available before shipment.
-

No MOQ, 6-Hour Quotes
One bushing or 10,000 pieces get an engineer-reviewed quote within 6 hours; prototypes ship in 3–5 days.

Certified Quality by TÜV
DEK is ISO 9001:2015, ISO 13485 and AS9100D certified by TÜV. Every bushing is held to ±0.005 mm on bore and OD with 0.005 mm concentricity, documented in reports you can review before shipment.
Certified Quality for Every Bushing
Bushings are made under ISO 9001:2015, ISO 13485 and AS9100D, certified by TÜV.
-
 AS9100D
Aerospace Quality Management System
-
 ISO 9001:2015
Quality Management Standard
-
 ISO 13485
Medical Devices Quality Management
Bushing Materials and Finishes
Bearing bronzes, steels and low-friction plastics, combined with the finish each bushing needs after machining.
Surface Finishes
Engineering Plastics
Not sure which bushing material fits? Ask our engineers.
View AllFrequently Asked Questions
Answers on custom sizes, sleeves versus bushings and small flanged bushing orders.
Get a Quote for Custom Machined Bushings
Send your drawing and get an engineer-reviewed quote within 6 hours, for one replacement bushing or a 10,000-piece run.
- Bore and OD tolerance class
- Material and hardness
- Quantity, no MOQ
- Bore fit before or after installation
- Prototypes ship in 3–5 days







Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








