









Acrylic CNC Machining
DEK's acrylic CNC machining turns cast and extruded PMMA into optically clear parts with ±0.01 mm on critical features and prototypes in 3–5 days. Sharp tooling, air-blast cooling and a polishing route restore full transparency.
-
±0.01 mm
Critical Features
-
3–5 days
Prototype Lead Time
-
92%
Light Transmission

Why Acrylic Machining Needs a Careful Shop
Acrylic punishes shops that cut it like aluminum: it crazes, chips and clouds under heat, clamping pressure or the wrong coolant. PMMA is one of the materials covered by our plastic CNC machining services, run on the same 3-, 4- and 5-axis mills as your metal parts.
Because acrylic parts usually mount into metal housings, we machine the aluminum or stainless companion parts in the same order and check the fit before both ship. Browse the full range under CNC machining plastics.
-

ISO 9001:2015, ISO 13485 and AS9100D
-

Engineer-reviewed pricing within 6 hours
-

No MOQ, from 1 to 10,000+ pieces
-

IQC, IPQC, FAI and OQC on CMM
Acrylic Grades We Machine
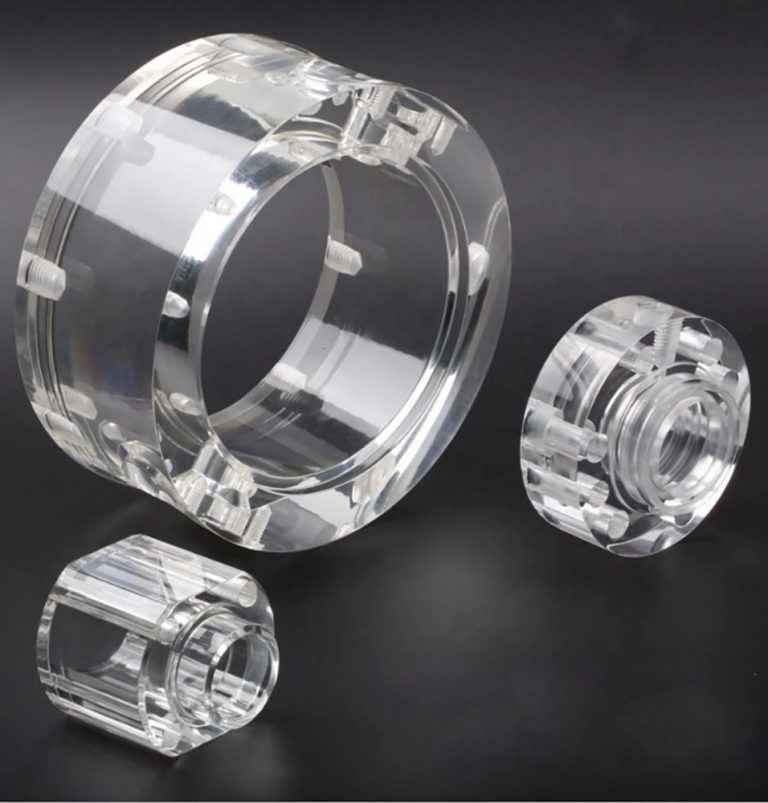
Cast PMMA: 1.19 g/cm³, 65–75 MPa tensile strength, 80 °C max service. Specify cast if the part is polished, bonded or over 12 mm thick.
-

Cast acrylic (PMMA-C)
92% light transmissionHigher molecular weight, lower internal stress. The default for optical parts, thick blocks and anything that will be polished or bonded.
-

Extruded acrylic
Lower cost, tighter thicknessPMMA-E is softer, gummier at the cutter and more prone to crazing. Good for flat covers and simple cut-outs at stock thickness.
-

Impact-modified acrylic
Added toughnessFor guards and handled components that take knocks, at a small cost in clarity compared with standard cast sheet.
-

UV-filtering grades
UV-transmitting or filteringUV-transmitting and UV-filtering grades for instrument windows and photo-curing fixtures that must control the light passing through.
-

Mirrored sheet
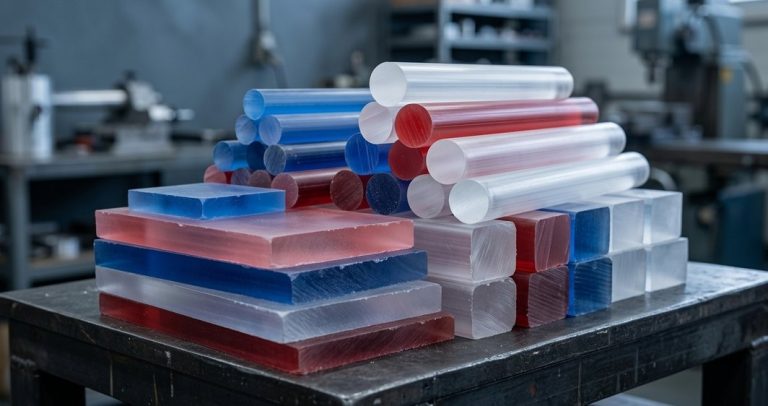
Colored, frosted, mirroredColored, frosted and mirrored sheet for display and signage parts where appearance matters more than optical clarity.
-

Cast PMMA (typical)
~70 × 10⁻⁶/K expansionThree times aluminum's expansion, 0.3% water absorption in 24 h and 80 °C service (extruded grades about 70 °C). Plan clearances accordingly.
-
±0.01 mm
Small rigid features
-
±0.05 mm
Thin or large sheet parts
-
Ra 0.2 µm
Polished acrylic faces
-
Ra 0.8–1.6
As-machined finish (µm)
Acrylic CNC Machining Processes
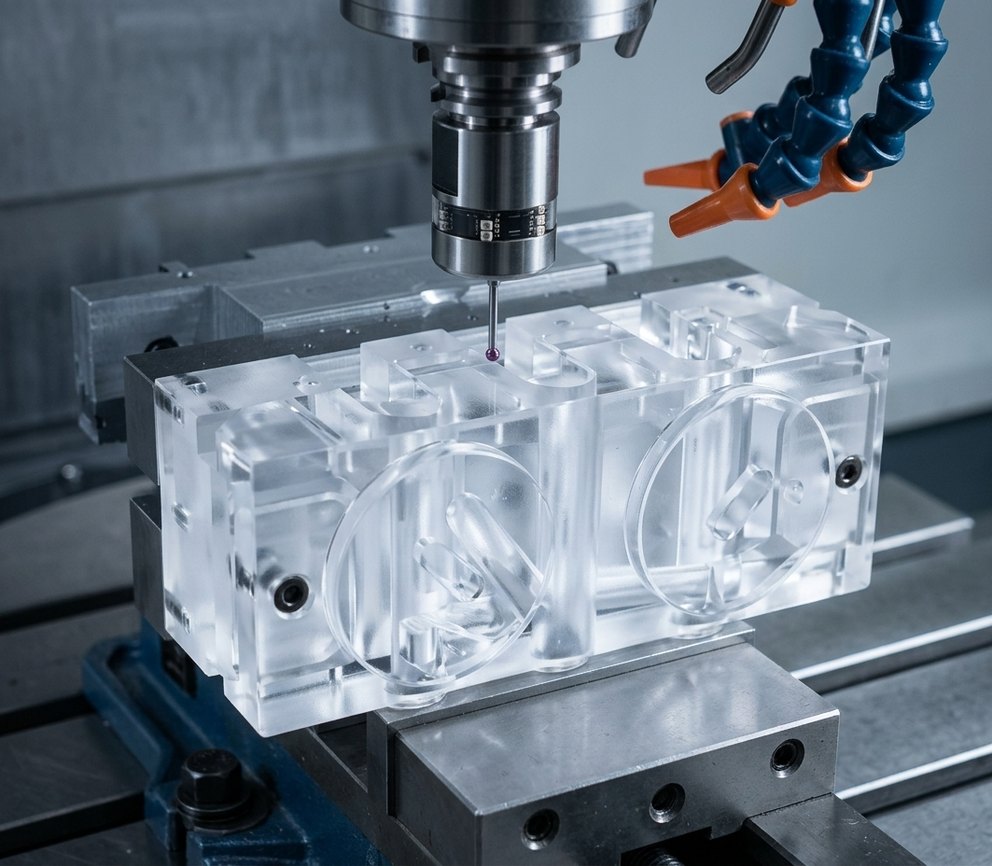
In clear acrylic machining, PMMA machining tolerances are measured after 24 hours at room temperature, with haze and edge clarity checked too.
-
1
CNC Milling
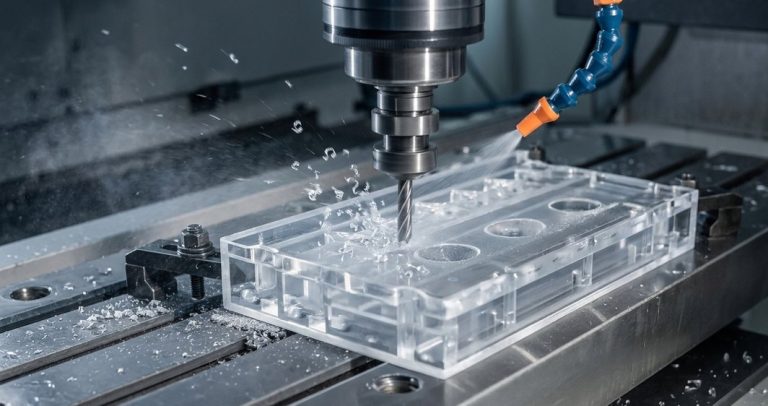
3-, 4- and 5-axis CNC milling for pockets, windows, chamfered edges, engraved text and freeform lens surfaces, using sharp polished-flute tooling.
-
2
CNC Turning
Round lenses, sight glasses, light pipes and threaded caps turned with air-blast cooling to avoid heat that clouds or crazes the surface.
-
3
Drilling and Tapping
Peck cycles and reduced feed at breakthrough stop chip-out; threaded inserts go into holes that see repeated assembly instead of interference fits.
-
4
Polishing and Bonding
Flame, vapor and diamond polishing, laser marking and solvent bonding. For sheet enclosures, see custom acrylic fabrication.
Design & Machining Tips for Acrylic
Rules our engineers apply to keep custom acrylic parts free of cracks, crazing and fit problems.
-
1
Stress Relief by Annealing
We anneal cast blanks at about 80 °C with a slow cool before finish passes, and again before solvent bonding or exposure to alcohols, which otherwise craze edges.
-
2
Thermal Expansion
A 70 mm acrylic lens grows about 0.13 mm more than its aluminum barrel over a 40 °C swing. Leave radial clearance or use a compliant retaining ring.
-
3
Sharp Corners
Internal corners start cracks: specify a radius of at least 0.5 mm (1 mm preferred). External edges get a 0.3 mm chamfer unless they are flame polished.
-
4
Thin Walls
Keep walls at 1.5 mm or more, 2 mm where the part will be polished or bonded. We can hold 0.8 mm on short spans with a backing fixture.
-
5
Cracking and Crazing
Air blast or a non-aromatic coolant, low clamping pressure on soft jaws or vacuum fixtures, and no press-fit pins. Specify tapped inserts, not interference fits.
-
6
Holes and Optical Faces
Zero-rake plastic drills, 0.05 mm oversize for through-fasteners, countersunk heads. On optical faces, call out flatness and scratch-dig, not a linear dimension.
When to Choose Acrylic vs Polycarbonate or PET
How acrylic compares with polycarbonate and PET. If no transparent window is needed, aluminum machining holds tighter tolerances.
| Criteria | This MaterialAcrylic | Polycarbonate | PET |
|---|---|---|---|
| Choose it for | Lenses, light guides | Guards, visors | Chemical exposure |
| Light transmission | 92% | 88% | – |
| Impact strength | Lower | 10–20× acrylic | – |
| Polishability | Best | Lower | Lower |
| Scratch / UV | Resistant, UV stable | Less resistant | – |
| Food contact | – | – | Approvals |
Where Custom Acrylic Parts Are Used
From microfluidic manifolds to cabin lighting lenses, machined PMMA serves wherever a part must be clear, light and precise.
-
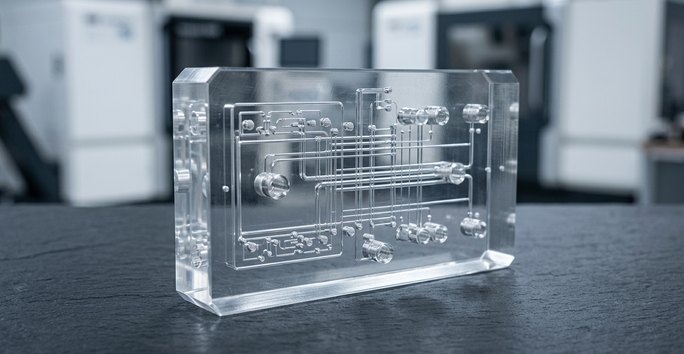 Medical and LaboratoryMicrofluidic manifolds, cuvette holders, sight windows and diagnostic device covers, machined under ISO 13485.
-
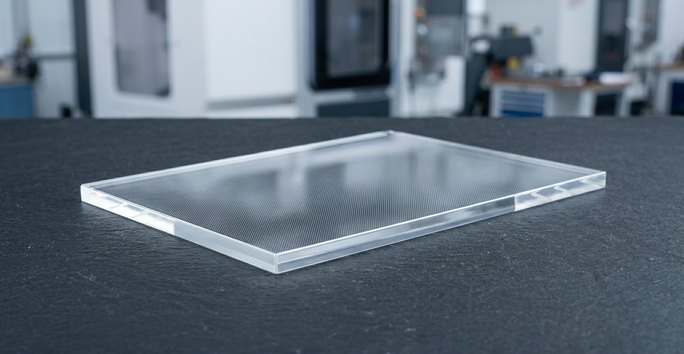 Electronics and DisplayLight guides, LED diffusers, touch-screen covers and instrument bezels polished for clean, even light output.
-
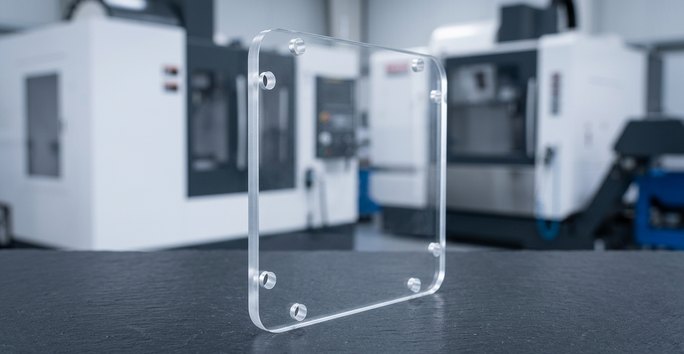 AutomationMachine guards, sensor covers and inspection fixtures that let operators see the process while keeping it enclosed.
-
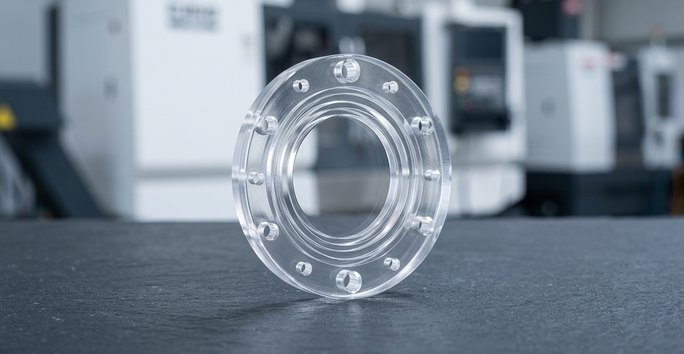 SemiconductorWafer viewing windows and inspection fixtures machined to hold ±0.01 mm on small, well-supported features.
-
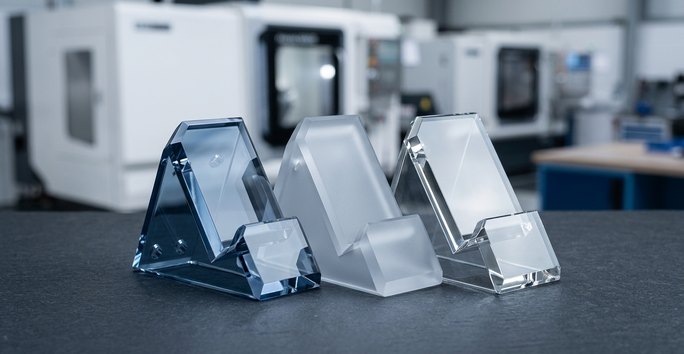 Consumer ProductsDisplay stands, lighting components and optical accessories in clear, colored, frosted or mirrored sheet.
-
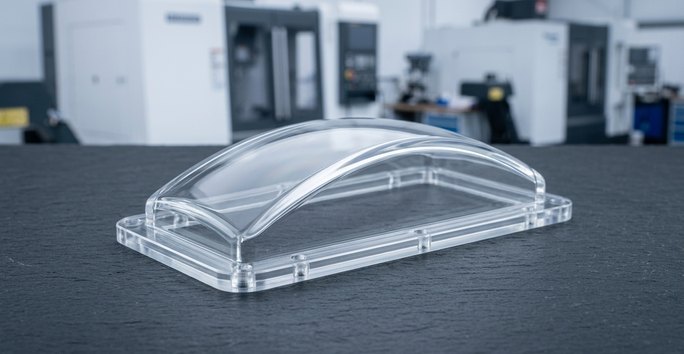 Aerospace and DefenseCabin lighting lenses, gauge covers and training-equipment windows, inspected from IQC through OQC before shipment.
Finishing Options for Polished Acrylic Parts
CNC machining plus finish: restore optical clarity, frost a diffuser face or mark part numbers on your acrylic parts.
Need another finish on PMMA? See all finishing options
-
 Vapor polishingMost PopularRestores optical clarity on complex geometries and internal channels that a buffing wheel cannot reach.Get a Quote
-
 Flame polishingMost PopularFast on straight edges; not for close-tolerance faces because it rounds edges slightly.Get a Quote
-
 Diamond and buff polishingMost PopularReaches Ra 0.05 µm or better on flat faces and lens surfaces after CNC machining.Get a Quote
-
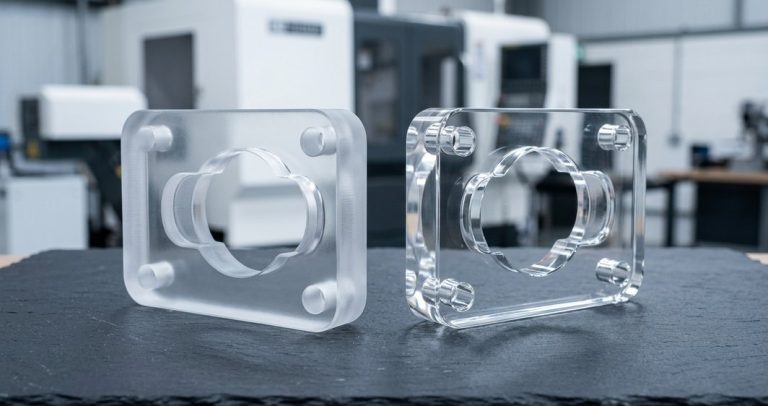 Bead blastingMost PopularCreates frosted diffuser surfaces and glare-free display faces on machined acrylic.Get a Quote
-
 Painting and back-paintingMost PopularOpaque colors on display parts, with masking that keeps the transparent windows clear.Get a Quote
-
 Laser markingMost PopularPermanent part numbers and scales marked on machined acrylic parts and instrument windows.Get a Quote
Acrylic Machining FAQ
Common questions from engineers specifying machined PMMA parts.
Other Materials
-
 DelrinAcetal homopolymer (Delrin 150) and copolymer for gears, bushings, valve bodies and food-contact parts: clean chips, low moisture, ±0.01 mm typical.Learn More
-
 NylonTough, quiet, self-lubricating PA6, PA66, 30% glass-filled and MoS2 nylon for gears, bushings, wear pads, rollers and insulators.Learn More
-
 PEIUnfilled Ultem 1000 and 30% glass-filled Ultem 2300 PEI for test sockets, sterilization trays and aircraft brackets: 170 °C continuous, UL 94 V-0.Learn More
-
 PolyethyleneUHMW-PE and HDPE: the lowest-friction, most abrasion-resistant commodity plastic, FDA compliant in natural grades, for wear strips and chain guides.Learn More

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








