









Invar 36 Machining Services
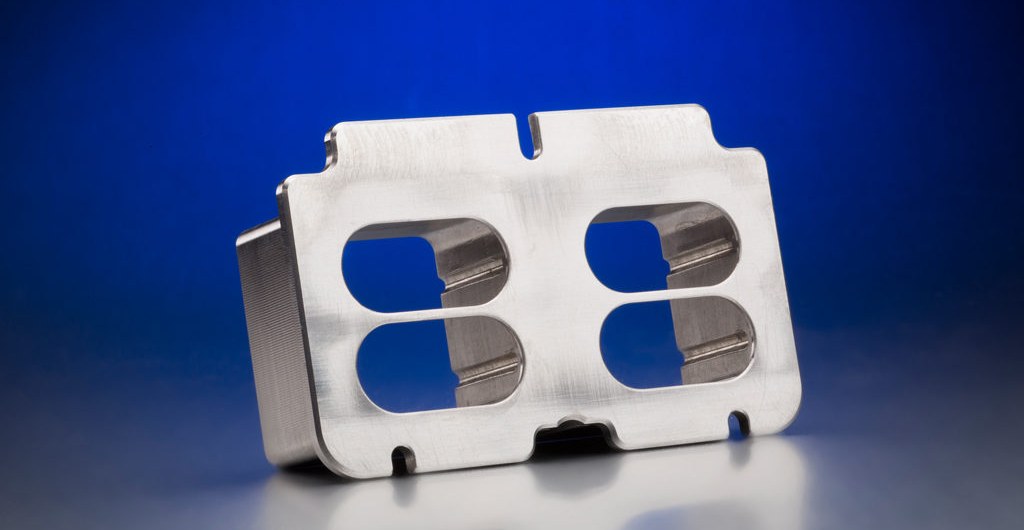
Also known as FeNi36 · UNS K93600 · EN 1.3912Invar 36 machining is ordered when a part must not move as temperature changes: FeNi36 expands about 1.2 µm/m·°C at 20–100 °C. DEK mills, turns, EDMs and grinds it to ±0.005 mm on request, with heat-treat cycles that keep dimensions stable.
-
1.2–1.5CTE µm/m·°C
-
450–550 MPaTensile Strength
-
240–280 MPaYield Strength
-
8.05 g/cm³Density
Invar 36 Machining Capabilities and Tolerances
Tolerances, finishes and part sizes DEK holds on Invar 36, inspected on CMM at 20 ± 0.5 °C after a 4-hour soak.
-

Milled & turned
±0.025 mm±0.005 mm on request
-

Swiss-turned features
±0.003 mm1 mm to 250 mm dia.
-

5-axis mold surfaces
±0.01 mmprofile
-

Bores
H6/H7standard fits
-

Ground flatness
0.003 mmover 300 mm
-

Surface finish
Ra 0.8–1.6 µmas-machined
-

Ground finish
Ra 0.2–0.4 µmprecision grinding
-

Prototype lead time
3–5 daysplus heat-treat cycles
Invar 36 Properties and Equivalent Designations
Annealed Invar 36 data: below its Curie temperature (about 230 °C) the CTE is near zero, then rises steeply above 200 °C.
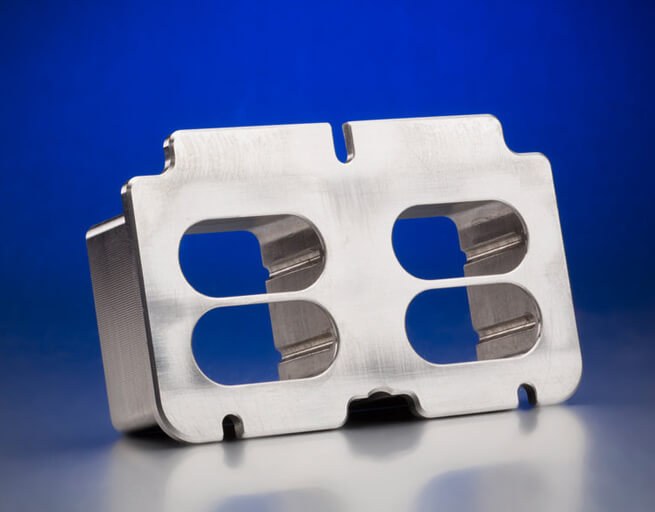

- Tensile strength 450–550 MPa
- Yield strength 240–280 MPa
- Hardness, annealed 130–170 HB
- Hardness, cold worked up to 250 HB
- Machinability ~35–40% (1212 = 100%)

- CTE, 20–100 °C 1.2–1.5 µm/m·°C
- CTE limit, ASTM F1684 ≤1.6
- CTE, 20–200 °C 2.0–2.5
- Curie temperature about 230 °C
- Density 8.05 g/cm³
- Thermal conductivity 10.5 W/m·K

- Ni 35–37%
- Mn ≤0.6%
- Si ≤0.35%
- C ≤0.10% (0.05% typical)
- Fe balance

- UNS K93600
- EN 1.3912 (Ni36)
- DIN / JIS Ni36 / Ni 36
- Round bar 6–250 mm
- Plate 6–100 mm
Why Fe-Ni36 Machining Is Gummy
How Invar 36 behaves on the shop floor: stringy chips, work hardening, trapped heat and slow stress relaxation.
Fe-Ni36 machining behaves like a soft austenitic stainless: the chip is long and stringy and welds to the edge if speed or feed drifts low. We run sharp, positive-rake, polished carbide with feeds high enough that the tool cuts rather than plows.
With 10.5 W/m·K, heat stays at the cut, so flood coolant is standard. Machining stresses relax over weeks unless removed by the stress-relief sequence run through heat treatment.
- Every finishing pass takes at least 0.1 mm to stay under the work-hardened skin.
- Tools are changed on schedule; thread milling rather than tapping above M6.
- Wire EDM cuts flexures and thin slots that would deflect under a cutter.
- Critical features finish on precision grinding.
-
Cutting Speed
40–80 m/minPositive-rake polished carbide
-
Machinability
~35–40%1212 steel = 100%
-
Work Hardening
150 to 250+ HBThin skin, rubbing tool
-
Min. Finish Pass
0.1 mmStays below hardened skin
-
Stress Drift
10–30 µm300 mm part, if not relieved
Optical, Metrology and Tooling Applications
Invar 36 parts machined where a few micrometers of thermal drift would break the function.
-
 Optical MountsMirror mounts, laser resonator frames, lens cells and interferometer bases; 5-axis machining cuts contoured mirror mounts.
-
 Metrology FixturesCMM artifacts, gauge fixtures and length standards, built on a CTE of about 1.2 µm/m·°C at 20–100 °C.
-
 Semiconductor PartsWafer stage components and reticle holders for semiconductor equipment where thermal stability sets positioning accuracy.
-
 Composite Layup MoldsLayup molds, mandrels and satellite optical benches; Invar's CTE matches cured carbon-epoxy after a 180 °C autoclave cure.
Invar 36 vs Kovar and Other Low-CTE Materials
Choose Invar 36 when the part itself must hold dimension; choose Kovar when it must match glass or alumina in a seal.
| Criteria | This GradeInvar 36 | Kovar | Super Invar |
|---|---|---|---|
| Nickel content | 36% Ni | 29% Ni | 32% Ni |
| Cobalt content | – | 17% Co | 5% Co |
| CTE (µm/m·°C) | 1.2–1.5 | about 5–6 | near 0.3 |
| Chosen for | Dimensional hold | Glass-to-metal seals | Lowest CTE |
| Machinability | ~35–40% | Slightly easier | – |
| Stress relief | Needed | Needed | – |
CNC Machining + Finish for Invar 36
Invar has no chromium and rusts like plain steel, so DEK ships parts oiled or with a finish applied to the parts we machine.
-
Electroless nickel plated AvailableThe usual finish on machined Invar 36 parts, applied after machining to protect an alloy that rusts like plain steel.
-
Gold plated AvailableGold plating is offered on Invar 36 parts we machine, typically specified with the plating spec sent alongside the drawing.
-
Black oxided AvailableBlack oxide is applied to machined Invar 36 parts as one of the usual protective finishes for this chromium-free alloy.
-
Rust-preventive oil AvailableEvery Invar 36 part ships with rust-preventive oil, since the alloy has no chromium and corrodes like plain steel.
Request an Invar 36 Machining Quote
Send a STEP, IGES or PDF drawing with stability requirement, tolerances and plating spec. An engineer lays out the stress-relief sequence and prices it within 6 hours.
Why DEK for Low Expansion Alloy Machining
20+ years of low expansion alloy machining in Invar, Kovar and Super Invar, with heat cycles, grinding and CMM inspection controlled in one workflow.
DEK is ISO 9001:2015, ISO 13485 and AS9100D certified by TÜV. Every lot gets a spectrometer check, and parts are inspected on CMM at controlled temperature. Invar 36 is the base grade on our Invar machining page.
Stress-relief cycles are built into the process and the quote. Engineer-reviewed quotes return within 6 hours, with no MOQ and prototypes in 3–5 days plus heat-treat cycles, through our CNC machining services workflow.
Choose Invar 36 when thermal drift of more than a few micrometers over a 10–20 °C swing would break the function: optical alignment, metrology references, and composite tooling cured at 180 °C, including frames up to about 1000 mm on CNC milling.
Do not choose it for service above 200 °C, where the CTE rises sharply toward the Curie point, for yield strength above 280 MPa, for corrosive environments without plating, or for large low-precision structures where its price is not justified.
-
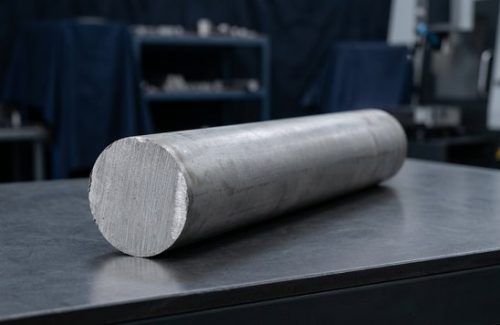 Raw Stock
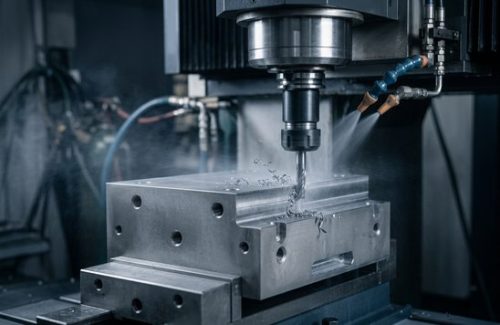 CNC Machined
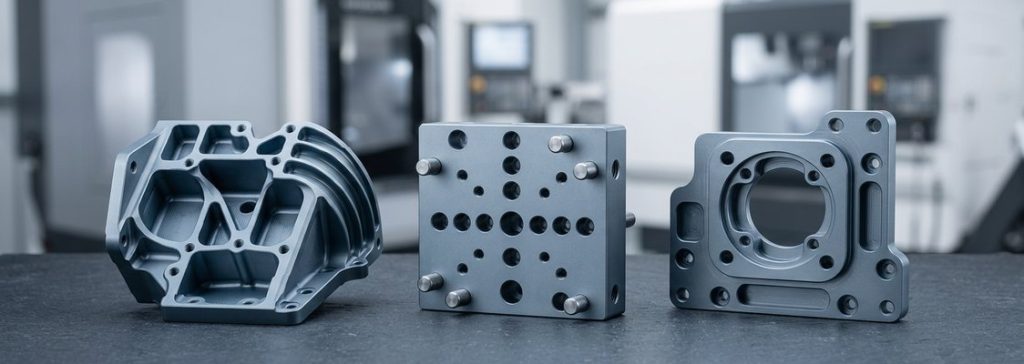 Finished Parts
-
 Raw Stock
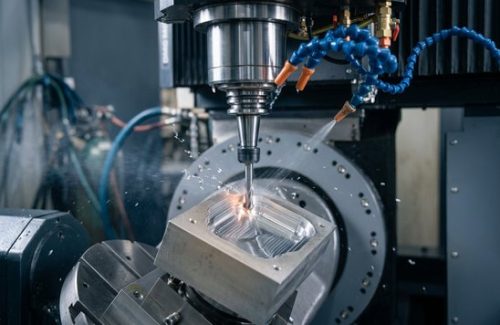 CNC Machined
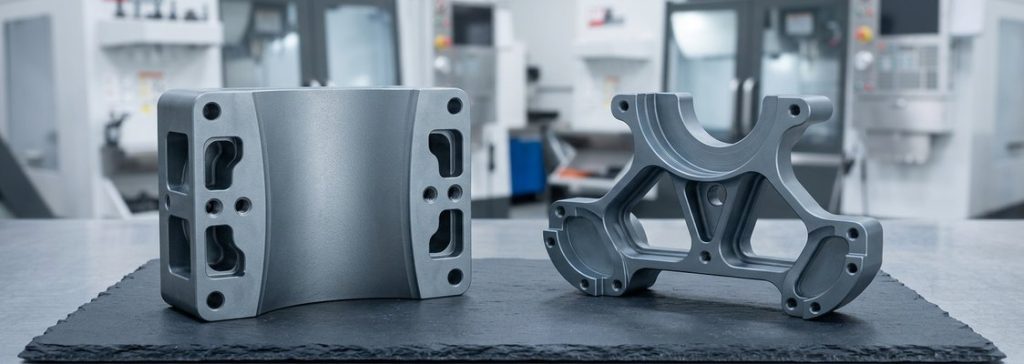 Finished Parts
Invar 36 Machining FAQ
Common questions from engineers specifying Invar 36 parts for stability.
Other Materials
-
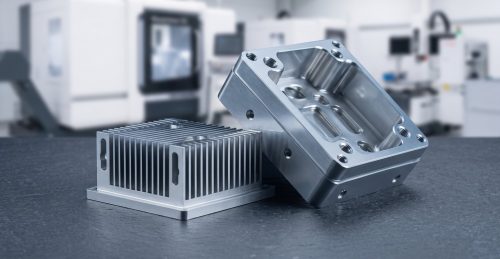 Aluminum 6063Aluminum 6063 is mainly composed of aluminum, magnesium, and silicon. Its excellent machinability makes it good for cutting, drilling, and shaping in CNC processes.Learn More
-
 Magnesium AZ61BMagnesium AZ61B is a wrought magnesium alloy in the AZ61 series. It has a low density, good strength-to-weight ratio, and excellent machinability.Learn More
-
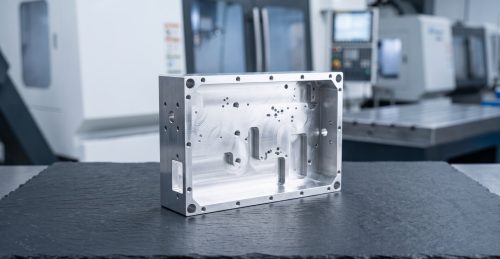 Aluminum 6082Aluminum 6082 is known for being highly resistant to corrosion and possessing exceptional strength, the highest among the 6000 series alloys.Learn More

Ready to Scale Your Project?
Get started with a stable process and controlled quality. Let's discuss your project.








